Degreaser manufacturing services move through a structured production sequence: formulation review, pilot batching, raw material procurement, high-shear blending, and packaging configuration, to deliver consistent, high-performance cleaning agents at scale. Building that capability in-house means absorbing the cost of mixing vessels, explosion-proof electrical systems, and environmental compliance infrastructure before a single batch ships. Working with an established contract manufacturer removes that burden. Industrial Technology Corporation handles the full production arc for industrial and commercial degreasers, from feasibility review through finished, labeled, and palletized goods ready for distribution.
How Do Degreaser Manufacturing Services Work?
The process begins well before a drop of raw material enters a vessel. Scale changes chemistry, and a contract manufacturer’s first obligation is to confirm that a proposed formulation is chemically sound and safe to produce at volume.
During formulation review, the manufacturer scrutinizes an existing formula, or co-develops one from scratch, and runs a compatibility analysis to confirm that every ingredient is miscible, stable under production conditions, and compatible with the intended packaging material. This step catches problems that only surface at scale, such as phase separation in concentrated blends, unexpected exothermic reactions during high-shear mixing, or surfactant instability at elevated temperatures. Once a formula clears feasibility, a pilot batch is produced at laboratory scale to verify cleaning efficacy, viscosity, and physical stability before committing to a full production run. The same technical groundwork that supports surfactant blending, particularly emulsification behavior and surfactant selection, carries over directly into degreaser formulation work.
Raw material sourcing follows next. Contract manufacturers carry bulk purchasing leverage that individual brands rarely match, which translates into lower per-unit costs for surfactants, alkaline builders, chelating agents, and solvents. At full-scale production, operators sequence ingredient additions into stainless steel or HDPE mixing vessels based on solubility and reactivity. Water-soluble builders go in first, surfactants are introduced under controlled agitation to prevent excessive foaming, and heat-sensitive components are added only after the batch temperature stabilizes. Standard heavy-duty alkaline degreasers typically contain 1% to 40% alkaline builders and 0.5% to 15% surfactants, and hitting those concentration targets consistently requires precise metering, calibrated agitation speed, and real-time temperature monitoring throughout the blend cycle.
What Types of Degreaser Products Can Be Blended?
Manufacturers capable of handling industrial-grade formulations work across a broad range of degreaser categories, spanning both liquid and powder formats, each with distinct chemistry and equipment requirements. Format dictates the process from start to finish.
Water-based degreasers: Formulated with surfactants such as alcohol ethoxylates and non-ionic surfactant packages, alkaline builders like sodium metasilicate, and chelating agents like EDTA to emulsify and lift hydrocarbon soils. Low VOC emissions make this the prevalent format in facilities with air quality compliance requirements.
Solvent-based degreasers: Rely on organic solvents to dissolve hydrocarbon soils, waxes, and adhesive residues directly. Production requires explosion-proof blending equipment and rigorous environmental controls, and these formulas are not interchangeable with aqueous-line infrastructure.
Concentrated degreaser blends: High-active formulations engineered to minimize freight and storage costs, diluted at the point of use. Maintaining phase stability in a concentrated state, meaning no precipitation or separation during storage, requires careful management of the builder-to-surfactant ratio.
Powder degreasers: Dry-blended formulations used in heavy-duty concrete floor scrubbers and industrial soak tanks. Particle size uniformity and moisture control during blending are critical to product performance and shelf stability. Learn more about the process behind dry-blend powder production.
The financial case for outsourcing is clear, but the operational case is often more compelling for companies that have tried running blending in-house.
Capital expenditure elimination: Mixing vessels, explosion-proof electrical systems, secondary containment, and environmental monitoring infrastructure represent a seven-figure investment before a single gallon is produced.
Cost efficiency: Brands transitioning from in-house blending to outsourced toll blending have documented up to a 27% reduction in product costs, driven by bulk raw-material purchasing power and optimized production scheduling.
Operational focus: Engineering and operations staff redirect their time toward distribution, customer service, and product development rather than batch scheduling and equipment maintenance.
Regulatory compliance transfer: The manufacturer assumes responsibility for managing safety data sheets, GHS labeling accuracy, chemical storage compliance, and waste disposal, a burden that grows in proportion to product line complexity.
Degreaser Manufacturing Services for Industrial Cleaning Applications
Heavy-duty industrial degreasers operate in conditions that place significant chemical stress on both the cleaning agent and the substrate. Removing carbon deposits, stamped-in drawing lubricants, crude oil residues, and synthetic metalworking fluids from metal, plastic, and composite parts demands formulations with enough alkalinity and surfactant activity to lift tenacious soils, all without etching aluminum alloys, staining anodized surfaces, or degrading polymer seals in the process.
Surfactant selection drives most of the performance differentiation in industrial degreaser formulation. A manufacturer working on a metalworking application will typically blend corrosion inhibitors, such as benzotriazole derivatives for copper alloys and sodium nitrite or amine-based inhibitors for ferrous metals, to prevent flash rusting on freshly cleaned steel parts, which can oxidize within minutes of aqueous cleaning if the rinse water isn’t neutralized or the inhibitor package isn’t present. Getting that chemistry right at the pilot batch stage is a known science; maintaining it across large production runs is where process discipline and quality control testing become operationally non-negotiable.
Degreaser production sits squarely within heavy-duty industrial and commercial chemical blending, a distinction that matters when evaluating a manufacturing partner. The equipment, regulatory framework, and formulation expertise required for industrial degreaser production share almost nothing with consumer-facing categories like private label skincare, cosmetics, or dietary supplements, which operate under an entirely different regulatory regime built around FDA cosmetic compliance and dermatological safety testing rather than industrial hazard communication standards.
Solvent-Based, Water-Based, and Concentrated Degreaser Blends
Water-based systems clean through three simultaneous mechanisms. Surfactant emulsification breaks the interfacial tension between the soil and the substrate, alkaline saponification converts fatty acid soils into water-soluble soaps, and chelation sequesters hardness ions that would otherwise precipitate and redeposit as scale. The shift away from chlorinated solvents, trichloroethylene in particular, which the Environmental Protection Agency has moved to restrict under the Toxic Substances Control Act, has accelerated the adoption of aqueous systems across automotive, aerospace, and general metalworking sectors. Modern water-based formulations, when properly specified, match or exceed the cleaning performance of legacy chlorinated products on most common industrial soils.
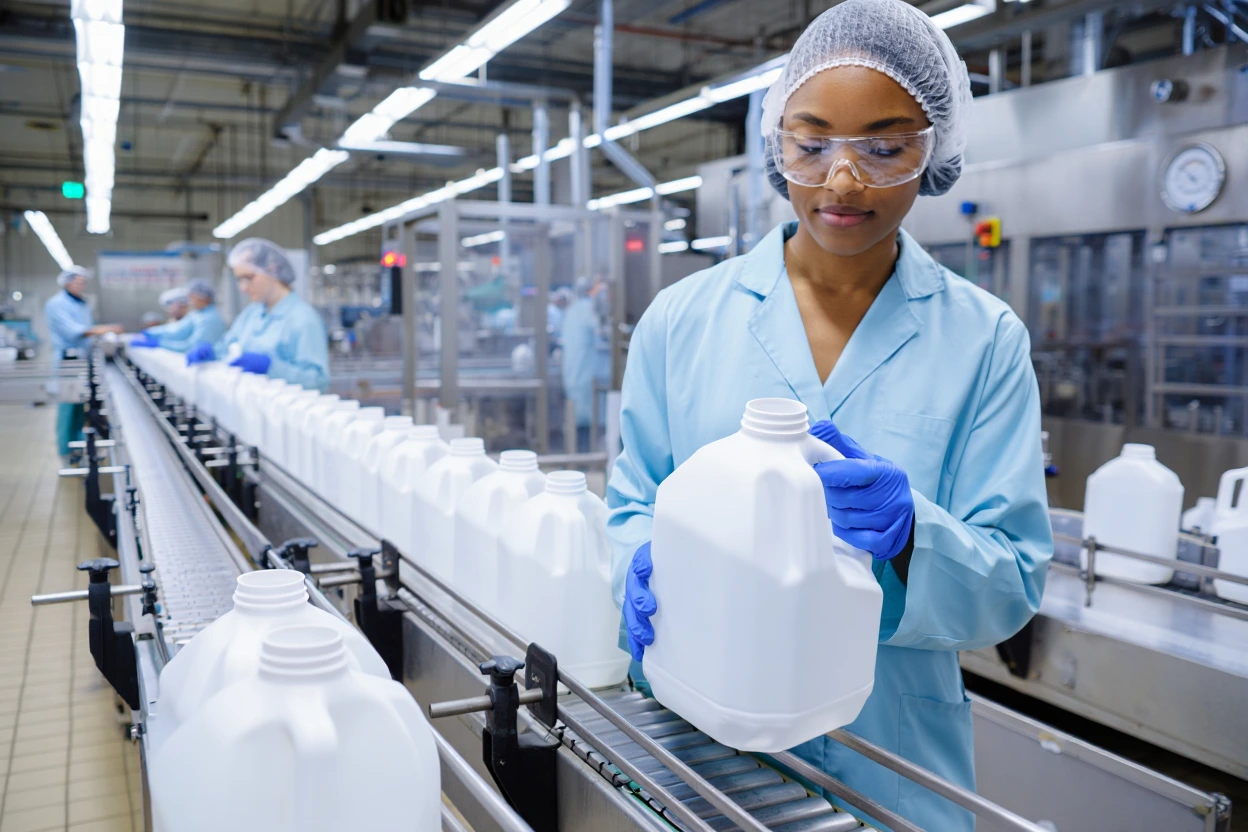
Packaging format selection reflects how a product will actually be used in the field. Spray bottles account for a substantial share of the degreaser packaging market, reflecting the volume of ready-to-use commercial and janitorial applications, while drums remain the standard for high-volume industrial accounts where concentrated product is dispensed through dilution stations or applied via pressure washing equipment. That split has direct implications for how filling lines are configured: trigger-spray fill heads, capping torque settings, and label placement tolerances differ substantially between a 32-ounce bottle and a 55-gallon drum. A well-equipped manufacturer runs both without treating either as an afterthought. Explore private label chemical packaging for a closer look at container and labeling options.
Quality Checks for Strength, Consistency, and Packaging Accuracy
Every production batch moves through a defined QA/QC sequence before it ships. No batch clears on visual inspection alone.
pH Testing (ASTM D1172): Verifies that the alkalinity or acidity of the finished blend matches the target specification. A heavy-duty alkaline degreaser running outside its pH window will underperform on saponifiable soils or risk substrate damage.
Specific Gravity (ASTM D891): Confirms liquid density, which serves as a proxy for active ingredient concentration. A specific gravity variance from spec is often the first indicator of an under-diluted or over-diluted batch.
Total Alkalinity (ASTM D460): Measures the chemical buffering capacity of alkaline degreasers, a critical parameter for products used in recirculating soak tanks where bath depletion must be tracked and corrected.
Flash Point Verification (ASTM D56 / D93): Required for any solvent-containing blend. Flash point data determines DOT hazmat classification, shipping requirements, and storage protocols.
Soil-Removal Performance: Steel coupon testing verifies cleaning efficacy against established residual soil benchmarks, which serve as a meaningful reference point for products positioned in institutional or government procurement channels.
Packaging and Fill Accuracy: Automated filling lines use gravimetric weight-checking to confirm precise fill volumes across every container format, from trigger spray bottles to 275-gallon IBC totes.
Choosing the Right Degreaser Manufacturing Partner
Technical capability is the threshold criterion. A manufacturer that cannot demonstrate liquid and powder format capability, formulation modification services, and packaging configurations spanning from 5-gallon pails to bulk tankers is not equipped to grow with a degreaser line as it scales across distribution channels.
Beyond equipment, geography carries more weight in bulk chemical logistics than most procurement teams initially account for. A centrally located blending facility with direct freight access to major manufacturing hubs can meaningfully reduce freight costs and lead times for high-volume accounts shipping 55-gallon drums or 275-gallon totes compared to sourcing from either coast. Proximity to the end-use environments a formulation is designed to serve also informs formulation decisions in ways a distant manufacturer cannot easily replicate.
Regulatory Compliance and Safety Standards in Degreaser Manufacturing Services
Chemical manufacturing at the industrial scale operates under layered regulatory oversight, and a manufacturer that treats compliance as a secondary concern creates liability risk for every brand whose product runs through its facility.
OSHA’s Hazard Communication Standard (HazCom 2012, aligned with the Globally Harmonized System) requires that every hazardous chemical produced or handled in a U.S. facility be accompanied by a compliant Safety Data Sheet and GHS-formatted label. For a manufacturer producing toll blended degreasers, this means generating accurate SDS documentation for each formulation, including correct hazard classifications, exposure limits, first-aid measures, and disposal guidance, and confirming that label artwork submitted by a client meets all GHS pictogram, signal word, and precautionary statement requirements before a product ships. Errors in SDS or label content are not administrative inconveniences; they are compliance violations that carry per-incident penalties. Formulations that carry hazmat classifications also need packaging and shipping documentation handled correctly from the start, which is where hazmat chemical packaging support becomes essential.
At the facility level, chemical storage, secondary containment, stormwater management, and wastewater discharge fall under both federal EPA regulations and state environmental standards. Facilities operating near industrial waterways face active oversight of runoff prevention and spill containment protocols, not theoretical review. Brands whose formulations are manufactured at a facility that has already built compliance infrastructure into daily operations avoid treating it as an expensive add-on later.
Frequently Asked Questions
What is the difference between toll blending and contract manufacturing?
Toll blending is a narrower service: the client provides the formulation, and sometimes the raw materials, while the manufacturer executes the blending and packaging. Contract manufacturing covers a broader scope, including custom formulation development, raw material sourcing, QA/QC protocol development, packaging configurations, and outbound logistics. Many brands start with toll blending and expand into full contract manufacturing as their degreaser line grows. See degreaser contract blending for a full breakdown of service structure.
What packaging formats are available for toll blended degreasers?
Standard configurations include 32-ounce trigger spray bottles for janitorial and commercial use, 1-gallon jugs for mid-volume commercial accounts, 5-gallon pails, 55-gallon drums, and 275-gallon IBC totes for high-volume industrial distribution. Container material selection, such as HDPE, polypropylene, or steel, depends on the formulation’s pH, solvent content, and shelf-life requirements.
Can water-based degreasers perform as well as solvent-based ones?
Yes, with the right surfactant architecture. Modern aqueous formulations use non-ionic surfactant blends, specifically alcohol ethoxylates, alkyl polyglucosides, and amine oxides, combined with alkaline builders to emulsify and lift heavy mineral oils, synthetic lubricants, and stamping compounds from metal substrates. The performance gap between aqueous and solvent-based systems has narrowed considerably over the past decade, and for most common industrial soils, a well-formulated water-based degreaser eliminates the flammability risk, VOC liability, and waste disposal complexity of solvent-based alternatives without sacrificing cleaning efficacy.
What is the typical minimum order quantity for degreaser manufacturing services?
Minimum order quantities vary based on formulation complexity, raw material procurement lead times, and packaging line configuration. For liquid blending, minimums typically start at 500 to 1,000 gallons, the threshold at which production and packaging line efficiency justifies the setup cost. Powder blending minimums are governed by dry-blending equipment cycle times and packaging line requirements. A technical team can provide specific guidance once a formulation and packaging configuration are defined.
How long does it take to go from formulation review to first production run?
Timelines depend on formulation complexity and whether raw materials need to be sourced or are already on hand. A straightforward reformulation of an existing degreaser with common ingredients can often move from feasibility review to pilot batch within a few weeks, while a fully custom formulation with specialty surfactants or corrosion inhibitors may take longer to validate. Building in time for pilot batch testing and QA/QC review before committing to a full production run helps avoid costly rework later.
Improving a chemical supply chain requires more than finding a manufacturer with available tank capacity. It requires a partner who understands formulation chemistry well enough to catch compatibility issues before they reach production, who maintains QA/QC protocols rigorous enough to defend batch consistency across every order, and who operates under the regulatory framework that governs industrial chemical manufacturing rather than consumer cosmetics or food supplements. The next step is a formulation feasibility review, where a technical team evaluates a formula, target volumes, and packaging requirements and returns a concrete cost-benefit analysis.
Ready to scale degreaser production? Contact Industrial Technology Corporation today to discuss degreaser manufacturing and packaging requirements with a technical team based in Davenport, Iowa.
When it comes to creating high-quality car care products, one key component is achieving the right blend of soaps and waxes. Whether used for hand washes, automated tunnel washes, or detailing services, car wash soaps and waxes require careful formulation to ensure they deliver both cleaning power and protection. This is especially true in today’s market, where customers seek not only cleanliness but a showroom-quality finish.
Understanding the Chemistry of Car Wash Soaps
Car wash soaps are more than just simple detergents. They’re crafted blends of surfactants, emulsifiers, and other agents designed to lift dirt, oil, and grime from a car’s surface without harming the paint or finish. The composition of these soaps affects their performance, including their foaming ability, rinsability, and compatibility with waxes and sealants.
Surfactants and Their Role
Surfactants are one of the primary components in car wash soaps. These molecules are specially designed to lower the surface tension between water and contaminants, allowing dirt and oils to be lifted off surfaces more effectively. Different types of surfactants can be used to create various levels of cleaning power and foam. For example:
Anionic surfactants provide a rich lather and are excellent at breaking down oils and dirt but may be harsher on certain finishes.
Non-ionic surfactants are gentler and work well in combination with other chemicals to stabilize and soften the cleaning process.
Amphoteric surfactants are versatile and can adapt to varying pH levels, making them ideal for formulations that require compatibility with waxes and conditioners.
Balancing pH Levels
A car wash soap’s pH level is critical for ensuring it cleans effectively without damaging the vehicle’s surface. High-alkaline soaps are effective at removing tough grime but may be too harsh for some finishes. Neutral or slightly acidic soaps are gentler and better suited for routine washes. Finding the right pH balance is crucial for manufacturers to offer a versatile soap that is safe for all paint types and finishes.
The Art and Science of Blending Waxes
Waxes add a protective, glossy layer to the car’s surface, enhancing shine and helping repel dirt, water, and UV rays. The blending of waxes for car care products requires a careful combination of natural and synthetic ingredients, emulsifiers, and stabilizers to ensure that the wax adheres well to the surface and lasts over time.
Types of Waxes in Car Care Products
The most common waxes used in car care products include:
Carnauba wax, derived from the leaves of the carnauba palm, is highly prized for its gloss and hydrophobic properties. It’s typically blended with other ingredients to enhance its spreadability and durability.
Synthetic polymers provide excellent durability and are often used in longer-lasting car waxes. They can be blended to produce a finish that rivals natural waxes while offering easier application and increased resilience.
Beeswax and other natural waxes add smoothness and improve texture in many formulations, although they’re generally used as secondary components to enhance the primary wax.
Liquid Blending for Wax Consistency and Performance
The blending process for waxes requires a high degree of precision to ensure consistency. Liquid blending equipment must be capable of evenly mixing ingredients at controlled temperatures to achieve a uniform product. Factors such as mixing speed, shear rate, and the order of ingredient addition can impact the performance of the final product. Careful blending ensures that the wax provides an even coat, bonds well with the paint, and enhances the car’s appearance.
Combining Soaps and Waxes for Optimal Results
Creating a car wash product that both cleans and protects requires the skillful blending of soaps and waxes. Car wash formulations that combine these two elements must achieve a delicate balance where the soap cleans effectively without stripping away the wax.
Challenges in Blending Soaps and Waxes Together
The blending of soaps and waxes presents a few challenges:
Compatibility: The pH of the soap and the wax’s stability must be compatible to avoid separation or degradation over time.
Cleaning vs. Protecting: While soaps are designed to lift and remove contaminants, they shouldn’t be so strong that they remove protective wax layers with each wash.
Rinseability: Products need to rinse cleanly without leaving residue, which can be challenging when waxes are involved, as wax residues can sometimes cause streaking.
Strategies for Effective Soap and Wax Blends
To overcome these challenges, formulators often employ techniques such as:
Layered Blends: Use surfactants that offer mild cleaning power along with polymers and waxes that deposit a thin layer of protection.
Time-Released Waxes: These advanced wax formulations slowly release over multiple washes, providing a gradual build-up of protection with regular use.
Emulsifiers: Emulsifiers are crucial in creating stable, homogeneous blends of soaps and waxes. They help combine oil- and water-based ingredients to produce a uniform, easily applied product.
The Role of Liquid Blending in Car Wash Formulation
Precision liquid blending is essential in the production of car wash soaps and waxes. With sophisticated equipment and highly controlled processes, manufacturers can ensure uniform consistency, texture, and performance in every batch.
Key Equipment and Techniques in Liquid Blending
The following equipment and techniques are vital for successful liquid blending:
High-shear mixers: Used to break down wax particles and incorporate them evenly into the solution. High-shear mixing is crucial when dealing with viscous ingredients or emulsions.
Inline homogenizers: These systems are used to ensure that all ingredients are mixed to a fine particle size, resulting in a stable emulsion.
Batch mixing tanks: Equipped with variable speed control, these allow for the blending of large quantities of product without compromising consistency.
Temperature control: Heat is often applied during blending to help dissolve or soften certain waxes and surfactants, making them easier to mix uniformly.
Quality Control in Blending
In car wash product formulation, consistency and performance are paramount. Each batch must undergo rigorous quality checks to ensure it meets the desired specifications. Common tests include:
Viscosity tests to ensure the product flows evenly during application.
Stability tests to determine whether the soap and wax separate over time.
Foam tests to measure the foaming capacity of soaps.
Gloss and water-repellency tests to assess the effectiveness of waxes.
Innovations in Car Wash Soap and Wax Blends
With advancements in chemical engineering and liquid blending technology, today’s car wash products are more effective and longer lasting than ever. Innovations in blending processes and ingredient formulations allow manufacturers to develop products with enhanced cleaning, protection, and shine.
Eco-Friendly Formulations
As consumers become more environmentally conscious, car wash product manufacturers are creating eco-friendly formulations that are biodegradable and free from harsh chemicals. Advanced liquid blending enables formulators to incorporate eco-friendly surfactants, natural waxes, and sustainable ingredients without compromising performance.
Nano-Ceramic Waxes
One of the latest trends in car wax is the use of nano-ceramic technology. These waxes incorporate nano-sized particles that bond at a molecular level to the car’s surface, creating a highly durable and glossy finish. Nano-ceramic waxes require advanced liquid blending techniques to ensure an even distribution of particles and proper adhesion.
Multi-Function Blends
Today’s car wash products are evolving to offer multiple benefits in a single application. From soap-wax combinations that clean, shine, and protect to UV-blocking ingredients that prevent paint fading, multi-function formulations provide added value to customers. Such complex formulations rely on precision liquid blending to combine diverse ingredients seamlessly.
Custom Blending Solutions for the Car Wash Industry
For businesses in the car wash industry, custom formulations provide an edge in a competitive market. Custom toll blending services allow brands to develop proprietary blends tailored to specific customer needs, environmental conditions, or equipment.
Private Label Opportunities
Many companies in the car wash industry leverage private labeling to offer products under their brand names. Toll blending companies can provide turnkey private label solutions, from formulation to packaging, enabling car wash businesses to develop their own line of soaps and waxes without the need for in-house blending facilities.
Advantages of Working with a Liquid Blending Specialist
Partnering with an experienced toll blending provider allows car wash product companies to scale production, maintain consistency, and adhere to quality standards. The benefits of working with a specialist in liquid blending include:
Access to state-of-the-art equipment: Professional blending facilities have access to advanced mixers, homogenizers, and heating systems, which are essential for producing high-quality car care products.
Expertise in chemical formulation: Skilled chemists and engineers understand how to balance soaps, waxes, and other additives to create a product that meets specific performance criteria.
Quality assurance protocols: Toll blending providers maintain strict quality control processes, ensuring every batch meets high standards for consistency, stability, and performance.
Partner with Industrial Technology Corporation for Your Liquid Blending Needs
The science and precision behind car wash soaps and waxes highlight the importance of quality liquid blending in producing top-tier products for the automotive industry. From selecting the right surfactants and waxes to implementing state-of-the-art blending techniques, creating high-performing car wash products requires expertise and dedication.
At Industrial Technology Corporation, we specialize in custom toll blending services, private label opportunities, and high-quality chemical formulations to meet your business’s unique needs. Whether you’re looking to develop a new car wash product, enhance an existing formula, or create a custom solution, our team is here to help.
Contact us today to discuss your specific requirements, request a quote, or learn more about how our blending services can elevate your product line. We look forward to working with you to develop innovative solutions that drive your business’s success.
In today’s fast-paced commercial environment, cleanliness is a top priority. Effective cleaning solutions are essential in any high-traffic area, whether it’s an industrial plant, hospital, food processing facility, or other commercial space. However, not all cleaning products are created equal. Off-the-shelf solutions may be convenient but lack the precision and effectiveness that custom formulations can provide for specific commercial needs. For businesses requiring unique cleaning standards or facing specialized challenges, concentrated, custom-formulated cleaners can offer a more effective and tailored solution.
Industrial Technology Corporation (ITC) is a trusted provider of custom chemical formulations, toll blending services, and private-label solutions for diverse industries. Our expertise in commercial cleaners allows us to create powerful, cost-effective products tailored to meet specific commercial cleaning challenges.
The Importance of Concentrated Cleaners in Commercial Settings
Concentrated cleaners are highly effective cleaning solutions that pack a punch in terms of both performance and cost-efficiency. Unlike diluted formulas, concentrated cleaners contain higher percentages of active ingredients, enabling users to dilute them to the desired strength for various cleaning tasks. This flexibility is especially beneficial in commercial settings where cleaning requirements vary significantly across different surfaces, contaminants, and equipment.
Benefits of Concentrated Commercial Cleaners
Cost Efficiency: Concentrated formulations provide more uses per volume than ready-to-use products, reducing the frequency of reordering and overall chemical expenditure.
Storage and Transportation: Concentrates reduce the volume and weight of cleaning products, lowering storage space requirements and transportation costs.
Reduced Environmental Impact: Concentrated cleaners minimize packaging waste and reduce the carbon footprint associated with shipping, making them a more environmentally friendly option.
Customizability: Concentrated solutions allow for precise adjustments based on the cleaning environment, which can enhance safety, efficacy, and cost-effectiveness.
ITC’s concentrated commercial cleaners can be custom-blended to meet unique cleaning needs in specific commercial applications, from removing heavy grease and grime to sanitizing medical-grade facilities. Each formulation is developed to maximize cleaning performance while considering factors like surface compatibility, user safety, and environmental compliance.
Custom Chemical Formulations for Specialized Commercial Needs
In commercial applications, cleaning requirements are rarely one-size-fits-all. Different industries face unique challenges that require custom chemical formulations. ITC specializes in developing high-quality commercial cleaners that address industry-specific challenges. Our experienced chemists and technicians work closely with clients to identify specific cleaning needs and develop custom formulations that enhance effectiveness and efficiency.
Key Industries Benefiting from Custom Formulated Commercial Cleaners
Healthcare: Medical facilities require disinfectants and cleaners that meet stringent health and safety standards. Custom formulations can provide antimicrobial properties and ensure compatibility with medical equipment.
Food and Beverage Processing: This industry faces strict regulatory requirements for cleanliness. Custom cleaners can be formulated to remove food residue, grease, and other organic materials, ensuring safety without compromising food quality.
Manufacturing and Industrial: Factories and plants often deal with heavy soils, oils, and other industrial contaminants. High-strength degreasers and solvents tailored to specific machinery or contaminants can make cleaning more efficient.
Hospitality and Facilities Management: Custom cleaners can provide solutions for managing the cleanliness of large areas, including floors, bathrooms, kitchens, and high-touch surfaces in hotels, office buildings, and retail spaces.
Each industry faces its own regulatory requirements, environmental concerns, and cleaning challenges, which can be more effectively addressed through custom formulations. ITC’s commitment to safety, regulatory compliance, and environmental responsibility ensures that our commercial cleaners align with each client’s unique requirements and industry standards.
The Science Behind Concentrated Custom Formulations
The creation of concentrated custom cleaners requires a deep understanding of chemistry, materials, and cleaning processes. ITC’s R&D team leverages years of expertise to design formulations that target specific contaminants and optimize cleaning performance.
Formulation Factors Considered by ITC
Active Ingredients Selection: The choice of surfactants, solvents, and additives is critical in designing a cleaner that effectively breaks down grease, grime, and other contaminants. ITC selects ingredients based on their cleaning efficacy, material compatibility, and safety profile.
pH Level: A cleaner’s pH level affects its suitability for different surfaces and contaminants. For instance, alkaline cleaners are effective on greasy soils, while acidic cleaners are better for mineral deposits.
Viscosity and Consistency: Viscosity can affect the product’s ease of application and ability to cling to surfaces. For example, thick gel formulations are often ideal for vertical surfaces, allowing for longer contact times.
Dwell Time: Custom formulations can be designed to optimize dwell time, which is the amount of time a cleaner needs to remain on a surface to be effective. Adjusting dwell time can help balance efficiency with cleaning power.
Environmental and Safety Regulations: ITC ensures all formulations comply with regulatory standards, including OSHA, EPA, and REACH guidelines. Biodegradable and environmentally safe ingredients are prioritized to support clients’ sustainability goals.
ITC’s Custom Formulation Process: From Concept to Delivery
At ITC, our custom formulation process is collaborative and client-focused. We work closely with each client to understand their specific needs and create formulations that solve unique cleaning challenges. Here’s an overview of how our process works:
Step 1: Consultation and Needs Assessment
We begin by consulting with clients to identify their cleaning challenges and requirements. This includes understanding the type of contaminants, surfaces, and cleaning methods used in their commercial environment.
Step 2: Research and Development
Once we understand the requirements, our chemists conduct research to determine the most effective ingredients and formulation strategies. This may involve testing different combinations of surfactants, solvents, and additives to achieve optimal performance.
Step 3: Testing and Quality Assurance
Every custom formulation undergoes rigorous testing to ensure it meets performance, safety, and environmental standards. This includes testing for cleaning efficacy, material compatibility, stability, and shelf life.
Step 4: Production and Packaging
Once the formulation is approved, we proceed with production. ITC offers toll blending services, allowing clients to outsource production while retaining control over the formula. Our production facilities are equipped to handle both small and large batches, and we offer flexible packaging options, including private labeling for clients seeking branded solutions.
Private Label Opportunities for Commercial Cleaners
In addition to custom formulations, ITC offers private label opportunities for businesses looking to expand their product line with high-quality commercial cleaners. Private labeling allows businesses to market premium cleaning products under their own brand name without the need for in-house formulation or production. Our team handles everything from formulation and blending to packaging, labeling, and shipping, providing a turnkey solution for clients.
Benefits of Private Labeling with ITC
Brand Differentiation: Private labeling allows companies to distinguish themselves in a competitive market by offering proprietary cleaning solutions.
Quality Assurance: All private label products benefit from ITC’s rigorous quality control and manufacturing standards, ensuring consistency and reliability.
Custom Packaging Options: We offer a range of packaging options tailored to different distribution needs, from bulk drums to small bottles, allowing for flexibility in product presentation.
Reduced Overhead: With ITC managing formulation and production, businesses can focus on their core operations while offering a high-quality product to customers.
Toll Blending Services for Streamlined Production
For companies that have developed their own chemical formulas but lack the resources for large-scale production, ITC’s toll blending services offer an efficient and cost-effective solution. Toll blending allows clients to maintain full control over their proprietary formulas while outsourcing the production process to a trusted partner.
Our state-of-the-art facilities are equipped to handle a wide range of chemical blending needs, from liquid and powder formulations to corrosive and high-viscosity products. We work under strict confidentiality agreements to protect client formulas, ensuring that all intellectual property remains securely in the client’s control.
Advantages of ITC’s Toll Blending Services
Scalability: Our facilities can handle both small and large batch sizes, making it easy to scale production based on demand.
Compliance and Safety: ITC ensures that all products are blended according to regulatory guidelines, with thorough testing to guarantee safety and quality.
Efficient Supply Chain Management: With ITC handling production and distribution logistics, clients can streamline their supply chain and reduce costs.
Technical Expertise: Our team of chemists and production specialists brings a wealth of experience, enabling us to handle complex formulations with precision and efficiency.
Why Choose ITC for Custom Formulated Commercial Cleaners?
ITC has a longstanding reputation for excellence in custom chemical formulations, toll blending, and private-label solutions. Our commitment to quality, safety, and client satisfaction has made us a trusted partner for businesses across a range of industries. We understand the importance of developing cleaning solutions that are not only effective but also aligned with regulatory requirements and sustainability goals.
Our dedicated team of chemists, R&D specialists, and production experts are committed to delivering solutions that meet the highest standards of quality and performance. Whether you need a specialized cleaner for a specific contaminant, a private-label solution to enhance your brand, or toll blending services to scale your production, ITC is here to help.
Contact ITC for Your Commercial Cleaner Needs
If your business requires high-quality, custom-formulated commercial cleaners, look no further than Industrial Technology Corporation. Whether you need custom toll blending services, private label opportunities, or quality chemical formulations tailored to your industry, we are here to meet your needs. Contact us today to inquire about our services, request a quote, or discuss your specific requirements. We look forward to partnering with you to develop innovative cleaning solutions that drive success for your business.
Commercial cleaning products are essential for maintaining cleanliness and hygiene in various industries, from hospitality and healthcare to manufacturing and retail. However, improper storage and handling of these products can pose serious health and safety risks to employees and customers. In this guide, we’ll discuss best practices for storing and using commercial cleaning products safely to minimize hazards and ensure a clean and safe working environment.
Understanding Commercial Cleaning Products
Types of Cleaning Products
Commercial cleaning products encompass a wide range of formulations, including disinfectants, detergents, degreasers, and sanitizers. These products contain various chemicals and active ingredients designed to effectively remove dirt, grease, stains, and germs from surfaces.
Common Chemicals
Some common chemicals found in commercial cleaning products include bleach (sodium hypochlorite), ammonia, hydrogen peroxide, quaternary ammonium compounds (quats), and alkalis (such as sodium hydroxide). Each chemical has specific properties and uses, but they can also present health and safety risks if mishandled or improperly stored.
Best Practices for Storing Commercial Cleaning Products Safely
Read Labels and Safety Data Sheets (SDS)
Before storing or using commercial cleaning products, carefully read the product labels and safety data sheets (SDS) provided by the manufacturer. Pay attention to important information such as chemical ingredients, hazard warnings, storage requirements, and first-aid measures.
Store in Proper Containers
Store commercial cleaning products in their original containers or appropriate chemical-resistant containers designed for that purpose. Avoid transferring products to unlabeled or incompatible containers, as this can lead to confusion, cross-contamination, and chemical reactions.
Segregate Hazardous Chemicals
Segregate hazardous chemicals, such as acids and alkalis, to prevent accidental mixing and chemical reactions. Store incompatible chemicals separately and ensure adequate ventilation in storage areas to minimize the risk of exposure to hazardous fumes or vapors.
Use Secure Storage Areas
Store commercial cleaning products in secure storage areas that are inaccessible to unauthorized personnel, such as locked cabinets, closets, or storage rooms. Keep products away from heat sources, direct sunlight, and sources of ignition to reduce the risk of fire or explosion.
Maintain Proper Ventilation
Ensure adequate ventilation in storage areas to prevent the buildup of fumes or vapors from commercial cleaning products. Install ventilation systems or use fans to circulate air and remove airborne contaminants, especially in confined or poorly ventilated spaces.
Keep Out of Reach of Children and Pets
Store commercial cleaning products out of reach of children and pets to prevent accidental ingestion or exposure. Use childproof locks or safety latches on cabinets or storage containers to restrict access and reduce the risk of accidental poisoning or injury.
Safe Handling and Use of Commercial Cleaning Products
Wear Personal Protective Equipment (PPE)
When handling or using commercial cleaning products, wear appropriate personal protective equipment (PPE) to minimize exposure to hazardous chemicals. This may include gloves, safety goggles, face masks, aprons, or respiratory protection, depending on the product and application.
Follow Dilution Instructions
Follow dilution instructions provided by the manufacturer when mixing concentrated cleaning products with water. Avoid over-diluting or under-diluting products, as this can affect their effectiveness and may result in inadequate cleaning or disinfection.
Avoid Mixing Chemicals
Never mix different commercial cleaning products together, as this can produce harmful chemical reactions, toxic fumes, or even explosions. Follow manufacturer recommendations and use products as directed to ensure compatibility and safety.
Use in Well-Ventilated Areas
Use commercial cleaning products in well-ventilated areas to minimize exposure to fumes or vapors. Open windows or doors, use exhaust fans, and avoid working in confined spaces without adequate ventilation when using chemical-based cleaning products.
Clean Up Spills Promptly
In the event of a spill or leak, clean up commercial cleaning products promptly using appropriate spill containment and cleanup procedures. Wear PPE and use absorbent materials, such as spill kits or absorbent pads, to contain and absorb spills and prevent them from spreading.
Conclusion
Proper storage and use of commercial cleaning products are essential for maintaining a safe and healthy workplace environment. By following best practices for storing, handling, and using these products safely, you can minimize hazards, reduce risks, and ensure effective cleaning and disinfection. Remember to read product labels and SDS, store chemicals securely, segregate hazardous materials, use PPE, follow dilution instructions, avoid mixing chemicals, use in well-ventilated areas, and clean up spills promptly to protect yourself and others from harm.
Need Commercial Cleaning Products in Davenport, IA?
Here at Industrial Technology Corporation, we are committed to ensuring the safety and effectiveness of commercial cleaning products in your workplace. Our expertise in providing top-quality cleaning solutions is matched by our dedication to educating our clients on best practices for storage and handling. By partnering with us, you can confidently maintain a clean, safe, and healthy environment for your employees and customers.
Reach out to us today to learn more about how our products and guidance can help you minimize hazards and maximize cleanliness in your operations.
Maintaining cleanliness in commercial environments is essential for the health and well-being of occupants and visitors. However, in sensitive environments such as healthcare facilities, schools, childcare centers, and food processing plants, choosing the right cleaning products is critical to ensure effective cleaning while minimizing the risk of adverse reactions or contamination. In this guide, we’ll explore how to choose commercial cleaning products for sensitive environments, highlighting key factors to consider and offering tips for selecting safe and effective cleaning solutions.
Understanding Sensitive Environments
Definition and Examples
Sensitive environments are spaces where occupants may be more vulnerable to the effects of cleaning products due to factors such as age, health conditions, or the nature of activities conducted in the space. Examples include hospitals, clinics, nursing homes, schools, daycare centers, food preparation areas, and facilities serving individuals with allergies or respiratory sensitivities.
Importance of Proper Cleaning
In sensitive environments, proper cleaning is paramount to maintain a safe and healthy environment for occupants. Effective cleaning helps remove dirt, germs, and contaminants, reducing the risk of illness, infection, and allergic reactions. However, using harsh or inappropriate cleaning products can exacerbate health issues or cause adverse reactions, highlighting the need for careful product selection.
Factors to Consider When Choosing Cleaning Products
Safety and Non-Toxicity
The safety of cleaning products is of utmost importance in sensitive environments. Look for products that are non-toxic, hypoallergenic, and free from harsh chemicals, fragrances, and irritants. Consider certifications such as Green Seal, EcoLogo, or Safer Choice, which indicate that the product has been independently tested and meets stringent environmental and health standards.
Effectiveness and Performance
While prioritizing safety, it’s also essential to ensure that cleaning products are effective at removing dirt, bacteria, and other contaminants. Look for products with proven efficacy against common pathogens and soil types found in the specific environment. Consider factors such as contact time, application method, and compatibility with surfaces to ensure optimal cleaning results.
Environmental Impact
In addition to safety and effectiveness, consider the environmental impact of cleaning products. Choose products that are biodegradable, phosphate-free, and formulated with renewable or sustainable ingredients. Look for eco-friendly packaging options such as recyclable or compostable containers to minimize waste and reduce environmental footprint.
Tips for Selecting Safe and Effective Cleaning Solutions
Conduct a Risk Assessment
Before selecting cleaning products, conduct a thorough risk assessment of the sensitive environment to identify potential hazards, vulnerabilities, and specific cleaning requirements. Consider factors such as the age and health status of occupants, the presence of allergens or contaminants, and any regulatory or industry standards that must be met.
Consult with Experts
Consult with cleaning professionals, environmental health specialists, or product manufacturers to gather information and recommendations on suitable cleaning products for sensitive environments. They can provide valuable insights into product selection, usage guidelines, and best practices for maintaining cleanliness and safety.
Test Products Before Use
Before using new cleaning products in sensitive environments, conduct a small-scale test to evaluate their compatibility, efficacy, and potential impact on occupants. Test products in inconspicuous areas or on sample surfaces to assess their cleaning performance and any adverse reactions or sensitivities.
Conclusion
Choosing the right commercial cleaning products for sensitive environments requires careful consideration of safety, effectiveness, and environmental impact. By prioritizing non-toxicity, efficacy, and eco-friendliness, you can ensure a clean and healthy environment for occupants while minimizing the risk of adverse reactions or contamination. Conducting a risk assessment, consulting with experts, and testing products before use are essential steps in selecting safe and effective cleaning solutions. With proper product selection and implementation, you can maintain cleanliness and safety in sensitive environments and promote the well-being of occupants and visitors alike.
Need Commercial Cleaning Products in Davenport, IA?
Here at Industrial Technology Corporation, we understand the critical importance of maintaining cleanliness in sensitive environments. Our commitment to providing safe, effective, and environmentally-friendly cleaning solutions ensures that healthcare facilities, schools, childcare centers, and food processing plants remain sanitary and safe for all occupants. We are dedicated to helping you select the best products that meet rigorous health and environmental standards.
Reach out to us today to discover how our expertise and high-quality cleaning products can support your needs and enhance the well-being of those in your care.