Chemical compatibility testing is the bench-scale evaluation of how raw materials, the finished formula, and its packaging behave together before a full commercial batch is ever blended. It screens for separation, unexpected heat or gas, pH drift, and container damage while a problem still costs a few beakers of material instead of a few thousand gallons. For any brand moving a liquid or powder formula into larger volumes, this step protects product quality, worker safety, and the schedule you promised your customers.
A formula that looks flawless in a 500 mL beaker can behave very differently in a large vessel, in a warehouse, or on a truck. Mixing energy, heat build-up, ingredient addition order, and storage conditions all change at scale. Knowing how your ingredients interact first lets a blending partner adjust the formula, choose the right containers, and set realistic production timelines. It also makes every later step, from custom blending capabilities to final packout, more predictable.
Why Chemical Compatibility Testing Comes Before Every Custom Blend
Skipping early screening does not remove risk. It simply moves the risk to the most expensive place to discover it. A separated emulsion, a gelled concentrate, or a drum that swells in storage each trace back to an interaction that a short bench evaluation could have caught. Pre-blend screening turns those unknowns into data you can act on.
What Happens at the Bench Before a Full Batch
Bench work starts with a formulation review. A technical team looks at every ingredient, its concentration, its role in the formula, and the order in which ingredients are added. Small test batches are then blended and observed under controlled conditions. Technicians watch for cloudiness, layering, precipitation, temperature change, gas evolution, and changes in color or odor, then record how the sample holds up over hours, days, and weeks.
The results show whether the formula can move forward as written, needs a minor adjustment, or requires a different ingredient altogether. That decision is far easier to make before raw materials are purchased and before packaging is ordered.
Where Feasibility Review Fits in Toll Blending
Feasibility review sits between the first conversation about your product and the first production run. It bridges laboratory concepts and multi-ton manufacturing, and it is where the most consequential decisions about a formula are made. For brand owners who outsource production, it is also the stage where expectations about performance, shelf life, and packaging are aligned with what the chemistry can actually deliver.
The process applies to brand-new formulas and to reformulations alike. When a supplier discontinues an ingredient or a price spike forces a substitution, the same screening confirms that the replacement behaves like the original. It is equally valuable for liquid formulations that depend on stable viscosity and for dry mixes that must stay uniform from the blender to the end user.
Common Mixing Hazards the Screening Is Designed to Catch
Some incompatibilities are well documented, and they explain why a documented review comes first. The table below lists examples that blending teams are trained to recognize.
Combination
Potential Result
Why Early Screening Matters
Hypochlorite bleach with ammonia-containing products
Release of irritating chloramine vapors
Cleaning concentrates often contain several reactive ingredients at once
Hypochlorite bleach with acids
Release of chlorine gas
A pH adjustment meant to improve performance can create a hazard
Strong oxidizers with organic solvents
Rapid heat, fire risk, or pressure build-up
Solvent-based degreasers and oxidizing additives should never be paired without testing
Concentrated acids with concentrated bases
Strong exothermic reaction and splashing
Addition order and cooling must be planned before scale-up
Surfactants with incompatible salts or electrolytes
Cloudiness, layering, or loss of viscosity
Visible only after hours or days, so it needs a timed observation window
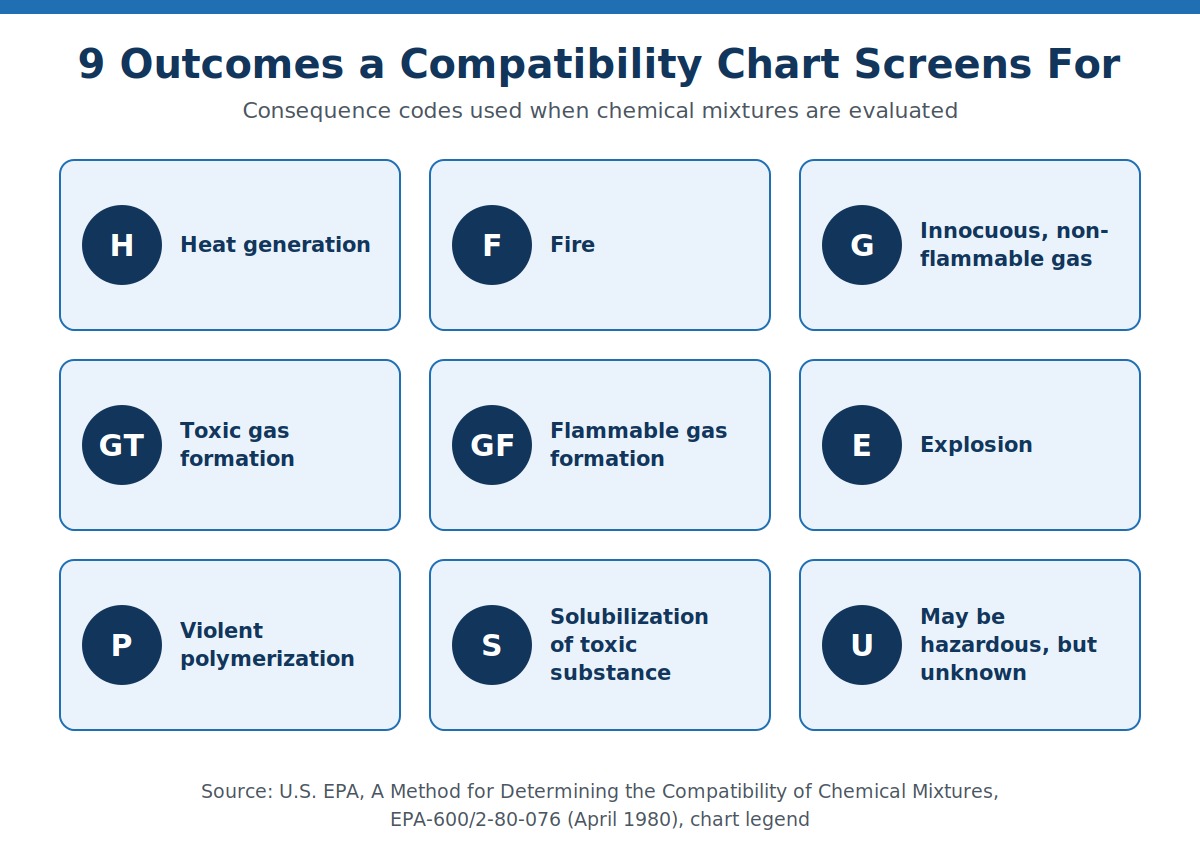
Published reactivity data can flag many of these pairings in advance. A free reactivity prediction tool built for responders and planners shows which hazards, such as heat or gas generation, may arise when two substances meet. It is a useful starting point for a formulation review, though it does not replace hands-on bench evaluation of your actual blend.
Core Parameters Evaluated During Pre-Blend Formulation Screening
A thorough review does not rely on a single measurement. It combines several tests that each reveal a different way a formula can fail. Together they describe how the product will behave during blending, filling, storage, and use.
pH Stability and Drift
pH determines whether a formula stays stable or slowly changes character. A shift can alter cleaning performance, deactivate an active ingredient, or make a mixture more corrosive than intended. In concentrated industrial products, even a small drift can contribute to container damage or an unsafe handling condition. Testing at the start of the study and again after aging establishes a baseline and shows how well the formula buffers itself.
Viscosity and Flow Behavior
Viscosity tells you whether the product pours, pumps, and disperses the way your customers expect. Think of it like concrete slump: too thin and the product migrates or leaks, too thick and it will not move through dispensing equipment. Measuring viscosity at several temperatures confirms that the formula flows properly in a cold warehouse as well as on a warm production floor. This matters especially for surfactant-based cleaners, which can thicken or thin sharply as concentration and temperature change.
Thermal Reactivity and Gas Evolution
Some ingredient combinations release heat, generate gas, or build pressure as they interact. Technicians monitor temperature and watch for bubbling or venting during small-scale mixing, then repeat the test with the intended addition order and rate. This is particularly relevant for car wash concentrates and for solvent-heavy degreasers, where oxidizing and organic components can share the same formula.
Emulsion and Phase Stability
Emulsions combine ingredients that do not naturally stay mixed, so they depend on surfactants and mixing energy to hold together. The failure mode is quiet. A batch can look perfect at the end of blending and then separate into distinct layers on a shelf. Timed observation, centrifuge screening, and temperature cycling reveal weak emulsions early. Teams developing emulsion-based products benefit most from this step.
Freeze-Thaw and Accelerated Aging
Products rarely live at room temperature. They are stored in unheated buildings, loaded onto trucks in summer heat, and delivered in winter. Freeze-thaw cycling and elevated-temperature aging compress months of real-world exposure into a short evaluation window. A formula that separates after one freeze or darkens after a week of heat is far better discovered in a lab than in a customer complaint.
Summary of Core Tests
Test
What It Reveals
Problem It Prevents
pH measurement over time
Chemical stability and buffering strength
Drift that weakens performance or increases corrosivity
Viscosity at multiple temperatures
Flow, pumping, and dispersion behavior
Leaking, clogging, or poor dispensing
Thermal and gas monitoring
Heat release and pressure generation
Exothermic events and pressurized containers
Emulsion and phase observation
Separation, creaming, or precipitation
Non-functional layers on the shelf
Freeze-thaw and heat aging
Resilience across storage and transit conditions
Permanent separation, gelling, or discoloration
Material Compatibility Testing for Packaging and Equipment
A formula can pass every raw material test and still fail because it attacks its own container. Material compatibility testing evaluates how the finished product interacts with drums, totes, bottles, closures, and the equipment used to blend and fill it. A product that degrades its packaging has simply moved the failure to a warehouse, a truck, or a customer facility.
How Chemical Compatibility Testing Protects Containers and Closures
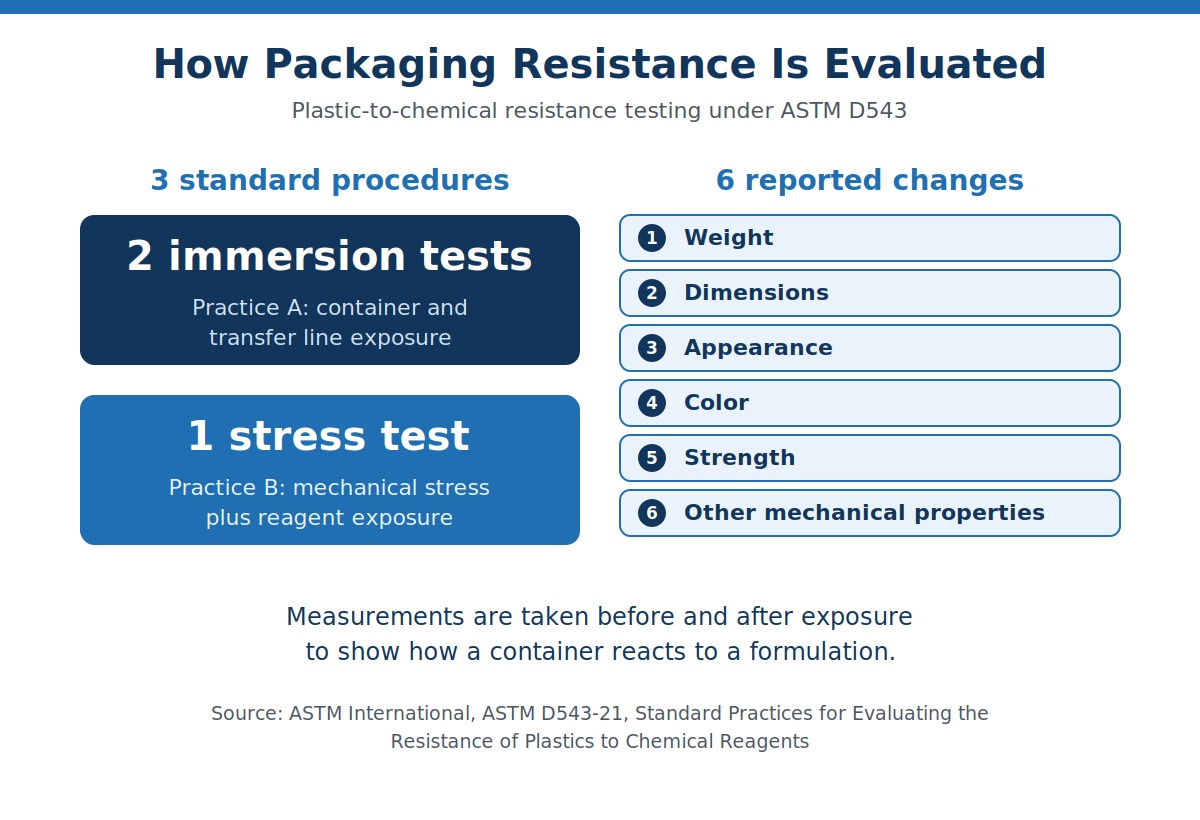
Packaging evaluation exposes sample containers or material coupons to the finished formula under controlled, often elevated, temperatures. The samples are weighed, measured, and inspected before and after exposure. Recognized immersion and stress-cracking practices look for changes in weight, dimensions, appearance, color, and strength, which together show whether a container will hold up through its intended shelf life.
Plastic Drums, Totes, and Bottles
Plastics can soften, swell, craze, or crack when certain solvents, surfactants, or fragrance oils sit against them for weeks. Stress cracking is especially tricky because a container can look fine until it is handled or stacked. Permeation is another concern, since volatile ingredients can migrate through container walls and cause weight loss or odor problems.
Steel Pails and Lined Containers
Acidic and alkaline formulas can corrode bare steel, and chloride-bearing products can attack many metals. Lined containers add protection, but the liner itself must resist the formula. Evaluating both the liner and any exposed seams or fittings prevents leaks that only show up after a long storage period.
Seals, Gaskets, and Closures
Small components cause outsized problems. O-rings, bung gaskets, and cap liners can swell, shrink, or harden in contact with a formula, and a failed seal is a leak waiting to happen. Testing these parts alongside the container confirms the entire closure system works as a unit.
Packaging Component
Typical Concern
What Testing Confirms
Plastic drums and totes
Softening, swelling, stress cracking, permeation
Container keeps its shape, weight, and strength through shelf life
Steel pails and drums
Corrosion from acidic, alkaline, or chloride-bearing formulas
Bare metal or lining resists the formula without pitting
Liners and coatings
Blistering, peeling, or dissolving
Lining stays intact and does not contaminate the product
Gaskets, O-rings, and cap liners
Swelling, shrinking, or hardening
Closure stays leak-resistant after exposure
Once a container is chosen, the next question is how the filled product will be handled. Programs that include hazmat-ready containers need verified material compatibility before labeling and shipping rules can be applied with confidence. Brands running recurring fill schedules can also lock in an approved container through contract fill and pack programs, so every run uses the same tested components.
The Operational Cost of Skipping Pre-Production Screening
The cost of an untested formula shows up in several ways, and most of them are avoidable. A failed batch means lost raw materials, lost labor, and lost production time. A container that fails in storage means damaged inventory and possible cleanup. A product that separates in a customer’s hands means returns, replacement shipments, and a damaged reputation.
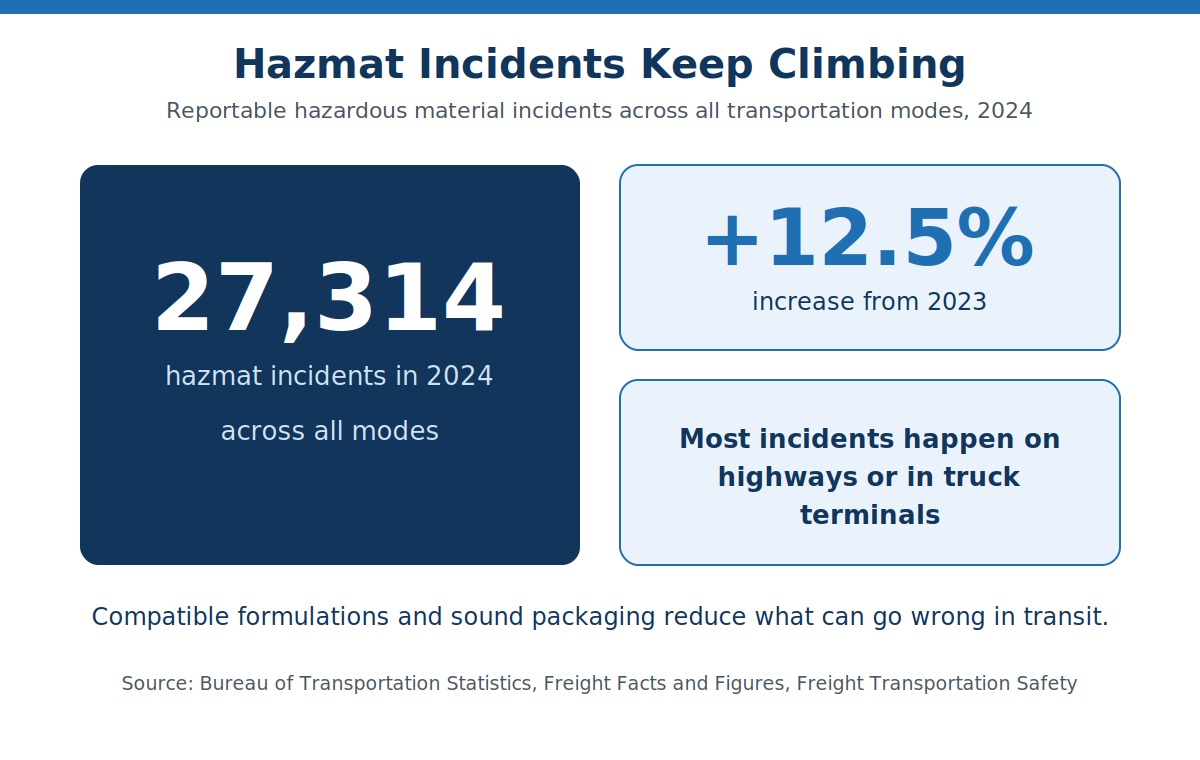
Transportation adds another layer. Hazardous material incidents across all transport modes reached 27,314 in 2024, up 12.5 percent from 2023, and most occur on highways or in truck terminals. A compatible formula in a verified container is far less likely to contribute to that kind of event.
Warehouse and Storage Risks
Storage conditions can quietly undermine a product that was stable on the day it was made. Heat, cold, light, and time all give slow reactions a chance to progress. Reviewing how a finished product will be held matters just as much as reviewing how it will be blended, which is why storage and outbound shipping conditions belong in the early conversation.
Planning for Realistic Timelines
Early testing also makes schedules more reliable. When stability data, packaging approvals, and addition order are settled in advance, production runs move forward without surprise holds. Customers who share their target launch dates up front let the team plan the right number of aging checks and decide which tests can run in parallel.
Reformulation and Ingredient Substitution Strategies
Compatibility work is not only a safeguard. It is also the way to change a formula with confidence. Ingredient shortages, cost pressure, and evolving customer expectations all push brands to adjust what goes into a product, and each change needs the same discipline as the original design.
Validating Substitute Ingredients
Swapping one ingredient for another can change viscosity, foaming, stability, color, and corrosivity all at once. Running the substitute through the same battery of tests as the original shows whether the finished product performs equivalently. Brands building private label product lines often rely on this step to keep multiple formulas consistent when suppliers change.
Reducing Hazard at the Source
Input substitution replaces a more hazardous raw material with a safer one without simply diluting the waste stream. Examples include moving from a harsh solvent to a lower-VOC or bio-based alternative, or replacing an unstable additive with a more robust one. Compatibility screening is what proves the safer option actually works in the finished product. The same logic applies to specialty chemical formulas where performance requirements are tight and small changes can have large effects.
How ITC Approaches Intake-to-Feasibility Review
Industrial Technology Corporation is a family-owned manufacturer with more than 40 years of experience blending and packaging chemical products for customers nationwide. Its intake-to-feasibility process is designed to confirm that a formula can be made safely and consistently before production begins.
Formula intake: Share your ingredient list, concentrations, target specifications, and intended packaging.
Raw material review: Each ingredient is reviewed for compatibility, handling needs, and known hazards.
Bench-scale screening: Small test batches are evaluated for pH, viscosity, thermal behavior, and phase stability.
Packaging evaluation: The formula is checked against the containers and closures planned for production.
Formula adjustment: If a problem appears, the team recommends changes to ingredients, order of addition, or packaging.
Production planning: Approved formulas move into scheduling with documented parameters and realistic timelines.
Because the review covers both formula and container, customers avoid the common problem of solving one issue while creating another. The same team understands the industries ITC supports, so recommendations reflect how products are actually used, stored, and shipped in each market.
Frequently Asked Questions About Chemical Compatibility Testing
What is the difference between chemical compatibility and chemical stability?
Chemical compatibility describes how two or more materials interact when combined, including whether they cause reactions, separation, or damage. Chemical stability describes how a single finished formulation holds its properties over time under conditions such as heat, cold, and light. Compatibility is evaluated first, during feasibility review, and stability testing then continues across the intended shelf life.
How does temperature affect compatibility during storage and shipping?
Extreme temperatures can speed up reactions, weaken emulsions, and cause ingredients to precipitate. Freeze-thaw cycling and heat aging recreate those conditions in a controlled way. A formula that passes at room temperature but separates after a single freeze is not truly stable, so temperature testing is a standard part of a thorough review.
What is a common example of chemical incompatibility in blending?
Mixing hypochlorite bleach with ammonia-containing products releases irritating chloramine vapors, and mixing bleach with acids can release chlorine gas. In industrial blending, strong oxidizers combined with organic solvents, or acids added to bases without controlled cooling, can create dangerous heat, gas, or pressure. Pre-production screening is designed to catch these interactions before they reach a mixing vessel.
How do you know if a formula is compatible with plastic packaging?
Plastic samples such as HDPE or PET are exposed to the formula, often at elevated temperatures, and then inspected for swelling, softening, stress cracking, discoloration, and weight change. This accelerated approach compresses months of storage into a short evaluation window and gives reliable evidence about long-term container performance before any drums are filled at production scale.
Is bench-scale testing enough, or is scale-up testing needed too?
Bench-scale testing identifies most chemistry and packaging problems early, but mixing energy, heat transfer, and addition rates change in larger vessels. A well-run program treats the bench evaluation as the first gate and then confirms performance during the first production-scale batch with in-process checks and finished-product testing.
When should compatibility testing be repeated?
Repeat screening any time an ingredient, supplier, concentration, or container changes. Even a change that seems minor, such as a new grade of surfactant or a different drum liner, can alter how a formula behaves. Treating each change as a mini feasibility review keeps product quality consistent from one production run to the next.
Start Your Formulation Review
If you are preparing to scale a liquid or powder product, confirming compatibility first is the most reliable way to protect your investment. To discuss your formula, your packaging plans, and your timeline, contact the ITC team today. You can also learn more about the company behind the process at Industrial Technology Corporation.
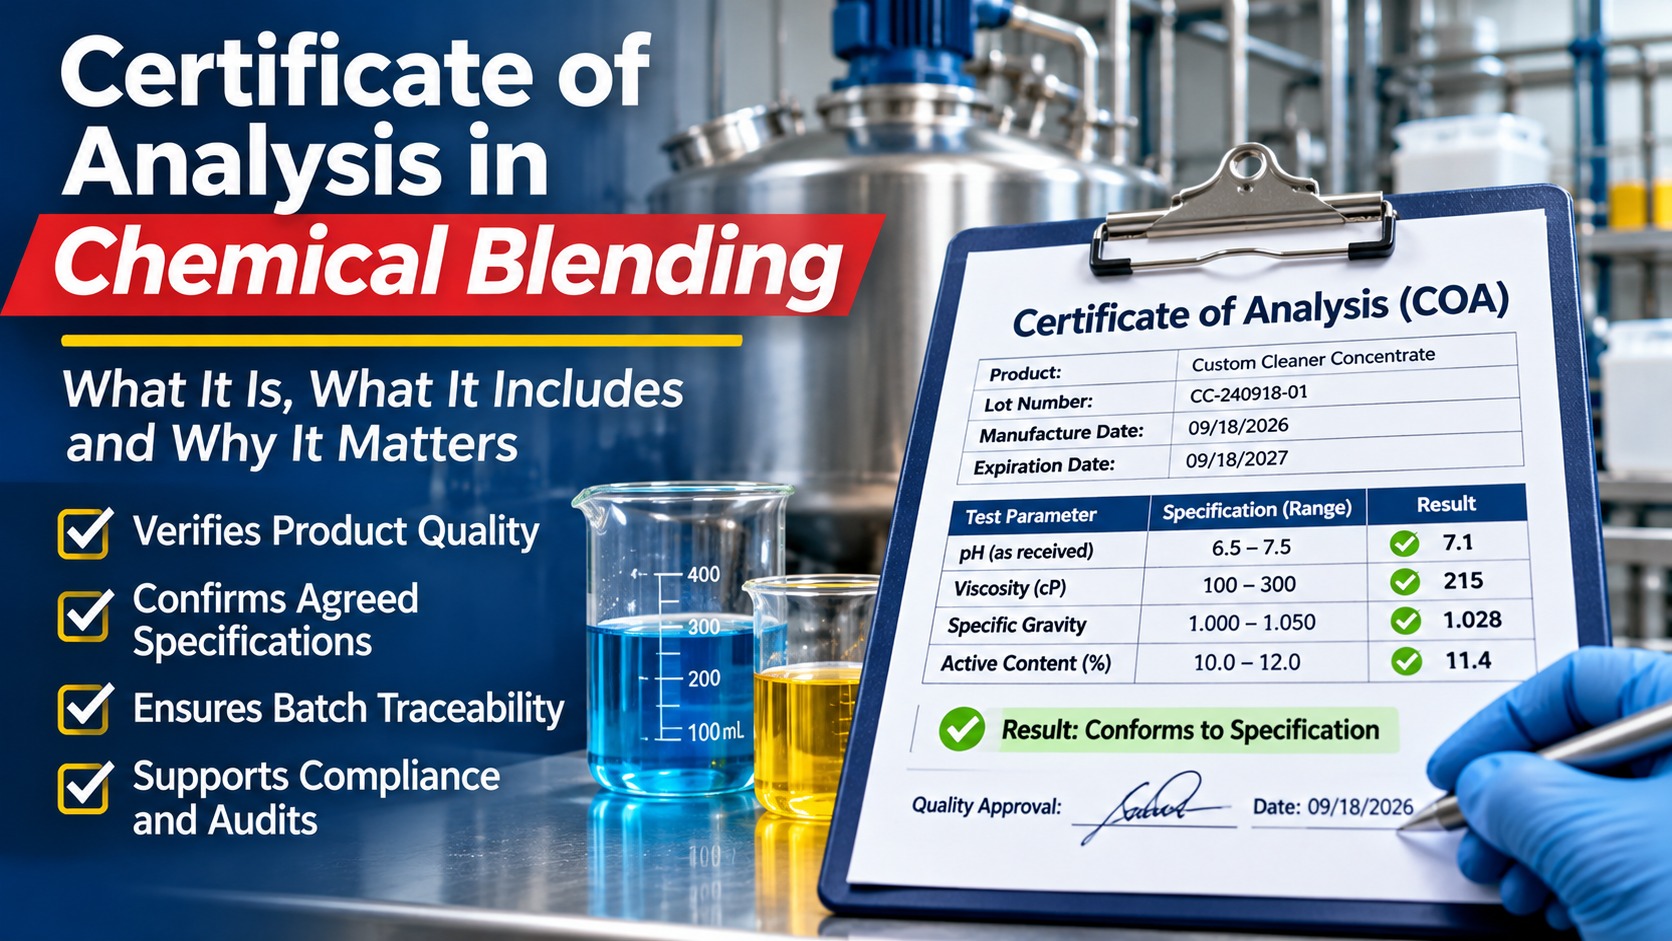
A certificate of analysis in chemical blending is a formal, batch-specific document that verifies a custom chemical mixture meets its agreed specifications based on quality control testing. It is not a product brochure or a generic technical summary. It is measured evidence, tied to one lot number, that the formulation in the container matches what was ordered.
For procurement managers and quality specialists, an off-spec batch has immediate and concrete consequences. A car wash concentrate blended at the wrong pH can strip coatings instead of cleaning them. An industrial degreaser with an active ingredient outside tolerance fails on the line and triggers a root-cause investigation that costs hours and credibility. A commercial cleaner that performs differently from one batch to the next wears down customer trust in a way no discount repairs. The certificate of analysis, usually shortened to COA, is the record that keeps those problems from reaching your floor.
At Industrial Technology Corporation, a COA accompanies every batch of custom liquid and powder formulations we blend, because documentation is part of the manufacturing job and not an administrative afterthought.
How a Certificate of Analysis in Chemical Blending Works
A COA is not interchangeable with a product specification sheet. A specification sheet describes what a formulation is designed to do and the parameters it should meet. A batch COA reports what one specific lot measured during testing, which shows the gap, if any, between a design target and a confirmed result. For teams managing supply chain risk, that difference matters, because a target is an intention and a measurement is a fact.
Chemical mixtures are hard to verify by inspection. Two blends can look identical in the drum and still differ in concentration, pH, or viscosity enough to change how they perform. Batch-level documentation gives your quality team numbers to work from instead of assumptions, and it gives you something concrete to compare against the ranges you agreed on before production began.
What Happens Before a Certificate of Analysis in Chemical Blending Is Issued
The COA is the final step in a quality control sequence that begins before blending starts. Raw materials are verified on receipt, testing equipment is calibrated against certified reference standards, the batch is blended, and samples are tested against the agreed specification ranges. Only then does a qualified person review the results and sign the document. Because the instruments were checked against verified standards first, the measurements on the COA rest on a documented baseline, which is what makes the record defensible when an auditor or a downstream customer asks for proof.
Agreed Specifications Come First
Before production, we work with each customer to define acceptable ranges for the parameters that matter most to their application. Those ranges become the acceptance criteria in the results table of the COA. Testing methods are chosen to suit the formulation, since a thin water-based wash concentrate and a dry powder blend do not need the same protocol.
Key Components of a Chemical Blending COA
The parameters tested vary by product. pH and viscosity matter most for liquid cleaners, while moisture content and bulk density are important for powders. The structure of the document stays consistent, which lets a receiving team verify shipments quickly regardless of which product is on the dock.
Section
What It Contains
Why It Matters
Header and manufacturer information
Blending facility, contact details, and the customer purchase order reference
Ties the document to the right order and supplier
Product and lot identification
Product name, product code, and unique lot number
Must match the container label for traceability
Specifications and test results
Parameters tested, minimum and maximum limits, measured results, and test methods
The core evidence that the batch is on spec
Dates and shelf life
Manufacture date, test date, and expiration or retest date
Confirms stability over the intended service life
Quality approval
Name, title, signature, and date of the reviewer
Creates accountability for the release decision
Why the Signature Matters
A COA without a named, qualified signatory is a data sheet with a logo on it. The signature shows that a qualified person reviewed the results, compared them with the agreed ranges, and judged the batch fit for release. That accountability is what makes the document useful during an audit or a field failure investigation. The lot number deserves the same attention: it should match the label on every container, whether a 5 gallon pail or a bulk tanker, and our packaging and labeling options are set up so the two always agree.
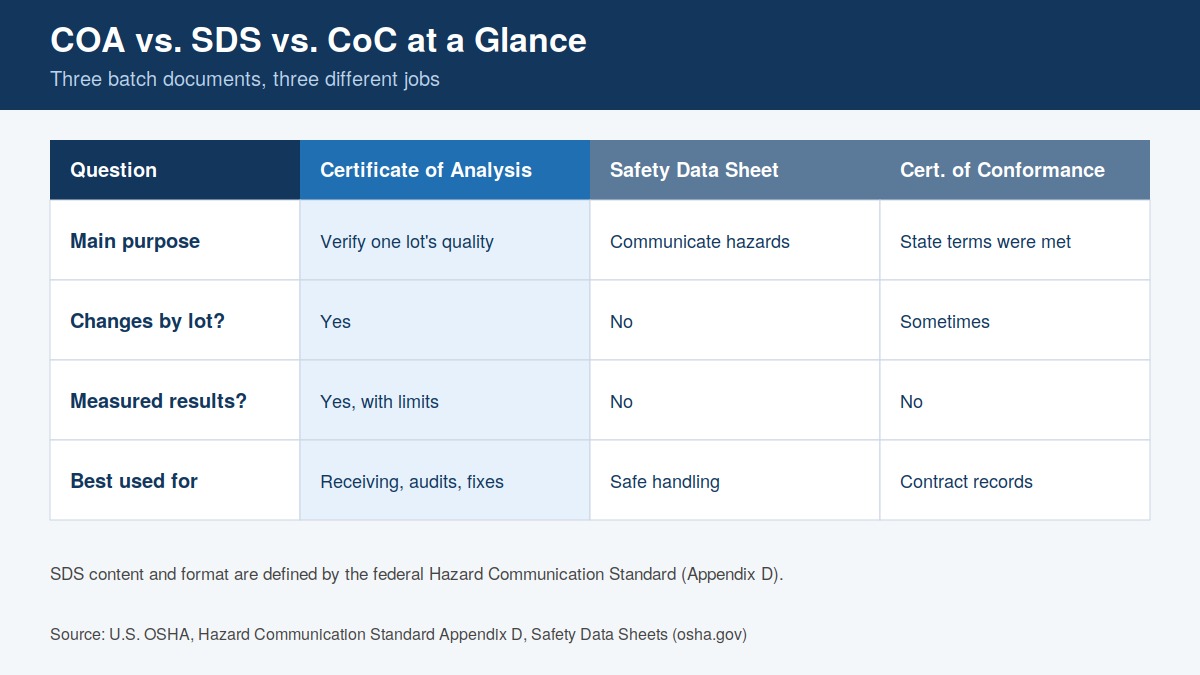
COA vs. SDS vs. CoC: Understanding Batch Documentation
Procurement teams new to toll blending often ask why a COA is needed when they already have the safety data sheet. The two documents answer different questions and cannot stand in for each other.
Safety Data Sheet (SDS)
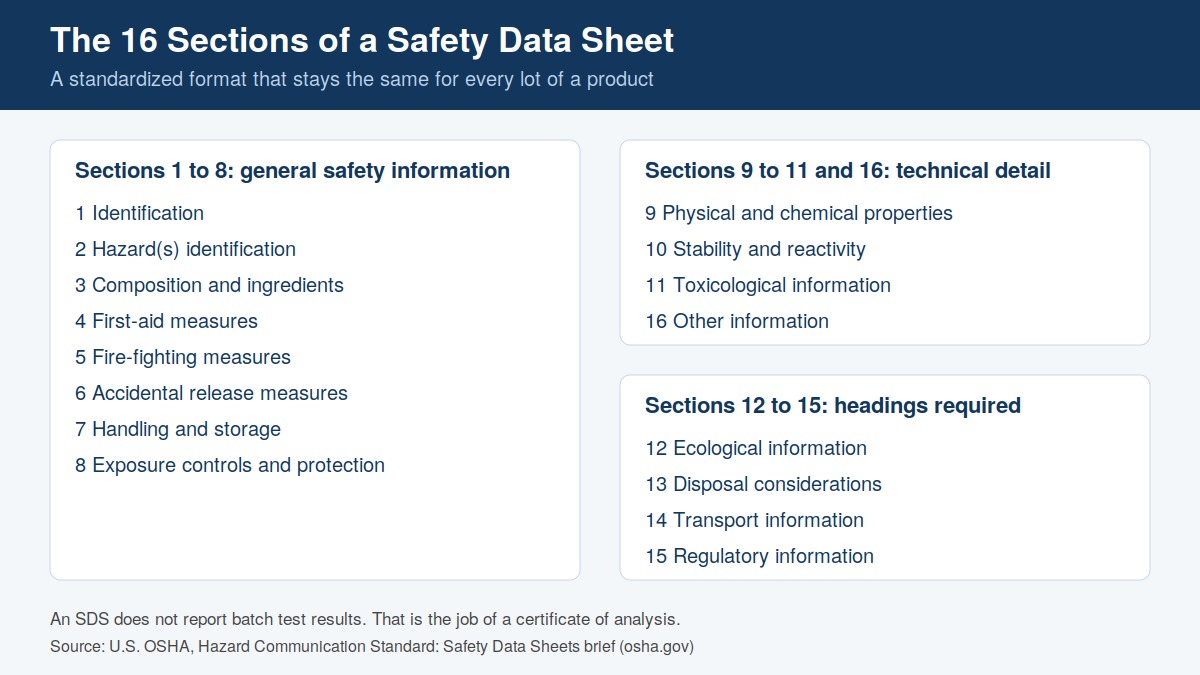
An SDS is a standardized hazard communication document. Under federal rules it follows a 16-section format covering identification, hazards, composition, first aid, handling, exposure controls, and related topics. It describes the product category and does not change from lot to lot. The SDS tells your receiving team how to handle the material safely. It does not tell your quality team whether a particular batch is correct.
A certificate of conformance is a signed statement that a shipment meets contract terms. It usually contains no test data, no measured values, and no analytical verification. That makes it a contractual declaration rather than a quality record. A quality specialist cannot use it to confirm active ingredient concentration, check a dilution ratio, or investigate a failure in the field, because there are no numbers to work with.
An Easy Way to Remember the Difference
Think of an SDS as the owner’s manual for a vehicle model, written for every unit of that model and explaining how to operate it safely. A COA is the inspection report on the specific vehicle you just bought, with the exact readings and tolerances for that unit. The manual is generic to the design, and the inspection report is specific to the one in your driveway.
Document
Main Purpose
Batch-Specific
Contains Measured Results
Certificate of analysis (COA)
Verify quality and specification compliance for one lot
Why a COA Is Critical for Quality Assurance and Compliance
Compliance depends on proof. Facilities that operate under a recognized quality management framework, such as ISO 9001 quality management requirements, document how products are verified, and a COA is one of the records that shows the system working. It gives auditors a paper trail, supports compliance checks on regulated properties such as volatile organic compound content when that parameter is part of the agreed specification, and links a specific production run to the standards it was built to meet.
When a regulatory or customer inquiry arrives, and in industrial chemical manufacturing it eventually does, the COA answers it with measured data rather than memory. It is much easier to respond to a question about a lot shipped months ago when the lot number, test results, dates, and approver are already on a single signed record.
Compliance Support for Specific Product Types
If you formulate products for the transportation sector, such as wash concentrates, wheel brighteners, or surface preparation chemistries, your batch records need to hold up under both customer and regulatory scrutiny. Our automotive chemical blending capabilities pair precise production with complete batch transparency, and our car wash concentrate production follows the same documentation standard. Industrial maintenance products are handled the same way through our degreaser manufacturing.
Operational Benefits of Working With a Blender That Provides a COA
Lower supply chain risk: Off-spec material is caught before it enters your production line, which prevents downtime and avoidable recalls.
Faster receiving inspections: Your team matches the lot number on the container to the COA and verifies results against the agreed ranges, which removes guesswork at the dock.
Evidence-based troubleshooting: If a product behaves unexpectedly in the field, such as a cleaner struggling in hard water, the measured data helps you investigate stability or adjust dilution without starting over.
Audit readiness: Signed, dated, lot-specific records make quality reviews faster and less stressful.
Consistency across batches: Comparing COAs from repeat orders shows whether a product is holding steady over time.
These benefits apply whether the product is a liquid or a dry blend. Our liquid formulation production and dry powder blending each use test parameters suited to the physical form of the product.
What to Look for in a Blending Partner
A blender’s willingness to issue a detailed, signed, batch-specific COA on every run tells you a lot about how it operates when no one is watching. If your current supplier struggles to provide consistent documentation or to hit your specifications, it is reasonable to compare options. Brands selling under their own name have even more at stake, since their reputation rides on every shipment, which is why documentation is built into our private label production. You can also see the range of sectors we support under industries served, and how finished product moves from release to delivery through warehousing and shipping.
How to Read and Use a COA When It Arrives
A COA only protects you if someone checks it. A simple receiving routine takes a few minutes and catches most documentation problems before material is released to production.
Confirm the lot number on the COA matches the label on every container in the shipment.
Check that the product name and code match your purchase order.
Compare each measured result with the minimum and maximum limits listed for that parameter.
Verify that the manufacture date, test date, and expiration or retest date make sense for the product.
Confirm the document is signed and dated by the approving reviewer.
File the COA with the receiving record so it can be found by lot number later.
If Something Does Not Match
If the lot number or any result does not line up, hold the material and contact your blending partner before it is used. A mismatch breaks the chain of traceability, and it is far easier to resolve at the dock than after the product has been dispensed or shipped to your own customers.
Frequently Asked Questions
What is the difference between a COA and a certificate of conformance?
A certificate of conformance is a signed statement that a shipment meets contract terms, and it typically contains no measured data. A certificate of analysis is a batch-specific quality document that lists the actual test results and specification ranges for one lot. If a batch fails in the field, a certificate of conformance gives you nothing to investigate, while a COA gives you the numbers.
Who issues a certificate of analysis in chemical blending?
The chemical manufacturer or toll blender that performed the blending and quality control testing issues the COA. It should be signed and dated by a qualified quality specialist or chemist who verified the results, not by a sales or logistics representative. The signature creates a clear line of accountability from the test data to the person who approved the release.
How long should a company keep certificates of analysis?
Retention periods depend on your quality system, customer contracts, and any rules that apply to your industry or product. Many companies keep COAs at least through the shelf life of the product, and some keep them longer to support audits and complaint investigations. Confirm the requirement with your compliance team and keep each COA filed by lot number so it can be retrieved quickly.
Can a COA be used to verify VOC content for commercial cleaners?
Yes, when volatile organic compound content or a related property such as specific gravity is included in the agreed test parameters. The COA then shows the measured value for that batch, which gives you a record to support compliance reviews. Tell your blender early which regulated properties you need reported so they are added to the specification.
What should I do if the lot number on the container does not match the COA?
Do not use the material. A mismatch means you cannot confirm that the document describes what is in the container. Contact your blending partner right away to obtain the correct batch-specific COA before releasing the product to production.
Do all chemical blenders provide a COA with every batch?
Not necessarily. Some suppliers issue a certificate only on request, or provide a certificate of conformance without test data. Ask any prospective partner whether a signed, lot-specific COA with measured results is included with every run, and review a sample before you commit.
Get Batch Documentation Your Quality Team Can Rely On
A certificate of analysis is the most direct answer to a question every quality manager eventually asks: how do I know what is in this container? It turns a shipment into a verified, traceable, and auditable asset that supports production confidence, compliance, and troubleshooting. Every run we complete ships with a COA that reflects the agreed specifications, the measured results, and the signature of the professional who verified them. To discuss your formulation and the parameters you need documented, reach out to our team or call (563) 322-4882. Our contract blending programs are built to support your quality goals from initial scoping through full-scale production.
If you are comparing contract manufacturers, the chemical toll blending minimum order quantity a partner requires is one of the first numbers that shapes your budget, your inventory plan, and your launch timeline. Procurement teams and product managers are usually asking two questions at once: how much cash do I need to commit up front, and how much room do I have to scale up or down later? The honest answer is that minimums come from physical equipment limits and raw material buying rules far more than from any arbitrary policy meant to protect margin.
Knowing where those limits come from gives you leverage. You can design formulations around standard ingredients, choose packaging that fits the batch, and sequence pilot and commercial runs so you never pay to produce more than you can sell. At Industrial Technology Corporation, we walk customers through this math before the first batch is scheduled, and this guide lays out the same logic in plain terms.
What Determines a Chemical Toll Blending Minimum Order Quantity
A minimum order quantity is the smallest volume of a custom formulation a blender can produce in one run while keeping the batch uniform and covering the real cost of running the equipment. Four forces set that floor: vessel geometry, changeover labor, raw material purchasing, and packaging format. Each one is physical or logistical, which means each one can be planned around once you understand it.
Why Every Chemical Toll Blending Minimum Order Quantity Starts With the Vessel
Mixing vessels are engineered to work within a fill range. The liquid level has to cover the impeller so the batch circulates, and in temperature controlled formulations it has to cover enough of the jacketed wall for heating or cooling to work. In dry blending, the powder bed has to reach the agitator so the material is actually lifted and folded. Run below that range and the blender is no longer making a batch at all, it is moving material around without mixing it evenly.
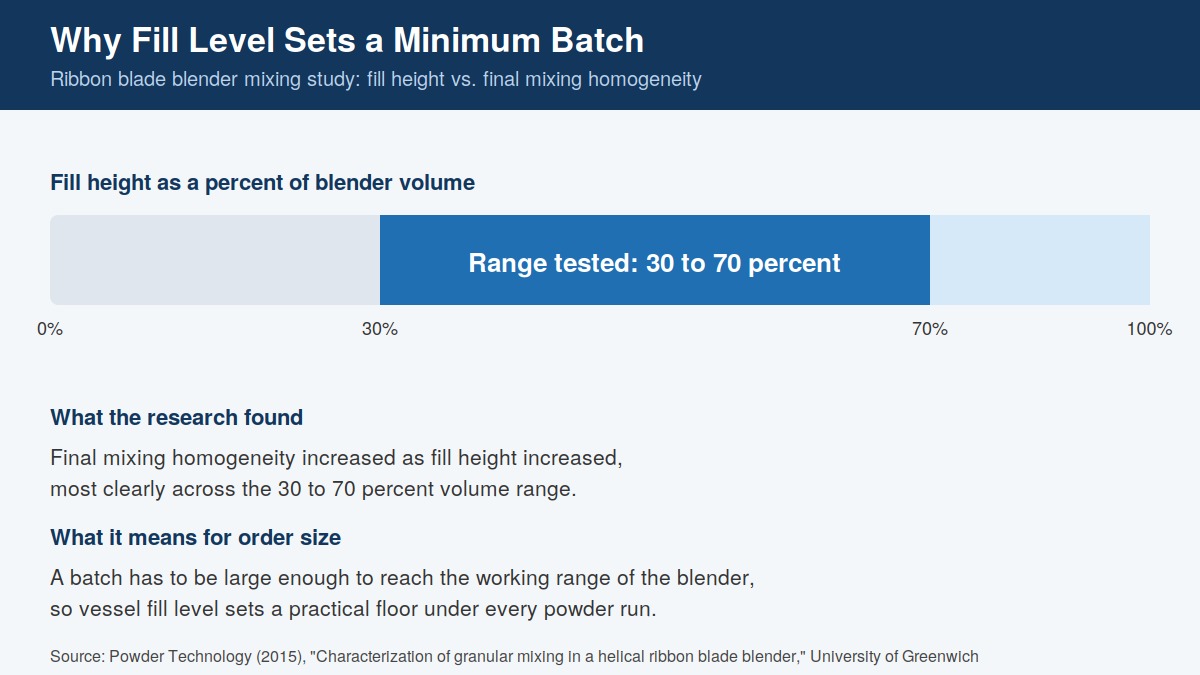
Research on ribbon blade mixers supports this. In one peer-reviewed study of granular mixing in a ribbon blade blender, final mixing homogeneity increased as fill height increased, most clearly across the 30 to 70 percent volume range that was tested. Equipment makers also commonly advise against operating a ribbon blender below roughly 30 to 40 percent of its rated volume, because the agitator cannot generate enough contact with the product.
Clean-Down Time and Changeover Costs
Between formulations, equipment has to be cleaned thoroughly so one customer’s chemistry never carries into the next. Flushing lines, cleaning vessels, and verifying the equipment is ready takes labor and takes the vessel out of production. That cost is fixed whether the run is small or large, so a very small batch carries a heavy changeover burden per gallon or pound. When a blender prices a short run, a meaningful share of the price is the cleaning, not the blending. Customers who run the same formulation repeatedly, or who group similar products together, spread that cost across more volume.
Raw Material Purchase Minimums
Suppliers sell ingredients in drums, totes, bags, and pallets. If your formula calls for a small amount of a specialty surfactant, solvent, or additive, the blender may still need to buy a full container to fulfill the run. That purchase minimum becomes a floor under the blender’s own minimum, and it can quietly raise the effective MOQ of every run that uses the ingredient.
Consolidate formulations so several products share the same specialty inputs.
Share your annual forecast so the blender can buy ahead and spread the purchase across scheduled runs.
Summary of the Main MOQ Drivers
Driver
What It Controls
How You Can Plan Around It
Vessel size and fill range
Smallest batch that mixes uniformly
Match batch volume to a vessel that fits it
Clean-down and changeover
Fixed labor cost per run
Group similar products and use repeat scheduling
Raw material pack sizes
Minimum ingredient purchase
Standardize inputs and share annual forecasts
Packaging format
Filling cycles and leftover product
Align batch size with whole container counts
Viscosity and chemistry
Pump, motor, and vessel compatibility
Confirm equipment fit early in development
Liquid vs. Powder Batch Size Minimums
Liquid and dry blending are different operations, so their minimums are calculated differently. A blender with a fleet of mid-size tanks will set a different floor than one running large powder vessels, and neither will match a generic number you read in an industry overview. The only reliable way to learn a real minimum is to describe your product and let the blender match it to the right equipment.
Liquid Tank Constraints
Liquid production is organized around tank capacity, pump flow rates, and temperature control. The tank has to hold enough liquid to submerge the impeller and keep the batch stable, and viscosity changes everything. A thick industrial degreaser needs different pumps and mixing energy than a thin, water based wash concentrate, so a blender running both will not apply the same minimum to each. Customers developing car wash concentrates or industrial degreasers should raise viscosity and foaming behavior early, because both affect which tank and pump the batch needs. For a closer look at tank based production, see our liquid formulation capabilities.
Powder Blender Fill Levels
Dry blending relies on ribbon blenders or plow mixers, where the physical volume of the vessel sets a hard lower boundary. You need enough material to generate the shear and folding action that produces a homogeneous blend, and there is no workaround for a blender running at a small fraction of its rating. The practical result is that powder minimums are often tied to the usable working volume of the blender, which is lower than the total shell volume. Our ribbon blender powder production is organized around exactly this constraint.
Packaging is one of the most overlooked drivers of the minimum you will actually be quoted. Smaller containers such as 5 gallon pails take more filling cycles, more labor, and more handling per unit of product than drums, totes, or bulk tankers. That operating cost shows up in the minimum run a blender will accept for a given container. If you are still deciding between formats, our packaging configurations from pails to bulk can be matched to your expected volume.
Heel and Yield Loss
Batch volume should also line up with the container count. Any product left behind in the vessel after filling, known as heel, is lost yield and adds to clean-down work before the next run. A batch sized to fill a whole number of drums or totes wastes less than one that leaves a partial container and a residue in the tank.
Regulated Products and Hazmat Handling
Formulations that ship as regulated materials need compliant containers, labels, and documentation, and that can influence which pack sizes make sense. Planning for hazmat ready packaging at the start avoids a late change to container size that would force a different batch volume.
Pilot, Small Batch, and Commercial Run Types
Most product launches move through three stages, and each stage has a different goal. Choosing a partner who can support all three prevents the handoff problems that appear when development happens in one facility and production in another.
Run Type
Purpose
Planning Notes
Pilot batch
Validate chemistry, stability, and packaging compatibility
Smallest commitment; confirm the formula before any market commitment
Small batch run
Regional market tests and niche industrial applications
Limits inventory risk and protects cash flow
High volume run
National distribution and repeat supply
Per unit cost improves and scheduling becomes predictable
Running a full commercial volume on an unproven formula is a cash flow risk most businesses cannot justify, which is why a pilot stage is worth building into the plan. Brands that sell under their own label often start with a pilot and then expand, and our team supports that path for private label product lines from the first sample through repeat production.
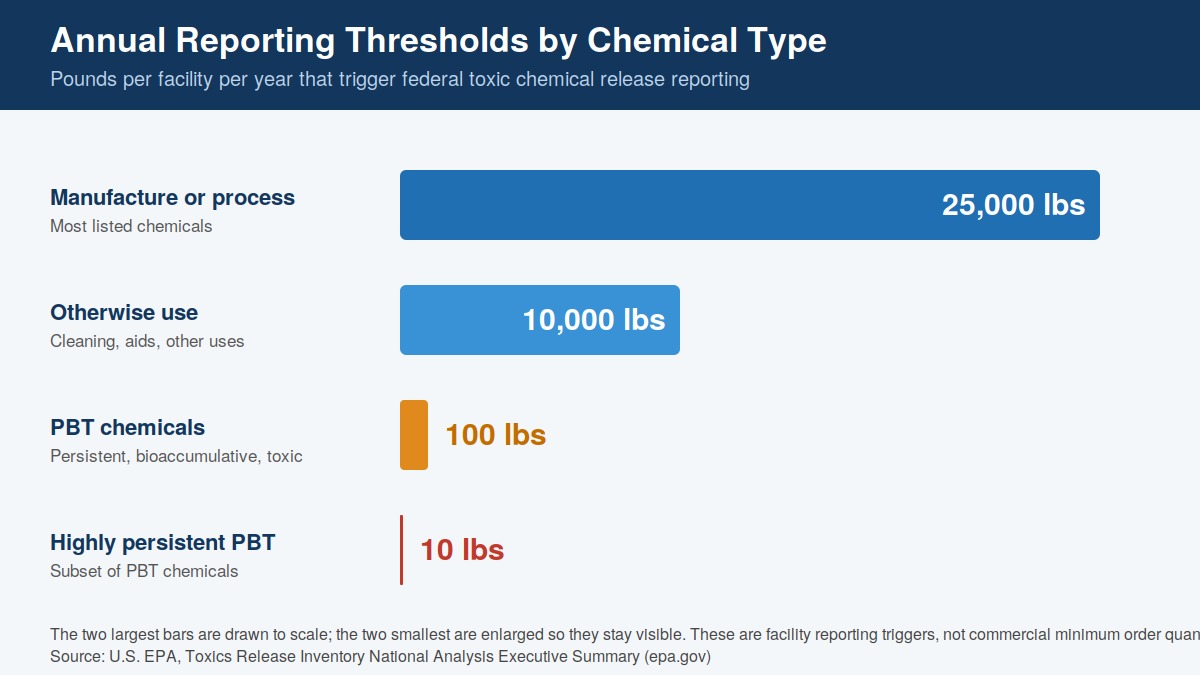
Federal Reporting Thresholds Are Not the Same as Order Minimums
Buyers sometimes confuse a blender’s commercial minimum with the annual quantity thresholds that trigger federal toxic chemical release reporting. They are separate. The reporting thresholds apply to a facility’s yearly totals, not to your order, but they influence how a blending partner schedules, tracks, and documents runs that involve listed chemicals. Under the national program, the standard annual threshold is 25,000 pounds for manufacturing or processing a listed chemical and 10,000 pounds for other use. Chemicals that persist and accumulate in the environment face far lower triggers, down to 100 pounds and 10 pounds.
If your formulation includes regulated solvents or other listed ingredients, raise them in your first conversation so reporting, documentation, and volume planning are handled together from day one.
How to Negotiate and Scale Order Quantities
Minimums are rarely fixed in stone. The variables behind them, including equipment scheduling, raw material purchasing, and clean-down time, respond to good planning. Buyers who arrive with a clear picture of annual volume, formulation complexity, and packaging requirements regularly get better terms than those who open with a single run and no forward view. Our full scope contract blending programs are built to flex around that kind of forward planning.
Commit to Annual Volume With Scheduled Releases
An annual volume agreement with scheduled release dates gives the blender predictable scheduling and lets them buy raw materials in larger, cheaper quantities. That predictability reduces the per run overhead they need to recover, which is often the lever that makes a lower minimum possible.
Standardize Ingredients and Share the Forecast
Formulas built around readily available inputs avoid the purchase minimums that inflate small runs. Sharing a realistic twelve month forecast, even a rough one, helps the blender plan purchasing and schedule equipment time around your demand curve.
Use One Partner From Development Through Commercial Production
Keeping pilot and commercial work with the same blender removes the technical transfer that often causes formulation drift. It also builds a shared record of what the formula needs at each scale.
Scaling From Pilot Batch to Full Production
Moving from a pilot to a commercial batch is where many quality problems begin. Viscosity behavior, mixing time, and ingredient feed rates all shift as batch size grows, and those shifts are not always linear or predictable from bench scale data. Each increase in scale should be checked against the pilot sample, with adjustments documented so the commercial batch matches what you approved.
What to Verify at Each Scale Increment
Viscosity and appearance compared with the approved pilot sample
Mixing time and agitation settings for the larger vessel
Ingredient addition order and feed rates
Packaging compatibility and fill accuracy at the new container size
Stability results before the first full commercial release
Once a product is running at volume, outbound logistics matter as much as the blend itself. Our warehousing and outbound freight support lets finished product be stored and released against your demand instead of all at once. We serve customers across many sectors, and you can see the full range of industries we support when you are mapping your product to the right production approach.
Frequently Asked Questions
What is MOQ in chemical manufacturing?
MOQ stands for minimum order quantity. In contract chemical manufacturing it is the lowest volume a blender can produce in one run while covering operating costs and keeping the batch consistent. The floor is set by physical equipment limits such as vessel size and impeller geometry, and by operating costs such as clean-down labor and setup time. Batch consistency is the firm constraint, because a run that is too small for the vessel can produce material that does not meet specification.
What are typical minimums for chemical toll blenders?
Minimums vary with whether the product is a liquid or a dry powder, the blender’s equipment, the packaging format, and raw material sourcing. Some large blenders require truckload volumes before they schedule a run, while more flexible partners can accommodate smaller batches for development or niche applications. Because a real number depends on your formulation, the best way to learn it is to describe the product and request a custom quote.
How does scaling from pilot batch to full production work?
The process starts with a small pilot batch to validate chemistry, stability, and packaging. After the pilot meets specification, the formula moves to a larger vessel with mixing time, ingredient feed rates, and temperature adjusted for the new scale. Using the same blender for both stages reduces the risk of formulation drift during technical transfer.
Are there flexible toll manufacturing options for small batches?
Yes. Some toll blenders support small batch work for new product launches, regional tests, and niche applications where volume is naturally limited. Small runs help manage cash flow and inventory risk during validation, and packaging can scale from pails to bulk as demand grows.
How does capacity planning affect a chemical toll blending minimum order quantity?
Capacity planning schedules equipment, labor, and raw materials across a mix of large runs and small custom batches. A facility running near capacity may need larger minimums to justify a schedule change, while one with open time can be more flexible. Sharing an annual forecast helps the blender plan ahead and often supports smaller or more frequent runs.
Why do powder and liquid products have different minimums?
Liquid blending is limited by tank volume, impeller coverage, pumps, and temperature control, while powder blending is limited by the working volume of ribbon blenders or plow mixers. Viscosity matters on the liquid side, and particle size and bulk density matter on the powder side, so the same batch volume does not suit both.
Plan Your Next Blending Run
Understanding a blender’s minimums turns a procurement detail into a supply chain planning tool. The businesses that handle it well enter the conversation knowing their annual volume, formulation complexity, and packaging needs, which shortens onboarding and reduces cost surprises. Tell us about your product and we will recommend a batch size, packaging format, and scale up path that fits it. You can request a custom blending quote online or call (563) 322-4882 to talk through your formulation.
Surfactant manufacturing services must deliver precise chemical performance on the plant floor, not just in a laboratory report. When production lines require consistent foaming, wetting, and emulsification for car wash concentrates, industrial degreasers, or commercial cleaners, basic mixing setups often fail. Relying on off-the-shelf blends can lead to costly batch separation, clogged dispensing equipment, and product failure. Consistency is non-negotiable.
Scaling a formulation means adjusting an existing recipe or developing a new one to handle complex physical chemistry. Working with an experienced custom toll blending partner provides access to specialized mixing technology, rigorous quality control, and bulk raw material procurement without the capital expense of an in-house chemical plant. Understanding the mechanics of the chemical blending process is critical for any operations manager transitioning a liquid or powder formulation from a lab-scale concept to high-volume commercial production.
Formulation Support & Compatibility Testing: Evaluating HLB values, raw materials, and chemical stability to prevent phase separation.
Precision Blending & Dilution: Using high-shear mixing and temperature-controlled vessels to blend anionic, cationic, nonionic, and amphoteric surfactants in liquid and powder formulations.
Viscosity & Gel-Phase Management: Controlling rheology through precise electrolyte addition and polymer thickeners.
Production Scaling & Packaging: Transitioning formulas from pilot batches to 5,000+ gallon commercial runs with packaging ranging from 5-gallon pails to bulk tankers.
What Do Surfactant Manufacturing Services Include?
Outsourced surfactant production covers the entire lifecycle of a product, starting in the laboratory and ending at the loading dock. Professional custom toll blending offers capabilities designed to handle the unique physical and chemical properties of surface-active agents. This begins with formulation support: technical teams review raw material specifications, evaluate Hydrophilic-Lipophilic Balance (HLB) values ranging from 0 to 20, and modify existing formulations to ensure chemical stability across all operating conditions.
Once the formulation is finalized, the process moves to physical production. Contract partners use specialized surfactant blending to compound anionic, cationic, nonionic, and amphoteric surfactants into completely homogeneous liquid and powder formulations. This stage involves precise dilution and viscosity management. Concentrated surfactants are notoriously prone to forming highly viscous liquid-crystalline gel phases when mixed with water. Just as a chef modifies a sauce’s fat content to change texture, surfactant ratios control how a cleaner spreads, foams, or cuts through grease. Manufacturers use temperature-controlled vessels, typically maintained between 40°C and 60°C, and controlled addition sequences to navigate around these gel zones. Without this precision, an entire batch can lock into an unpumpable state. Gel phases halt production.
Common Applications for Blended Surfactant Products
Surfactant blends serve as the functional backbone of industrial fluids. Single surfactants are rarely enough to satisfy all performance requirements at once, so manufacturers engineer multi-part mixtures to target specific soils, substrates, and operating environments.
Agricultural Adjuvants: Manufacturing specialized wetting agents, spreaders, and surfactants for herbicides to improve crop protection, leaf coverage, and rainfastness.
Car Wash Concentrates and Industrial Degreasers: Formulating high-foaming detergents, industrial degreasers, and commercial cleaners engineered to target specific soil types and grease. See car wash chemical blending for more on this application.
Personal Care & Cosmetics: Blending mild, skin-compatible amphoteric and nonionic surfactants for liquid soaps and industrial hand washes.
Oilfield & Industrial Fluids: Manufacturing emulsifiers and demulsifiers designed to perform under extreme temperatures and pressures.
How Surfactant Blending Supports Product Performance
The physical chemistry of surfactants governs how they behave at interfaces. Chemistry drives performance, and custom toll blending adjusts these molecular interactions to deliver specific performance characteristics in the finished product.
Optimized Wetting Speed: Lowering interfacial tension to allow rapid liquid penetration and spreading across solid surfaces.
Controlled Emulsification: Matching precise HLB values to keep unmixable oil and water phases permanently suspended in stable, microscopic droplets.
Tailored Foam Profiles: Engineering formulations for either high-density, long-lasting foam stabilization or rapid foam collapse using specialized antifoaming agents.
Enhanced Detergency: Combining anionic surfactants for soil removal and nonionic surfactants for hard-water tolerance to achieve a combined cleaning power that neither class delivers independently.
Surfactant Manufacturing Services for Cleaners, Degreasers, and Industrial Products
Industrial cleaning applications demand stable chemical systems that can withstand harsh operating environments. Custom toll blenders formulate and blend products tailored to these rigorous demands. Industrial degreasers, for instance, require highly alkaline environments, often operating at pH levels between 10 and 13, to support the saponification of fats and oils. pH stability is critical. Manufacturers blend strong alkalis such as sodium hydroxide or sodium metasilicate with specialized surfactants that remain stable and active at high pH without degrading or falling out of solution. For a closer look at how this chemistry applies specifically to degreaser formulation, see degreaser contract blending.
Metal parts washers present a different set of constraints entirely. These systems require low-foaming nonionic surfactants, specifically ethylene oxide/propylene oxide (EO/PO) block copolymers, combined with corrosion inhibitors to clean metal substrates without causing foam overflow or oxidative damage. To optimize detergency and wetting across diverse surfaces like concrete, plastic, and glass, formulators rely on specific anionic-to-nonionic surfactant ratios, typically ranging from 70:30 to 50:50. Outsourcing these complex formulations to a dedicated industrial cleaning chemical blending provider helps ensure that industrial cleaners and car wash concentrates perform consistently under heavy soil loads, batch after batch.
In surfactant manufacturing, the order of addition is just as critical as the chemical formula itself. Introducing water to a concentrated surfactant too quickly can lock the entire batch into an unpumpable gel phase, which is exactly why precise process controls matter at every stage of production.
Managing Concentration, Foam, Wetting, and Emulsification
To achieve optimal performance, a surfactant blend must balance several competing physical mechanisms at once. Formulators must first ensure that the surfactant concentration in the final working solution remains well above the critical micelle concentration (CMC), where industrial formulations typically target 3 to 5 times the CMC, to maintain active detergency under heavy soil loads. That threshold matters because below it, micelle formation collapses and the cleaning agent loses its ability to solubilize oils and suspend particulates. Second, while some applications require sustained, dense foam, many industrial processes demand rapid collapse, so manufacturers incorporate specialized defoaming agents that disrupt foam films through interfacial spreading and bridge-dewetting mechanisms. By carefully blending low-HLB and high-HLB surfactants, manufacturers at once lower interfacial tension, allowing the solution to spread rapidly across solid surfaces (wetting), and disperse oils into stable, microscopic droplets (emulsification), achieving both functions within a single, unified formulation. This is where operational reality intersects with chemistry: if filling equipment runs at 50°F, a formula that pours like honey at room temperature becomes an immediate supply chain bottleneck. Temperature dictates flow.
Why Batch Consistency Matters in Surfactant Production
In industrial applications, even minor compositional drift, such as a viscosity shift of 200 cP or a pH drift of 0.3 units, can cascade into product failures, clogged dispensing equipment, or rejected shipments. Maintaining strict batch consistency requires a layered quality control framework, not just a final-product check. Testing prevents failure. Rigorous analytical testing protocols at every production stage, consistent with quality benchmarks published by ASTM International, are what separate reliable contract manufacturers from those who simply have tank capacity.
Incoming Raw Material Verification: Quality control teams test every incoming lot of raw surfactant using Fourier-transform infrared spectroscopy (FTIR) or Raman fingerprinting to verify identity and purity before production begins.
In-Process and Finished-Batch Testing: Operators pull samples during and after the blending process to measure critical physical properties, including pH, specific gravity, and viscosity, to ensure batch consistency.
Moisture and Active Content Analysis: Chemists perform Karl Fischer titration to precisely measure water content, alongside chromatographic methods (HPLC or GC) to verify active surfactant concentrations and impurity profiles.
Viscosity Adjustments: Electrolyte addition, typically sodium chloride, for viscosity control in surfactant concentrates is managed within tight tolerances, usually ranging from 0.1% to 10% by weight of the total formulation, to prevent thinning or over-thickening.
Overcoming the Challenges of Surfactant Scaling
Transitioning a surfactant formula from a 1-liter laboratory beaker to a 5,000-gallon production reactor introduces significant thermodynamic and mechanical factors that bench-scale testing simply cannot predict. Heat transfer rates slow dramatically at volume. This means temperature-sensitive surfactants, particularly those with narrow gel-phase avoidance windows, can degrade or stratify if heating and cooling cycles are not carefully managed through the reactor’s full thermal mass. Mixing energy compounds the problem, since excessive shear in a large vessel entrains air and triggers massive foaming events that halt production lines and can damage agitator seals. Professional chemical production scaling addresses this through computational fluid dynamics (CFD) modeling and staged pilot-scale trials, verifying that the surfactant mixture’s physical behavior, including its rheology, its phase boundaries, and its foam response, remains stable before committing to a full commercial run. It is not a linear scaling problem. It is a process re-engineering exercise. Scale changes physical behavior.
Choosing the Right Surfactant Manufacturing Partner
Open tank capacity is not a differentiator. The meaningful variables are analytical depth, raw material purchasing power, and the ability to meet packaging requirements without forcing a brand into a generic configuration. Tailored packaging options should span the full range, from 5-gallon pails to bulk tankers, with private label capability for businesses building their own brand equity on top of outsourced production. Explore private label chemical packaging for a closer look at container and labeling options. Regulatory alignment matters just as much: a manufacturing partner should operate in full compliance with applicable state and federal environmental standards governing chemical storage, VOC compliance, wastewater discharge, and spill prevention, since their compliance posture directly affects the supply chain risk profile of every brand they work with.
Frequently Asked Questions
What is the difference between toll blending and contract manufacturing for surfactants?
Custom toll blending refers to a service where a brand provides the chemical formula and, in many cases, the raw materials, and the manufacturer blends and packages the product to specification. Contract manufacturing is more complete: the partner assists with formulation modification, sources raw materials, manufactures the product, and manages quality control, safety data sheets, and logistics. The distinction matters when a formula needs modification versus when a locked, validated formula is ready for volume production.
How do manufacturers control viscosity in surfactant blends?
Manufacturers manage viscosity through three primary mechanisms: adjusting the ratio of mixed surfactants to alter micellar architecture, adding precise quantities of electrolytes such as sodium chloride, typically within the 0.1% to 10% by weight range, to thicken or thin the system, and incorporating polymer rheology modifiers like xanthan gum or carbomers to provide low-shear stability and prevent settling during storage or transit.
What packaging options are available for outsourced surfactant production?
Outsourced surfactant manufacturing services handle tailored packaging configurations from 5-gallon pails to bulk tankers. Many facilities also offer private label packaging and custom labeling for commercial end use, which is particularly relevant for distributors building house-brand product lines on top of contract-manufactured formulations.
How is compatibility tested during the formulation review?
Chemists evaluate compatibility and formulation stability by subjecting the surfactant blend to accelerated stability protocols: exposing samples to freeze-thaw cycling and elevated heat storage, monitoring pH drift over time, checking for phase separation or precipitation in hard-water matrices, and verifying that the chemical compound does not degrade or interact adversely with the intended packaging materials. Hydrotrope selection and concentration adjustments often surface as critical variables during this review.
How is intellectual property protected during contract manufacturing?
Reputable contract manufacturers operate under legally binding non-disclosure agreements and maintain strict formulation data confidentiality, helping brands retain exclusive ownership of their chemical intellectual property throughout the manufacturing relationship.
Scaling a surfactant product line requires a partner who treats physical chemistry with the same rigor applied to the production schedule. By outsourcing to a dedicated specialist, brands eliminate capital constraints, compress their supply chain, and help ensure their car wash concentrates, industrial degreasers, or commercial cleaners perform consistently in the field. From initial formulation review to high-volume packaging and distribution, professional surfactant manufacturing services provide the operational infrastructure a business needs to grow without absorbing the overhead of running a chemical blending facility. Outsourcing reduces overhead.
Specialty chemical blending services help manufacturers, distributors, and product developers create precise chemical formulations that meet demanding performance, handling, packaging, and quality requirements. Unlike basic mixing, specialty blending often involves controlled ingredient sequencing, viscosity management, temperature awareness, batch documentation, compatibility review, and production methods designed to protect formula integrity from raw material intake through final packaging. For businesses that rely on chemical products in industrial, commercial, agricultural, cleaning, coatings, adhesives, water treatment, or maintenance applications, the right blending partner can help turn a technical formulation into a consistent, scalable, and market-ready product.
Chemical blending is both a scientific and operational process. It requires an understanding of how ingredients interact, how processing conditions affect final performance, and how production controls reduce variation between batches. A formula may look straightforward on paper, but real-world manufacturing introduces variables such as ingredient order, shear sensitivity, solubility, pH adjustment, thickening behavior, mixing time, raw material quality, packaging compatibility, and storage stability. Specialty chemical toll blenders support these requirements by combining formulation knowledge, production equipment, quality control systems, and packaging capabilities into one coordinated manufacturing process.
For companies without in-house production equipment, toll blending can provide access to experienced operators, mixing vessels, filling lines, batch records, and quality checks without the capital investment of building a chemical manufacturing facility. For companies that already manufacture some products internally, an outside blending partner can add capacity, support overflow demand, handle specialized formulas, or produce products that require equipment or procedures not available in-house.
How Do Specialty Chemical Blending Services Work?
Specialty chemical blending begins with a technical review of the product, the intended application, and the manufacturing requirements. The blending partner evaluates the formula, raw materials, handling needs, production steps, quality specifications, packaging requirements, and any special considerations that may affect consistency or safety. This review helps determine how the formula should be scaled from lab, pilot, or previous production quantities into reliable batch manufacturing.
A typical blending process may include raw material sourcing or customer-supplied ingredients, formula verification, production scheduling, batch sheet development, ingredient staging, controlled mixing, in-process checks, final quality testing, packaging, labeling, storage, and shipment. Each stage contributes to product consistency.
Many specialty formulas require more than adding ingredients to a tank and mixing until uniform. The sequence of addition may determine whether the product hydrates properly, disperses evenly, thickens correctly, or maintains stability. Some powders must be added slowly to prevent clumping. Some liquids must be blended under controlled shear to avoid foam, separation, or degradation. Some formulations require pH adjustment at a specific point in the process. Others require controlled heating, cooling, filtration, or extended mixing time to achieve the target appearance, viscosity, or performance.
A toll blending partner uses production instructions that define the exact manufacturing method. These instructions may include:
Raw material names, lot numbers, and quantities
Required personal protective equipment and handling procedures
Ingredient addition sequence
Mixing speed, mixing duration, and shear requirements
Temperature limits or heating and cooling steps
In-process testing requirements
Target pH, viscosity, density, color, odor, or appearance
Filtration, transfer, and packaging instructions
Labeling, lot coding, and documentation requirements
The goal is repeatability. A successful blending process produces the same finished product from batch to batch, within agreed specifications, while protecting workers, equipment, customers, and end users.
Formula Review, Ingredient Handling, and Production Planning
Before production begins, the blending partner typically performs a formula and process review. This step is important because specialty chemical formulations may include ingredients with unique handling requirements, such as acids, bases, solvents, surfactants, polymers, corrosion inhibitors, chelating agents, preservatives, dyes, fragrances, resins, or functional additives.
Formula review helps identify potential production concerns before they become batch problems. For example, a thickening agent may require pre-wetting or slow dispersion. A surfactant system may be foam-prone if mixed too aggressively. A powder may require dust control or controlled addition. A corrosive ingredient may require compatible tanks, pumps, seals, and transfer hoses. An emulsion may require specific shear conditions to maintain uniformity.
Production planning also includes batch size selection. Some formulas can be scaled easily, while others require adjustment because mixing energy, tank geometry, heat transfer, and ingredient incorporation change as batch volume increases. A good blending partner considers whether the formula is best produced in small pilot batches, mid-size production batches, or full-scale runs.
Ingredient handling is another critical part of specialty blending. Raw materials must be received, identified, stored, and staged properly. Some materials may need segregation, temperature-controlled storage, moisture protection, ventilation, or special transfer methods. Lot traceability is often essential, especially when customers require documentation that links each finished batch to specific raw material lots.
A well-planned blending operation reduces the risk of production delays, contamination, incorrect additions, viscosity drift, off-spec product, packaging issues, and rework. It also helps manufacturers meet customer expectations for lead time, consistency, and documentation.
Specialty Chemical Blending Services for Complex Applications
Specialty chemical blending services are especially valuable when products must meet technical performance standards or serve complex end-use applications. These products may be used in harsh environments, precision processes, regulated industries, or industrial operations where chemical performance affects safety, efficiency, equipment life, or product quality.
Examples of products that may require specialty blending support include:
Complex applications often require specific product characteristics. A cleaner may need controlled alkalinity, foam behavior, wetting action, and residue profile. A coating additive may require dispersion stability and compatibility with downstream systems. A water treatment product may need consistent concentration and solubility. A private label product may need matching appearance, packaging, labeling, and performance expectations across every production run.
Viscosity control is a common challenge in specialty blending. Some products must pour easily, while others need a thicker body for cling, suspension, or controlled application. Viscosity may be affected by ingredient order, hydration time, temperature, shear, pH, salt concentration, and raw material variation. Managing these variables requires process discipline and appropriate testing.
Packaging can also be part of the technical challenge. Chemical products may need to be filled into drums, totes, pails, bottles, jugs, or bulk containers. Packaging materials must be compatible with the finished product. Closures, liners, labels, lot codes, and pallet configurations may also need to meet customer or distribution requirements. A specialty toll blending partner can help align the finished formula with packaging formats that support safe handling, storage, shipment, and end use.
When Businesses Need Custom Chemical Blending Support
Businesses often seek custom chemical blending support when they need production expertise, manufacturing capacity, specialized equipment, private label support, or consistent quality without managing the entire process internally. Toll blending allows a company to outsource production while retaining ownership of its formula, brand, customer relationships, and market strategy.
A business may need blending support when:
It has developed a formula but lacks production equipment
Demand has outgrown internal batch capacity
A product requires specialized mixing, filling, or handling
A company wants to launch a private label chemical product
Internal teams need overflow production support
A formula requires improved batch consistency
A product needs packaging in multiple sizes or formats
A manufacturer wants to reduce capital investment
A business needs technical support for scale-up
Existing production processes are inefficient or inconsistent
Custom blending is also useful for companies entering new markets. Instead of purchasing tanks, mixers, pumps, filling equipment, warehouse space, and quality control systems, a company can work with an established toll blender to produce commercial batches more efficiently. This can shorten the path from formulation to market while allowing the business to focus on sales, distribution, customer support, and product development.
In some cases, businesses turn to a blending partner because their formula is too specialized for a commodity producer. Specialty blends may require careful sequencing, nonstandard ingredients, smaller batch sizes, custom documentation, private labeling, or packaging flexibility. A toll blender that understands technical chemical manufacturing can adapt to these needs more effectively than a high-volume producer built only for standard products.
For established manufacturers, custom blending can support operational resilience. If equipment goes down, demand spikes, labor availability changes, or a new product line requires different capabilities, an outside blending partner can provide supplemental capacity. This flexibility helps protect customer supply while reducing the need to overbuild internal operations.
Quality Control Steps That Protect Blend Consistency
Quality control is central to specialty chemical blending because customers depend on predictable performance. A product that varies in concentration, viscosity, color, pH, or appearance may create application problems, customer complaints, or downstream process failures. Consistent testing and documentation help verify that each batch meets agreed specifications before release. Many of these quality checks draw on standardized test methods published by ASTM International, which are widely referenced across the chemical manufacturing industry to keep testing consistent and results comparable from batch to batch.
Quality control may begin before blending with raw material inspection. Incoming materials can be checked against purchase specifications, certificates of analysis, labels, lot numbers, and physical condition. During production, operators may perform in-process checks to confirm that the batch is developing as expected. After blending, final samples may be tested against finished product specifications.
Common quality control checks may include:
Appearance and clarity
Color and odor
pH
Viscosity
Specific gravity or density
Solids content
Concentration or active content
Weight verification
Fill volume or fill weight
Packaging integrity
Lot coding and label accuracy
Documentation is just as important as testing. Batch records provide a written history of how the product was made, including raw material lots, ingredient quantities, production steps, operator checks, test results, packaging details, and release information. This traceability supports customer confidence and helps investigate any future questions about a batch.
Quality control also protects process repeatability. If a batch requires adjustment, the blender can document what happened and use that information to refine future production. Over time, well-maintained records help identify patterns related to seasonal temperature changes, raw material variation, mixing time, thickening response, or packaging behavior.
For private label and contract manufacturing customers, quality systems help protect the brand. The product may carry the customer’s name, but the manufacturing quality depends on the blending partner’s controls. That makes consistent production, testing, and documentation essential to long-term customer satisfaction.
What to Look for in a Specialty Chemical Blending Partner
Choosing the right blending partner is a technical and strategic decision. The best partner is not simply the company with mixing tanks available. It is the company that understands the formulation, the manufacturing process, the quality expectations, and the commercial goals behind the product.
Businesses should look for a partner with experience handling the type of chemistry involved in their product. Different chemical categories require different equipment, procedures, and expertise. A partner familiar with surfactants, polymers, cleaners, water-based blends, viscous products, concentrates, or private label packaging may be better prepared to anticipate production challenges.
Important capabilities to evaluate include:
Experience with similar chemical formulations
Ability to follow customer-owned formulas and batch procedures
Technical review and scale-up support
Compatible tanks, mixers, pumps, and transfer systems
Viscosity control and in-process testing capabilities
Raw material handling and lot traceability
Flexible packaging options
Private label support
Quality control documentation
Responsive communication and production planning
Ability to handle both small and larger batch requirements
Communication is especially important. A blending partner should ask technical questions before production, clarify formula details, identify potential risks, and communicate if something changes during manufacturing. Strong communication helps prevent assumptions, protects timelines, and supports better outcomes.
Confidentiality also matters. Many businesses rely on proprietary formulas, customer-specific formulations, or private label products. A professional toll blending partner should treat formula details, production information, and customer relationships with appropriate care.
Finally, businesses should consider whether the partner can grow with them. A product may begin as a small production run and later expand into larger volumes, additional fragrances, alternate concentrations, new packaging sizes, or related product lines. A scalable blending partner can support development, launch, growth, and long-term production needs.
FAQ
What are specialty chemical blending services?
Specialty chemical blending services involve the custom manufacturing of chemical formulas that require controlled mixing, ingredient sequencing, handling procedures, quality testing, and packaging. These services are commonly used for industrial, commercial, private label, and technical chemical products.
How is toll blending different from standard mixing?
Toll blending is a contract manufacturing service where a blending partner produces a customer’s formula according to defined specifications. Specialty toll blending often involves more technical controls than standard mixing, including viscosity targets, pH adjustment, process sequencing, compatibility considerations, and detailed batch documentation.
Who owns the formula in a toll blending arrangement?
In many toll blending relationships, the customer owns the formula while the blending partner manufactures the product according to agreed instructions. Ownership, confidentiality, and documentation expectations should be clearly defined before production begins.
Can a specialty blender help with scale-up?
Yes. A qualified blending partner can help evaluate how a lab or pilot formula may behave at the production scale. Scale-up support may include batch size planning, mixing method review, ingredient addition sequencing, viscosity evaluation, and production testing.
What types of packaging can be used for custom chemical blends?
Packaging depends on the product, volume, and distribution needs. Common options include bottles, jugs, pails, drums, totes, and bulk containers. Packaging must be compatible with the finished chemical formulation and suitable for storage, shipping, and end use.
Why is sequencing important in chemical blending?
Ingredient sequencing affects dispersion, solubility, viscosity, pH response, stability, and finished product uniformity. Adding ingredients in the wrong order can cause clumping, separation, excessive foam, incomplete blending, or off-spec performance.
What quality checks are used during specialty chemical blending?
Quality checks may include pH, viscosity, specific gravity, appearance, odor, color, fill weight, concentration, and packaging inspection. The exact tests depend on the formula and the finished product specifications.
When should a business use a toll blending partner?
A business should consider toll blending when it needs custom chemical production, additional capacity, specialized equipment, technical process support, private label packaging, or consistent manufacturing without investing in its own full-scale blending operation.
Partner With Industrial Technology Corporation for Specialty Chemical Toll Blending
Specialty chemical blending requires more than production equipment. It requires technical understanding, controlled processes, careful documentation, and a commitment to consistent results. We support businesses that need dependable custom toll blending services, private label opportunities, and quality chemical formulations designed for real-world industrial and commercial applications.
Whether you need custom toll blending services, private label opportunities, or quality chemical formulations for your business, Industrial Technology Corporation is here to meet your needs. Simply contact us today to inquire about our services, request a quote, or discuss your specific requirements. We look forward to working with you to develop innovative solutions that drive success for your business.