The Industrial Technology Team brings together decades of combined experience in chemical toll blending, contract manufacturing, and industrial packaging. Based at ITC's Davenport, Iowa facility, the team works directly with customers across automotive, agriculture, industrial cleaning, water treatment, and specialty chemical industries to develop custom formulations that meet exact performance and compliance requirements. From liquid and powder blending to private label packaging and hazmat-compliant shipping, the team draws on hands-on production knowledge to speak to the practical realities of scaling a chemical product from formula to finished goods. Their work spans every stage of the toll blending process, giving them a ground-level view of the technical and regulatory considerations that matter most to manufacturers and brand owners. Content published under the Industrial Technology Team byline reflects that operational expertise, aimed at helping businesses make informed decisions about blending, packaging, and contract manufacturing partners.
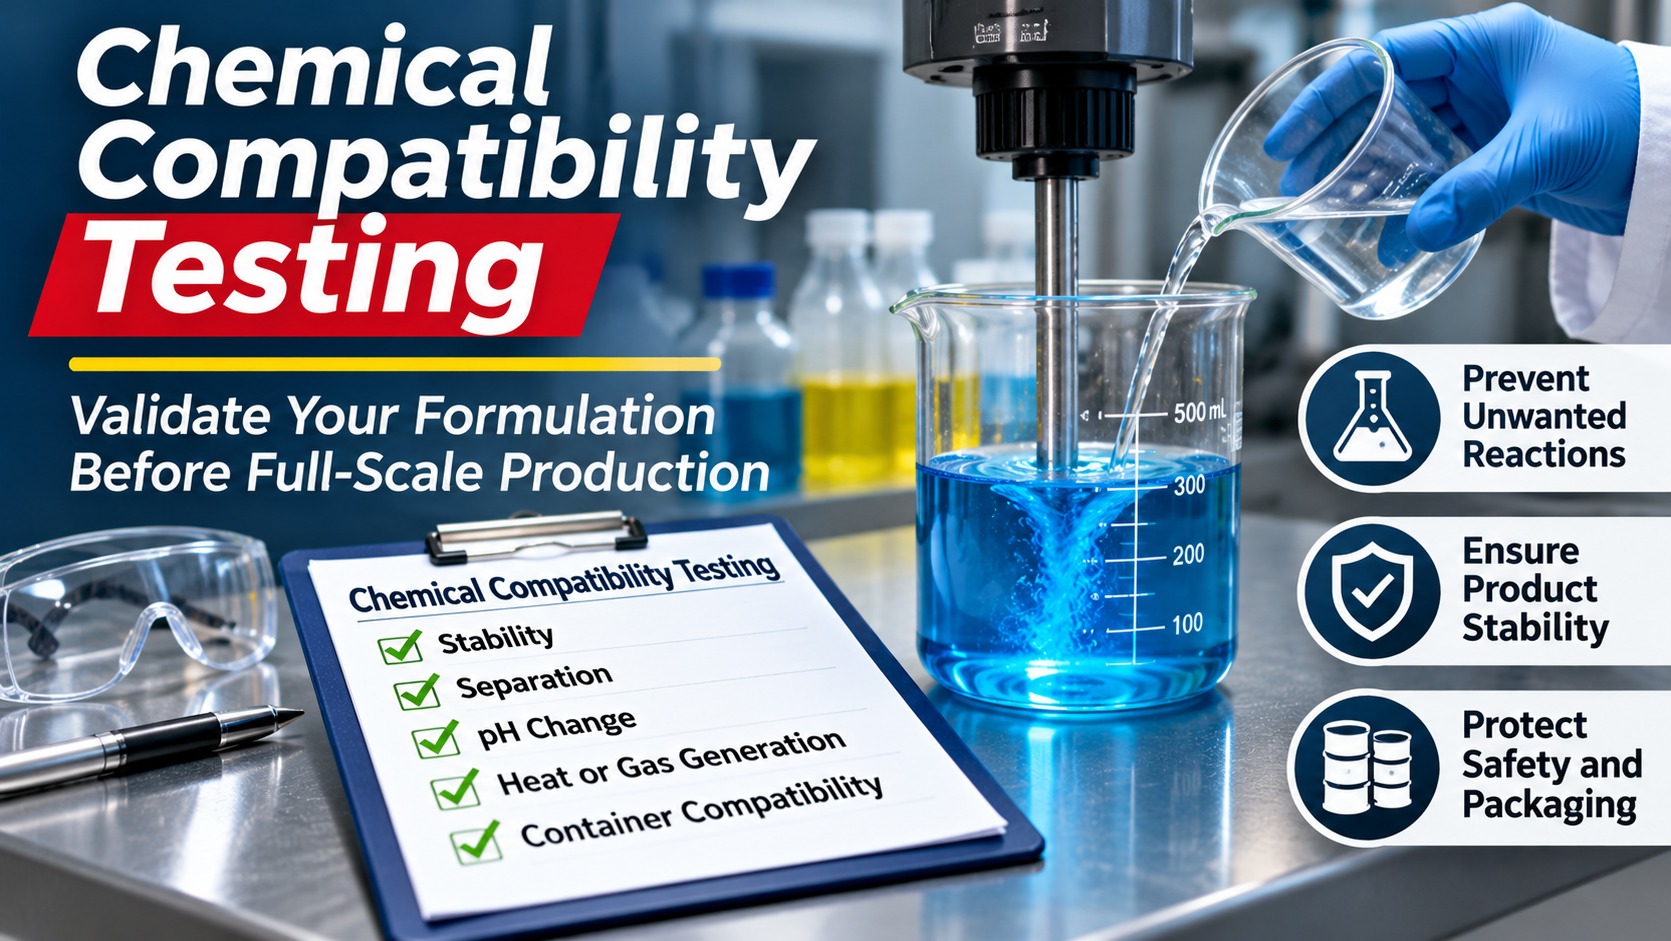
Chemical compatibility testing is the bench-scale evaluation of how raw materials, the finished formula, and its packaging behave together before a full commercial batch is ever blended. It screens for separation, unexpected heat or gas, pH drift, and container damage while a problem still costs a few beakers of material instead of a few thousand gallons. For any brand moving a liquid or powder formula into larger volumes, this step protects product quality, worker safety, and the schedule you promised your customers.
A formula that looks flawless in a 500 mL beaker can behave very differently in a large vessel, in a warehouse, or on a truck. Mixing energy, heat build-up, ingredient addition order, and storage conditions all change at scale. Knowing how your ingredients interact first lets a blending partner adjust the formula, choose the right containers, and set realistic production timelines. It also makes every later step, from custom blending capabilities to final packout, more predictable.
Why Chemical Compatibility Testing Comes Before Every Custom Blend
Skipping early screening does not remove risk. It simply moves the risk to the most expensive place to discover it. A separated emulsion, a gelled concentrate, or a drum that swells in storage each trace back to an interaction that a short bench evaluation could have caught. Pre-blend screening turns those unknowns into data you can act on.
What Happens at the Bench Before a Full Batch
Bench work starts with a formulation review. A technical team looks at every ingredient, its concentration, its role in the formula, and the order in which ingredients are added. Small test batches are then blended and observed under controlled conditions. Technicians watch for cloudiness, layering, precipitation, temperature change, gas evolution, and changes in color or odor, then record how the sample holds up over hours, days, and weeks.
The results show whether the formula can move forward as written, needs a minor adjustment, or requires a different ingredient altogether. That decision is far easier to make before raw materials are purchased and before packaging is ordered.
Where Feasibility Review Fits in Toll Blending
Feasibility review sits between the first conversation about your product and the first production run. It bridges laboratory concepts and multi-ton manufacturing, and it is where the most consequential decisions about a formula are made. For brand owners who outsource production, it is also the stage where expectations about performance, shelf life, and packaging are aligned with what the chemistry can actually deliver.
The process applies to brand-new formulas and to reformulations alike. When a supplier discontinues an ingredient or a price spike forces a substitution, the same screening confirms that the replacement behaves like the original. It is equally valuable for liquid formulations that depend on stable viscosity and for dry mixes that must stay uniform from the blender to the end user.
Common Mixing Hazards the Screening Is Designed to Catch
Some incompatibilities are well documented, and they explain why a documented review comes first. The table below lists examples that blending teams are trained to recognize.
Combination
Potential Result
Why Early Screening Matters
Hypochlorite bleach with ammonia-containing products
Release of irritating chloramine vapors
Cleaning concentrates often contain several reactive ingredients at once
Hypochlorite bleach with acids
Release of chlorine gas
A pH adjustment meant to improve performance can create a hazard
Strong oxidizers with organic solvents
Rapid heat, fire risk, or pressure build-up
Solvent-based degreasers and oxidizing additives should never be paired without testing
Concentrated acids with concentrated bases
Strong exothermic reaction and splashing
Addition order and cooling must be planned before scale-up
Surfactants with incompatible salts or electrolytes
Cloudiness, layering, or loss of viscosity
Visible only after hours or days, so it needs a timed observation window
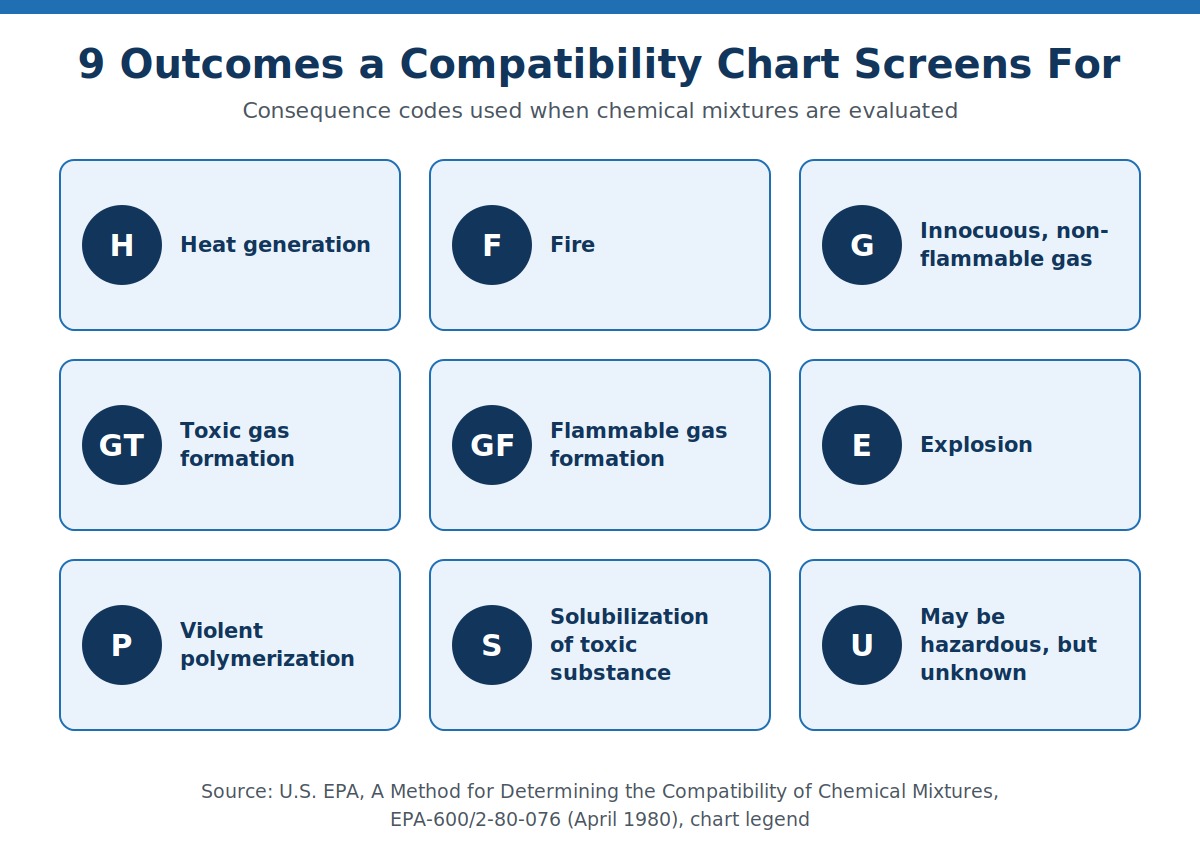
Published reactivity data can flag many of these pairings in advance. A free reactivity prediction tool built for responders and planners shows which hazards, such as heat or gas generation, may arise when two substances meet. It is a useful starting point for a formulation review, though it does not replace hands-on bench evaluation of your actual blend.
Core Parameters Evaluated During Pre-Blend Formulation Screening
A thorough review does not rely on a single measurement. It combines several tests that each reveal a different way a formula can fail. Together they describe how the product will behave during blending, filling, storage, and use.
pH Stability and Drift
pH determines whether a formula stays stable or slowly changes character. A shift can alter cleaning performance, deactivate an active ingredient, or make a mixture more corrosive than intended. In concentrated industrial products, even a small drift can contribute to container damage or an unsafe handling condition. Testing at the start of the study and again after aging establishes a baseline and shows how well the formula buffers itself.
Viscosity and Flow Behavior
Viscosity tells you whether the product pours, pumps, and disperses the way your customers expect. Think of it like concrete slump: too thin and the product migrates or leaks, too thick and it will not move through dispensing equipment. Measuring viscosity at several temperatures confirms that the formula flows properly in a cold warehouse as well as on a warm production floor. This matters especially for surfactant-based cleaners, which can thicken or thin sharply as concentration and temperature change.
Thermal Reactivity and Gas Evolution
Some ingredient combinations release heat, generate gas, or build pressure as they interact. Technicians monitor temperature and watch for bubbling or venting during small-scale mixing, then repeat the test with the intended addition order and rate. This is particularly relevant for car wash concentrates and for solvent-heavy degreasers, where oxidizing and organic components can share the same formula.
Emulsion and Phase Stability
Emulsions combine ingredients that do not naturally stay mixed, so they depend on surfactants and mixing energy to hold together. The failure mode is quiet. A batch can look perfect at the end of blending and then separate into distinct layers on a shelf. Timed observation, centrifuge screening, and temperature cycling reveal weak emulsions early. Teams developing emulsion-based products benefit most from this step.
Freeze-Thaw and Accelerated Aging
Products rarely live at room temperature. They are stored in unheated buildings, loaded onto trucks in summer heat, and delivered in winter. Freeze-thaw cycling and elevated-temperature aging compress months of real-world exposure into a short evaluation window. A formula that separates after one freeze or darkens after a week of heat is far better discovered in a lab than in a customer complaint.
Summary of Core Tests
Test
What It Reveals
Problem It Prevents
pH measurement over time
Chemical stability and buffering strength
Drift that weakens performance or increases corrosivity
Viscosity at multiple temperatures
Flow, pumping, and dispersion behavior
Leaking, clogging, or poor dispensing
Thermal and gas monitoring
Heat release and pressure generation
Exothermic events and pressurized containers
Emulsion and phase observation
Separation, creaming, or precipitation
Non-functional layers on the shelf
Freeze-thaw and heat aging
Resilience across storage and transit conditions
Permanent separation, gelling, or discoloration
Material Compatibility Testing for Packaging and Equipment
A formula can pass every raw material test and still fail because it attacks its own container. Material compatibility testing evaluates how the finished product interacts with drums, totes, bottles, closures, and the equipment used to blend and fill it. A product that degrades its packaging has simply moved the failure to a warehouse, a truck, or a customer facility.
How Chemical Compatibility Testing Protects Containers and Closures
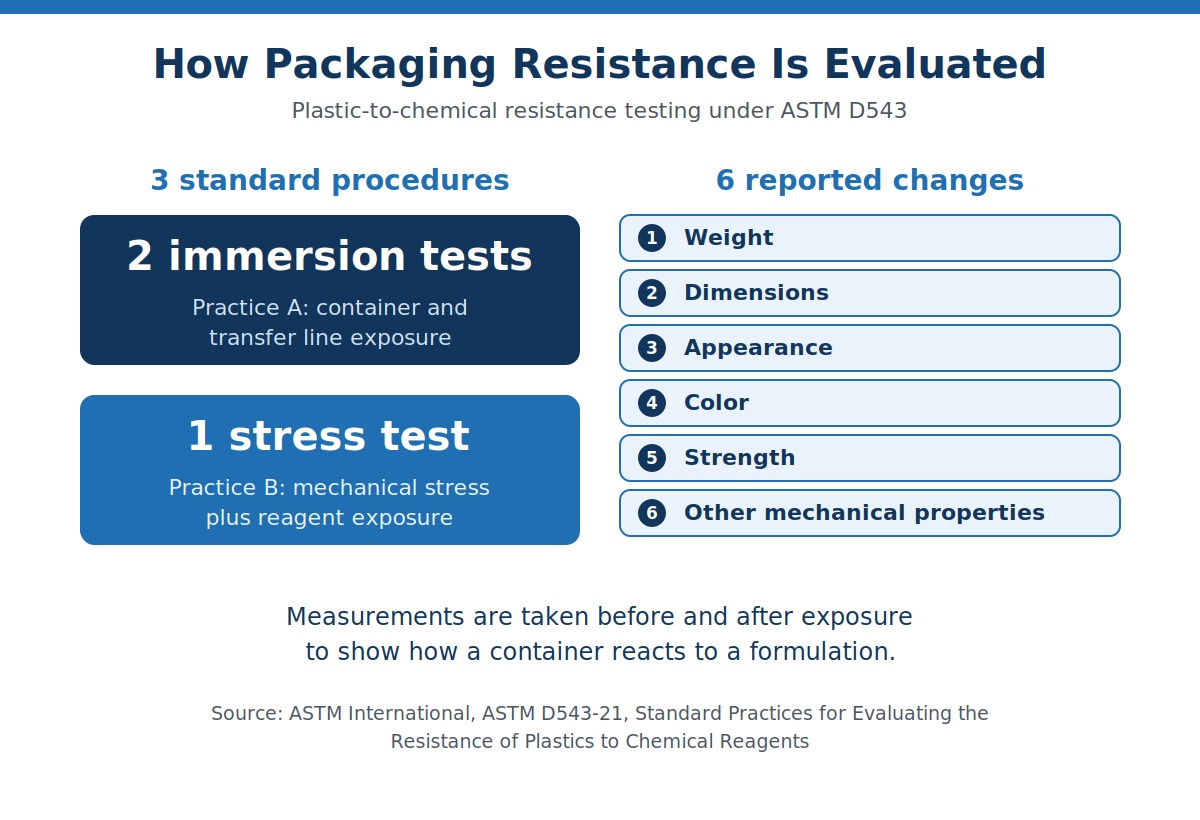
Packaging evaluation exposes sample containers or material coupons to the finished formula under controlled, often elevated, temperatures. The samples are weighed, measured, and inspected before and after exposure. Recognized immersion and stress-cracking practices look for changes in weight, dimensions, appearance, color, and strength, which together show whether a container will hold up through its intended shelf life.
Plastic Drums, Totes, and Bottles
Plastics can soften, swell, craze, or crack when certain solvents, surfactants, or fragrance oils sit against them for weeks. Stress cracking is especially tricky because a container can look fine until it is handled or stacked. Permeation is another concern, since volatile ingredients can migrate through container walls and cause weight loss or odor problems.
Steel Pails and Lined Containers
Acidic and alkaline formulas can corrode bare steel, and chloride-bearing products can attack many metals. Lined containers add protection, but the liner itself must resist the formula. Evaluating both the liner and any exposed seams or fittings prevents leaks that only show up after a long storage period.
Seals, Gaskets, and Closures
Small components cause outsized problems. O-rings, bung gaskets, and cap liners can swell, shrink, or harden in contact with a formula, and a failed seal is a leak waiting to happen. Testing these parts alongside the container confirms the entire closure system works as a unit.
Packaging Component
Typical Concern
What Testing Confirms
Plastic drums and totes
Softening, swelling, stress cracking, permeation
Container keeps its shape, weight, and strength through shelf life
Steel pails and drums
Corrosion from acidic, alkaline, or chloride-bearing formulas
Bare metal or lining resists the formula without pitting
Liners and coatings
Blistering, peeling, or dissolving
Lining stays intact and does not contaminate the product
Gaskets, O-rings, and cap liners
Swelling, shrinking, or hardening
Closure stays leak-resistant after exposure
Once a container is chosen, the next question is how the filled product will be handled. Programs that include hazmat-ready containers need verified material compatibility before labeling and shipping rules can be applied with confidence. Brands running recurring fill schedules can also lock in an approved container through contract fill and pack programs, so every run uses the same tested components.
The Operational Cost of Skipping Pre-Production Screening
The cost of an untested formula shows up in several ways, and most of them are avoidable. A failed batch means lost raw materials, lost labor, and lost production time. A container that fails in storage means damaged inventory and possible cleanup. A product that separates in a customer’s hands means returns, replacement shipments, and a damaged reputation.
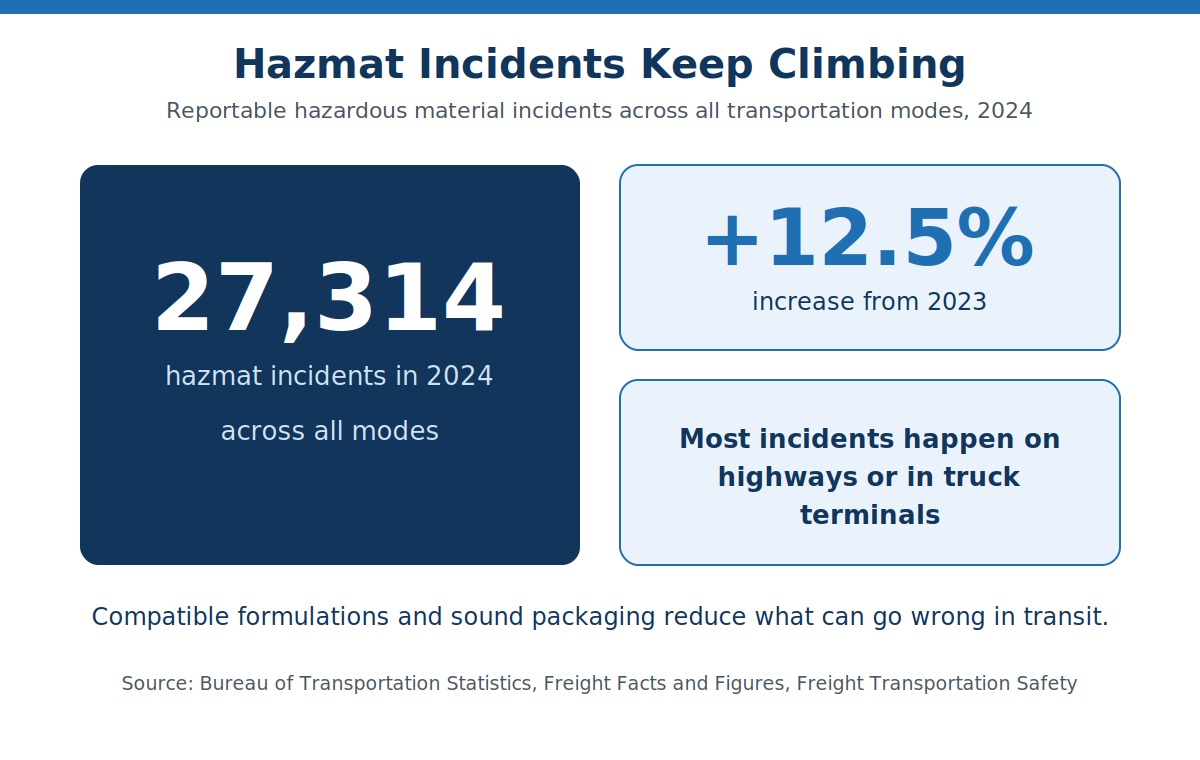
Transportation adds another layer. Hazardous material incidents across all transport modes reached 27,314 in 2024, up 12.5 percent from 2023, and most occur on highways or in truck terminals. A compatible formula in a verified container is far less likely to contribute to that kind of event.
Warehouse and Storage Risks
Storage conditions can quietly undermine a product that was stable on the day it was made. Heat, cold, light, and time all give slow reactions a chance to progress. Reviewing how a finished product will be held matters just as much as reviewing how it will be blended, which is why storage and outbound shipping conditions belong in the early conversation.
Planning for Realistic Timelines
Early testing also makes schedules more reliable. When stability data, packaging approvals, and addition order are settled in advance, production runs move forward without surprise holds. Customers who share their target launch dates up front let the team plan the right number of aging checks and decide which tests can run in parallel.
Reformulation and Ingredient Substitution Strategies
Compatibility work is not only a safeguard. It is also the way to change a formula with confidence. Ingredient shortages, cost pressure, and evolving customer expectations all push brands to adjust what goes into a product, and each change needs the same discipline as the original design.
Validating Substitute Ingredients
Swapping one ingredient for another can change viscosity, foaming, stability, color, and corrosivity all at once. Running the substitute through the same battery of tests as the original shows whether the finished product performs equivalently. Brands building private label product lines often rely on this step to keep multiple formulas consistent when suppliers change.
Reducing Hazard at the Source
Input substitution replaces a more hazardous raw material with a safer one without simply diluting the waste stream. Examples include moving from a harsh solvent to a lower-VOC or bio-based alternative, or replacing an unstable additive with a more robust one. Compatibility screening is what proves the safer option actually works in the finished product. The same logic applies to specialty chemical formulas where performance requirements are tight and small changes can have large effects.
How ITC Approaches Intake-to-Feasibility Review
Industrial Technology Corporation is a family-owned manufacturer with more than 40 years of experience blending and packaging chemical products for customers nationwide. Its intake-to-feasibility process is designed to confirm that a formula can be made safely and consistently before production begins.
Formula intake: Share your ingredient list, concentrations, target specifications, and intended packaging.
Raw material review: Each ingredient is reviewed for compatibility, handling needs, and known hazards.
Bench-scale screening: Small test batches are evaluated for pH, viscosity, thermal behavior, and phase stability.
Packaging evaluation: The formula is checked against the containers and closures planned for production.
Formula adjustment: If a problem appears, the team recommends changes to ingredients, order of addition, or packaging.
Production planning: Approved formulas move into scheduling with documented parameters and realistic timelines.
Because the review covers both formula and container, customers avoid the common problem of solving one issue while creating another. The same team understands the industries ITC supports, so recommendations reflect how products are actually used, stored, and shipped in each market.
Frequently Asked Questions About Chemical Compatibility Testing
What is the difference between chemical compatibility and chemical stability?
Chemical compatibility describes how two or more materials interact when combined, including whether they cause reactions, separation, or damage. Chemical stability describes how a single finished formulation holds its properties over time under conditions such as heat, cold, and light. Compatibility is evaluated first, during feasibility review, and stability testing then continues across the intended shelf life.
How does temperature affect compatibility during storage and shipping?
Extreme temperatures can speed up reactions, weaken emulsions, and cause ingredients to precipitate. Freeze-thaw cycling and heat aging recreate those conditions in a controlled way. A formula that passes at room temperature but separates after a single freeze is not truly stable, so temperature testing is a standard part of a thorough review.
What is a common example of chemical incompatibility in blending?
Mixing hypochlorite bleach with ammonia-containing products releases irritating chloramine vapors, and mixing bleach with acids can release chlorine gas. In industrial blending, strong oxidizers combined with organic solvents, or acids added to bases without controlled cooling, can create dangerous heat, gas, or pressure. Pre-production screening is designed to catch these interactions before they reach a mixing vessel.
How do you know if a formula is compatible with plastic packaging?
Plastic samples such as HDPE or PET are exposed to the formula, often at elevated temperatures, and then inspected for swelling, softening, stress cracking, discoloration, and weight change. This accelerated approach compresses months of storage into a short evaluation window and gives reliable evidence about long-term container performance before any drums are filled at production scale.
Is bench-scale testing enough, or is scale-up testing needed too?
Bench-scale testing identifies most chemistry and packaging problems early, but mixing energy, heat transfer, and addition rates change in larger vessels. A well-run program treats the bench evaluation as the first gate and then confirms performance during the first production-scale batch with in-process checks and finished-product testing.
When should compatibility testing be repeated?
Repeat screening any time an ingredient, supplier, concentration, or container changes. Even a change that seems minor, such as a new grade of surfactant or a different drum liner, can alter how a formula behaves. Treating each change as a mini feasibility review keeps product quality consistent from one production run to the next.
Start Your Formulation Review
If you are preparing to scale a liquid or powder product, confirming compatibility first is the most reliable way to protect your investment. To discuss your formula, your packaging plans, and your timeline, contact the ITC team today. You can also learn more about the company behind the process at Industrial Technology Corporation.
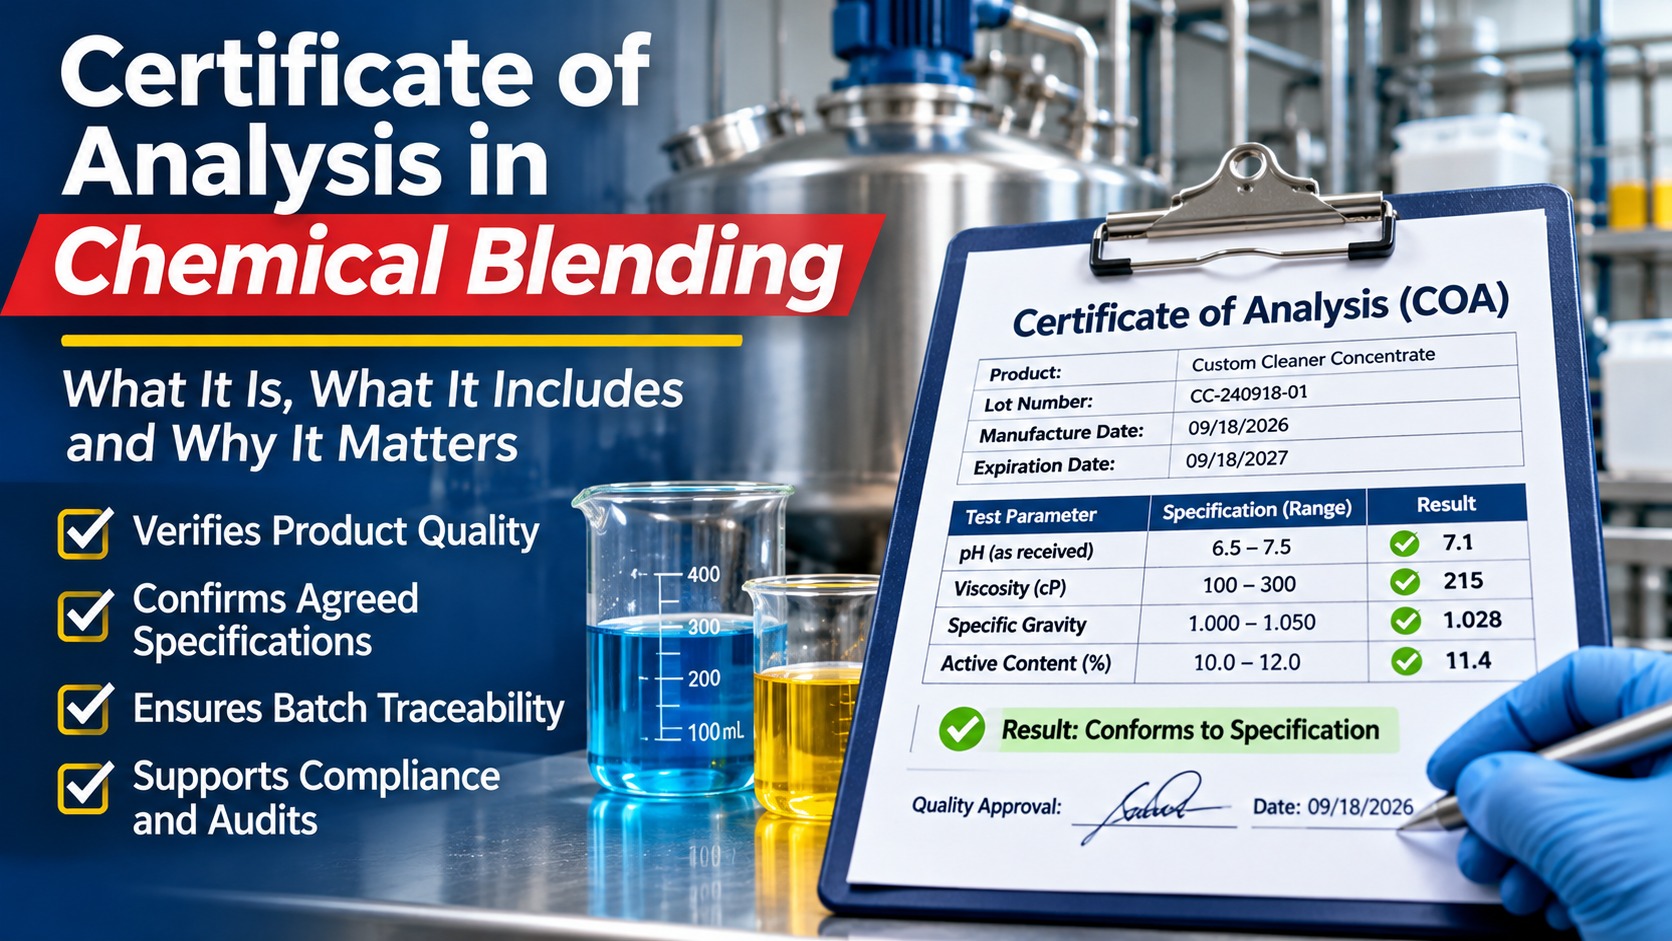
A certificate of analysis in chemical blending is a formal, batch-specific document that verifies a custom chemical mixture meets its agreed specifications based on quality control testing. It is not a product brochure or a generic technical summary. It is measured evidence, tied to one lot number, that the formulation in the container matches what was ordered.
For procurement managers and quality specialists, an off-spec batch has immediate and concrete consequences. A car wash concentrate blended at the wrong pH can strip coatings instead of cleaning them. An industrial degreaser with an active ingredient outside tolerance fails on the line and triggers a root-cause investigation that costs hours and credibility. A commercial cleaner that performs differently from one batch to the next wears down customer trust in a way no discount repairs. The certificate of analysis, usually shortened to COA, is the record that keeps those problems from reaching your floor.
At Industrial Technology Corporation, a COA accompanies every batch of custom liquid and powder formulations we blend, because documentation is part of the manufacturing job and not an administrative afterthought.
How a Certificate of Analysis in Chemical Blending Works
A COA is not interchangeable with a product specification sheet. A specification sheet describes what a formulation is designed to do and the parameters it should meet. A batch COA reports what one specific lot measured during testing, which shows the gap, if any, between a design target and a confirmed result. For teams managing supply chain risk, that difference matters, because a target is an intention and a measurement is a fact.
Chemical mixtures are hard to verify by inspection. Two blends can look identical in the drum and still differ in concentration, pH, or viscosity enough to change how they perform. Batch-level documentation gives your quality team numbers to work from instead of assumptions, and it gives you something concrete to compare against the ranges you agreed on before production began.
What Happens Before a Certificate of Analysis in Chemical Blending Is Issued
The COA is the final step in a quality control sequence that begins before blending starts. Raw materials are verified on receipt, testing equipment is calibrated against certified reference standards, the batch is blended, and samples are tested against the agreed specification ranges. Only then does a qualified person review the results and sign the document. Because the instruments were checked against verified standards first, the measurements on the COA rest on a documented baseline, which is what makes the record defensible when an auditor or a downstream customer asks for proof.
Agreed Specifications Come First
Before production, we work with each customer to define acceptable ranges for the parameters that matter most to their application. Those ranges become the acceptance criteria in the results table of the COA. Testing methods are chosen to suit the formulation, since a thin water-based wash concentrate and a dry powder blend do not need the same protocol.
Key Components of a Chemical Blending COA
The parameters tested vary by product. pH and viscosity matter most for liquid cleaners, while moisture content and bulk density are important for powders. The structure of the document stays consistent, which lets a receiving team verify shipments quickly regardless of which product is on the dock.
Section
What It Contains
Why It Matters
Header and manufacturer information
Blending facility, contact details, and the customer purchase order reference
Ties the document to the right order and supplier
Product and lot identification
Product name, product code, and unique lot number
Must match the container label for traceability
Specifications and test results
Parameters tested, minimum and maximum limits, measured results, and test methods
The core evidence that the batch is on spec
Dates and shelf life
Manufacture date, test date, and expiration or retest date
Confirms stability over the intended service life
Quality approval
Name, title, signature, and date of the reviewer
Creates accountability for the release decision
Why the Signature Matters
A COA without a named, qualified signatory is a data sheet with a logo on it. The signature shows that a qualified person reviewed the results, compared them with the agreed ranges, and judged the batch fit for release. That accountability is what makes the document useful during an audit or a field failure investigation. The lot number deserves the same attention: it should match the label on every container, whether a 5 gallon pail or a bulk tanker, and our packaging and labeling options are set up so the two always agree.
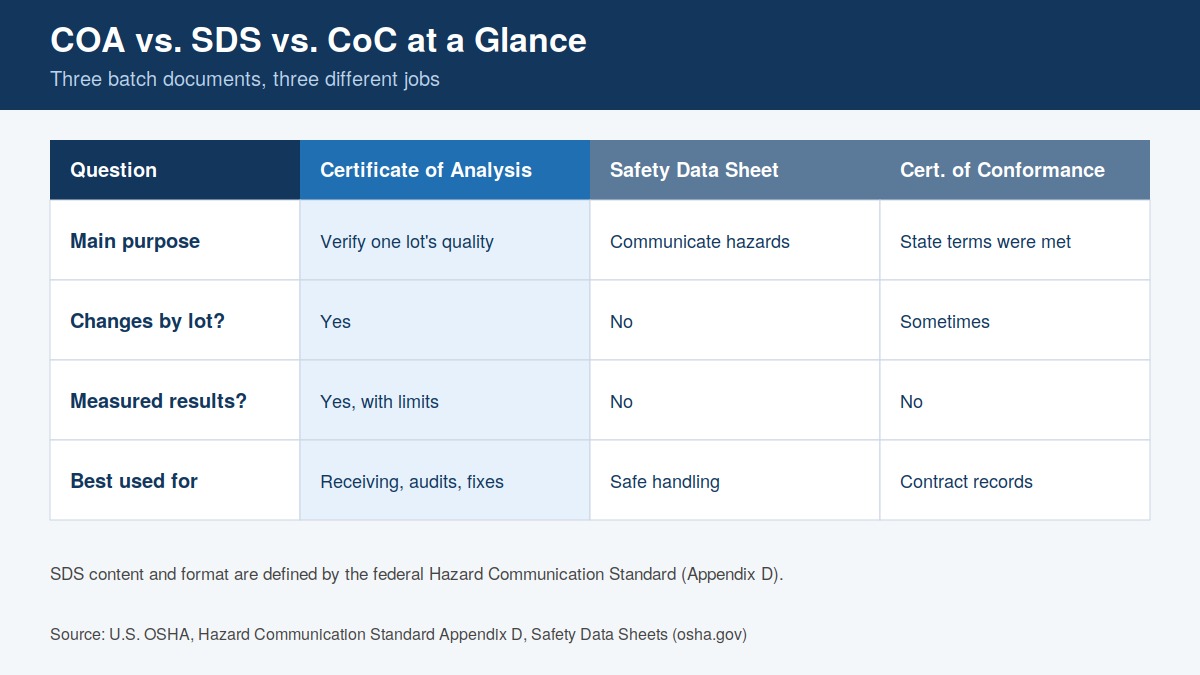
COA vs. SDS vs. CoC: Understanding Batch Documentation
Procurement teams new to toll blending often ask why a COA is needed when they already have the safety data sheet. The two documents answer different questions and cannot stand in for each other.
Safety Data Sheet (SDS)
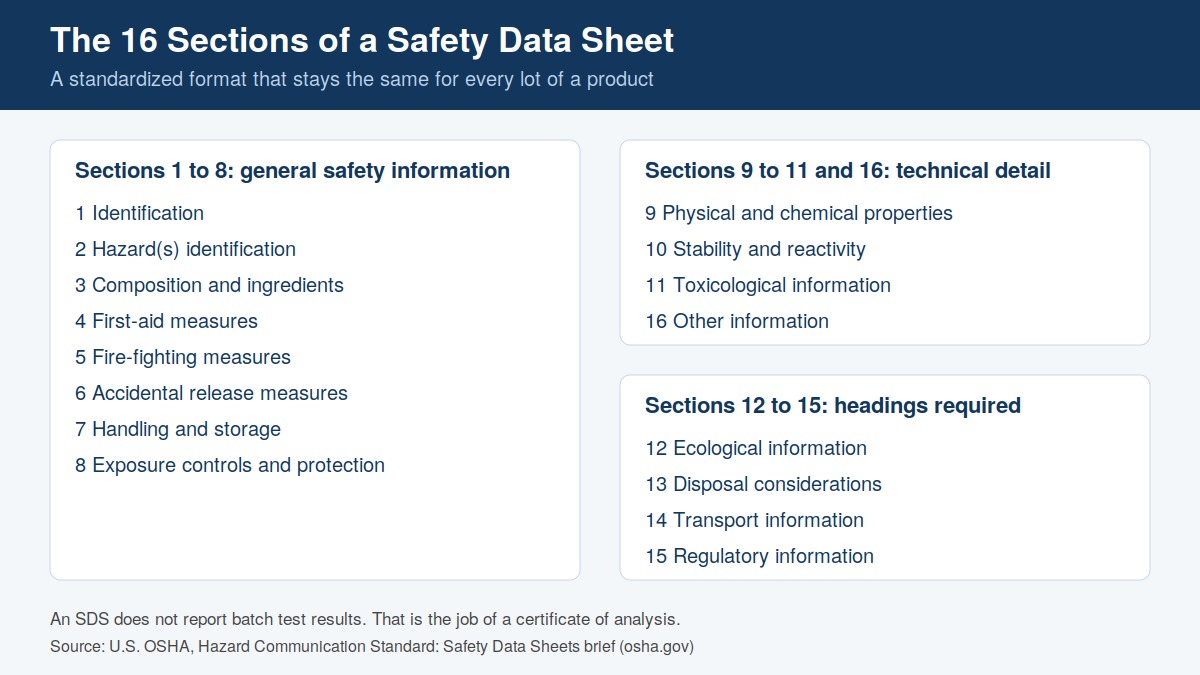
An SDS is a standardized hazard communication document. Under federal rules it follows a 16-section format covering identification, hazards, composition, first aid, handling, exposure controls, and related topics. It describes the product category and does not change from lot to lot. The SDS tells your receiving team how to handle the material safely. It does not tell your quality team whether a particular batch is correct.
A certificate of conformance is a signed statement that a shipment meets contract terms. It usually contains no test data, no measured values, and no analytical verification. That makes it a contractual declaration rather than a quality record. A quality specialist cannot use it to confirm active ingredient concentration, check a dilution ratio, or investigate a failure in the field, because there are no numbers to work with.
An Easy Way to Remember the Difference
Think of an SDS as the owner’s manual for a vehicle model, written for every unit of that model and explaining how to operate it safely. A COA is the inspection report on the specific vehicle you just bought, with the exact readings and tolerances for that unit. The manual is generic to the design, and the inspection report is specific to the one in your driveway.
Document
Main Purpose
Batch-Specific
Contains Measured Results
Certificate of analysis (COA)
Verify quality and specification compliance for one lot
Why a COA Is Critical for Quality Assurance and Compliance
Compliance depends on proof. Facilities that operate under a recognized quality management framework, such as ISO 9001 quality management requirements, document how products are verified, and a COA is one of the records that shows the system working. It gives auditors a paper trail, supports compliance checks on regulated properties such as volatile organic compound content when that parameter is part of the agreed specification, and links a specific production run to the standards it was built to meet.
When a regulatory or customer inquiry arrives, and in industrial chemical manufacturing it eventually does, the COA answers it with measured data rather than memory. It is much easier to respond to a question about a lot shipped months ago when the lot number, test results, dates, and approver are already on a single signed record.
Compliance Support for Specific Product Types
If you formulate products for the transportation sector, such as wash concentrates, wheel brighteners, or surface preparation chemistries, your batch records need to hold up under both customer and regulatory scrutiny. Our automotive chemical blending capabilities pair precise production with complete batch transparency, and our car wash concentrate production follows the same documentation standard. Industrial maintenance products are handled the same way through our degreaser manufacturing.
Operational Benefits of Working With a Blender That Provides a COA
Lower supply chain risk: Off-spec material is caught before it enters your production line, which prevents downtime and avoidable recalls.
Faster receiving inspections: Your team matches the lot number on the container to the COA and verifies results against the agreed ranges, which removes guesswork at the dock.
Evidence-based troubleshooting: If a product behaves unexpectedly in the field, such as a cleaner struggling in hard water, the measured data helps you investigate stability or adjust dilution without starting over.
Audit readiness: Signed, dated, lot-specific records make quality reviews faster and less stressful.
Consistency across batches: Comparing COAs from repeat orders shows whether a product is holding steady over time.
These benefits apply whether the product is a liquid or a dry blend. Our liquid formulation production and dry powder blending each use test parameters suited to the physical form of the product.
What to Look for in a Blending Partner
A blender’s willingness to issue a detailed, signed, batch-specific COA on every run tells you a lot about how it operates when no one is watching. If your current supplier struggles to provide consistent documentation or to hit your specifications, it is reasonable to compare options. Brands selling under their own name have even more at stake, since their reputation rides on every shipment, which is why documentation is built into our private label production. You can also see the range of sectors we support under industries served, and how finished product moves from release to delivery through warehousing and shipping.
How to Read and Use a COA When It Arrives
A COA only protects you if someone checks it. A simple receiving routine takes a few minutes and catches most documentation problems before material is released to production.
Confirm the lot number on the COA matches the label on every container in the shipment.
Check that the product name and code match your purchase order.
Compare each measured result with the minimum and maximum limits listed for that parameter.
Verify that the manufacture date, test date, and expiration or retest date make sense for the product.
Confirm the document is signed and dated by the approving reviewer.
File the COA with the receiving record so it can be found by lot number later.
If Something Does Not Match
If the lot number or any result does not line up, hold the material and contact your blending partner before it is used. A mismatch breaks the chain of traceability, and it is far easier to resolve at the dock than after the product has been dispensed or shipped to your own customers.
Frequently Asked Questions
What is the difference between a COA and a certificate of conformance?
A certificate of conformance is a signed statement that a shipment meets contract terms, and it typically contains no measured data. A certificate of analysis is a batch-specific quality document that lists the actual test results and specification ranges for one lot. If a batch fails in the field, a certificate of conformance gives you nothing to investigate, while a COA gives you the numbers.
Who issues a certificate of analysis in chemical blending?
The chemical manufacturer or toll blender that performed the blending and quality control testing issues the COA. It should be signed and dated by a qualified quality specialist or chemist who verified the results, not by a sales or logistics representative. The signature creates a clear line of accountability from the test data to the person who approved the release.
How long should a company keep certificates of analysis?
Retention periods depend on your quality system, customer contracts, and any rules that apply to your industry or product. Many companies keep COAs at least through the shelf life of the product, and some keep them longer to support audits and complaint investigations. Confirm the requirement with your compliance team and keep each COA filed by lot number so it can be retrieved quickly.
Can a COA be used to verify VOC content for commercial cleaners?
Yes, when volatile organic compound content or a related property such as specific gravity is included in the agreed test parameters. The COA then shows the measured value for that batch, which gives you a record to support compliance reviews. Tell your blender early which regulated properties you need reported so they are added to the specification.
What should I do if the lot number on the container does not match the COA?
Do not use the material. A mismatch means you cannot confirm that the document describes what is in the container. Contact your blending partner right away to obtain the correct batch-specific COA before releasing the product to production.
Do all chemical blenders provide a COA with every batch?
Not necessarily. Some suppliers issue a certificate only on request, or provide a certificate of conformance without test data. Ask any prospective partner whether a signed, lot-specific COA with measured results is included with every run, and review a sample before you commit.
Get Batch Documentation Your Quality Team Can Rely On
A certificate of analysis is the most direct answer to a question every quality manager eventually asks: how do I know what is in this container? It turns a shipment into a verified, traceable, and auditable asset that supports production confidence, compliance, and troubleshooting. Every run we complete ships with a COA that reflects the agreed specifications, the measured results, and the signature of the professional who verified them. To discuss your formulation and the parameters you need documented, reach out to our team or call (563) 322-4882. Our contract blending programs are built to support your quality goals from initial scoping through full-scale production.
If you are comparing contract manufacturers, the chemical toll blending minimum order quantity a partner requires is one of the first numbers that shapes your budget, your inventory plan, and your launch timeline. Procurement teams and product managers are usually asking two questions at once: how much cash do I need to commit up front, and how much room do I have to scale up or down later? The honest answer is that minimums come from physical equipment limits and raw material buying rules far more than from any arbitrary policy meant to protect margin.
Knowing where those limits come from gives you leverage. You can design formulations around standard ingredients, choose packaging that fits the batch, and sequence pilot and commercial runs so you never pay to produce more than you can sell. At Industrial Technology Corporation, we walk customers through this math before the first batch is scheduled, and this guide lays out the same logic in plain terms.
What Determines a Chemical Toll Blending Minimum Order Quantity
A minimum order quantity is the smallest volume of a custom formulation a blender can produce in one run while keeping the batch uniform and covering the real cost of running the equipment. Four forces set that floor: vessel geometry, changeover labor, raw material purchasing, and packaging format. Each one is physical or logistical, which means each one can be planned around once you understand it.
Why Every Chemical Toll Blending Minimum Order Quantity Starts With the Vessel
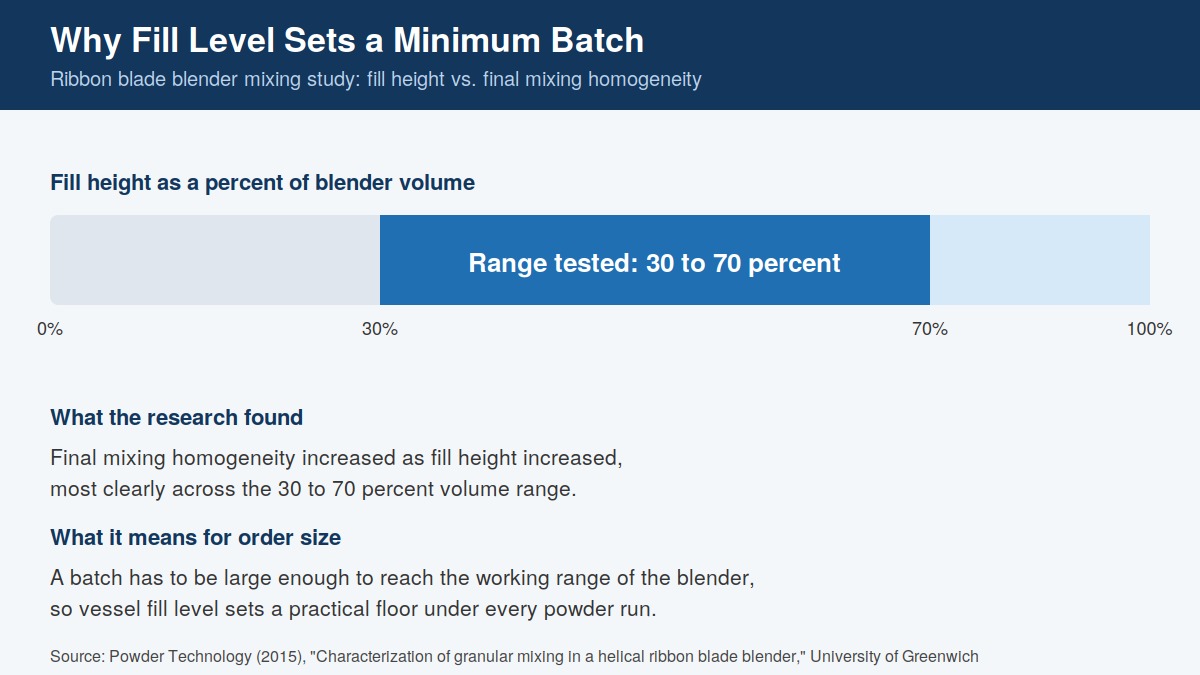
Mixing vessels are engineered to work within a fill range. The liquid level has to cover the impeller so the batch circulates, and in temperature controlled formulations it has to cover enough of the jacketed wall for heating or cooling to work. In dry blending, the powder bed has to reach the agitator so the material is actually lifted and folded. Run below that range and the blender is no longer making a batch at all, it is moving material around without mixing it evenly.
Research on ribbon blade mixers supports this. In one peer-reviewed study of granular mixing in a ribbon blade blender, final mixing homogeneity increased as fill height increased, most clearly across the 30 to 70 percent volume range that was tested. Equipment makers also commonly advise against operating a ribbon blender below roughly 30 to 40 percent of its rated volume, because the agitator cannot generate enough contact with the product.
Clean-Down Time and Changeover Costs
Between formulations, equipment has to be cleaned thoroughly so one customer’s chemistry never carries into the next. Flushing lines, cleaning vessels, and verifying the equipment is ready takes labor and takes the vessel out of production. That cost is fixed whether the run is small or large, so a very small batch carries a heavy changeover burden per gallon or pound. When a blender prices a short run, a meaningful share of the price is the cleaning, not the blending. Customers who run the same formulation repeatedly, or who group similar products together, spread that cost across more volume.
Raw Material Purchase Minimums
Suppliers sell ingredients in drums, totes, bags, and pallets. If your formula calls for a small amount of a specialty surfactant, solvent, or additive, the blender may still need to buy a full container to fulfill the run. That purchase minimum becomes a floor under the blender’s own minimum, and it can quietly raise the effective MOQ of every run that uses the ingredient.
Consolidate formulations so several products share the same specialty inputs.
Share your annual forecast so the blender can buy ahead and spread the purchase across scheduled runs.
Summary of the Main MOQ Drivers
Driver
What It Controls
How You Can Plan Around It
Vessel size and fill range
Smallest batch that mixes uniformly
Match batch volume to a vessel that fits it
Clean-down and changeover
Fixed labor cost per run
Group similar products and use repeat scheduling
Raw material pack sizes
Minimum ingredient purchase
Standardize inputs and share annual forecasts
Packaging format
Filling cycles and leftover product
Align batch size with whole container counts
Viscosity and chemistry
Pump, motor, and vessel compatibility
Confirm equipment fit early in development
Liquid vs. Powder Batch Size Minimums
Liquid and dry blending are different operations, so their minimums are calculated differently. A blender with a fleet of mid-size tanks will set a different floor than one running large powder vessels, and neither will match a generic number you read in an industry overview. The only reliable way to learn a real minimum is to describe your product and let the blender match it to the right equipment.
Liquid Tank Constraints
Liquid production is organized around tank capacity, pump flow rates, and temperature control. The tank has to hold enough liquid to submerge the impeller and keep the batch stable, and viscosity changes everything. A thick industrial degreaser needs different pumps and mixing energy than a thin, water based wash concentrate, so a blender running both will not apply the same minimum to each. Customers developing car wash concentrates or industrial degreasers should raise viscosity and foaming behavior early, because both affect which tank and pump the batch needs. For a closer look at tank based production, see our liquid formulation capabilities.
Powder Blender Fill Levels
Dry blending relies on ribbon blenders or plow mixers, where the physical volume of the vessel sets a hard lower boundary. You need enough material to generate the shear and folding action that produces a homogeneous blend, and there is no workaround for a blender running at a small fraction of its rating. The practical result is that powder minimums are often tied to the usable working volume of the blender, which is lower than the total shell volume. Our ribbon blender powder production is organized around exactly this constraint.
Packaging is one of the most overlooked drivers of the minimum you will actually be quoted. Smaller containers such as 5 gallon pails take more filling cycles, more labor, and more handling per unit of product than drums, totes, or bulk tankers. That operating cost shows up in the minimum run a blender will accept for a given container. If you are still deciding between formats, our packaging configurations from pails to bulk can be matched to your expected volume.
Heel and Yield Loss
Batch volume should also line up with the container count. Any product left behind in the vessel after filling, known as heel, is lost yield and adds to clean-down work before the next run. A batch sized to fill a whole number of drums or totes wastes less than one that leaves a partial container and a residue in the tank.
Regulated Products and Hazmat Handling
Formulations that ship as regulated materials need compliant containers, labels, and documentation, and that can influence which pack sizes make sense. Planning for hazmat ready packaging at the start avoids a late change to container size that would force a different batch volume.
Pilot, Small Batch, and Commercial Run Types
Most product launches move through three stages, and each stage has a different goal. Choosing a partner who can support all three prevents the handoff problems that appear when development happens in one facility and production in another.
Run Type
Purpose
Planning Notes
Pilot batch
Validate chemistry, stability, and packaging compatibility
Smallest commitment; confirm the formula before any market commitment
Small batch run
Regional market tests and niche industrial applications
Limits inventory risk and protects cash flow
High volume run
National distribution and repeat supply
Per unit cost improves and scheduling becomes predictable
Running a full commercial volume on an unproven formula is a cash flow risk most businesses cannot justify, which is why a pilot stage is worth building into the plan. Brands that sell under their own label often start with a pilot and then expand, and our team supports that path for private label product lines from the first sample through repeat production.
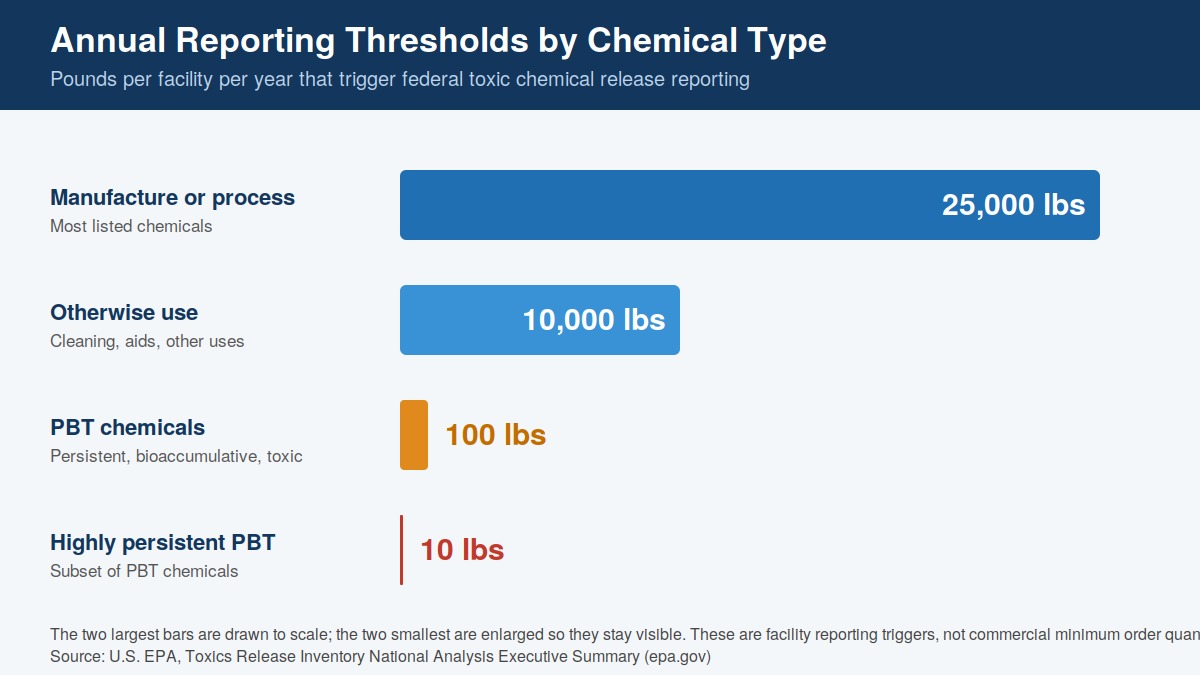
Federal Reporting Thresholds Are Not the Same as Order Minimums
Buyers sometimes confuse a blender’s commercial minimum with the annual quantity thresholds that trigger federal toxic chemical release reporting. They are separate. The reporting thresholds apply to a facility’s yearly totals, not to your order, but they influence how a blending partner schedules, tracks, and documents runs that involve listed chemicals. Under the national program, the standard annual threshold is 25,000 pounds for manufacturing or processing a listed chemical and 10,000 pounds for other use. Chemicals that persist and accumulate in the environment face far lower triggers, down to 100 pounds and 10 pounds.
If your formulation includes regulated solvents or other listed ingredients, raise them in your first conversation so reporting, documentation, and volume planning are handled together from day one.
How to Negotiate and Scale Order Quantities
Minimums are rarely fixed in stone. The variables behind them, including equipment scheduling, raw material purchasing, and clean-down time, respond to good planning. Buyers who arrive with a clear picture of annual volume, formulation complexity, and packaging requirements regularly get better terms than those who open with a single run and no forward view. Our full scope contract blending programs are built to flex around that kind of forward planning.
Commit to Annual Volume With Scheduled Releases
An annual volume agreement with scheduled release dates gives the blender predictable scheduling and lets them buy raw materials in larger, cheaper quantities. That predictability reduces the per run overhead they need to recover, which is often the lever that makes a lower minimum possible.
Standardize Ingredients and Share the Forecast
Formulas built around readily available inputs avoid the purchase minimums that inflate small runs. Sharing a realistic twelve month forecast, even a rough one, helps the blender plan purchasing and schedule equipment time around your demand curve.
Use One Partner From Development Through Commercial Production
Keeping pilot and commercial work with the same blender removes the technical transfer that often causes formulation drift. It also builds a shared record of what the formula needs at each scale.
Scaling From Pilot Batch to Full Production
Moving from a pilot to a commercial batch is where many quality problems begin. Viscosity behavior, mixing time, and ingredient feed rates all shift as batch size grows, and those shifts are not always linear or predictable from bench scale data. Each increase in scale should be checked against the pilot sample, with adjustments documented so the commercial batch matches what you approved.
What to Verify at Each Scale Increment
Viscosity and appearance compared with the approved pilot sample
Mixing time and agitation settings for the larger vessel
Ingredient addition order and feed rates
Packaging compatibility and fill accuracy at the new container size
Stability results before the first full commercial release
Once a product is running at volume, outbound logistics matter as much as the blend itself. Our warehousing and outbound freight support lets finished product be stored and released against your demand instead of all at once. We serve customers across many sectors, and you can see the full range of industries we support when you are mapping your product to the right production approach.
Frequently Asked Questions
What is MOQ in chemical manufacturing?
MOQ stands for minimum order quantity. In contract chemical manufacturing it is the lowest volume a blender can produce in one run while covering operating costs and keeping the batch consistent. The floor is set by physical equipment limits such as vessel size and impeller geometry, and by operating costs such as clean-down labor and setup time. Batch consistency is the firm constraint, because a run that is too small for the vessel can produce material that does not meet specification.
What are typical minimums for chemical toll blenders?
Minimums vary with whether the product is a liquid or a dry powder, the blender’s equipment, the packaging format, and raw material sourcing. Some large blenders require truckload volumes before they schedule a run, while more flexible partners can accommodate smaller batches for development or niche applications. Because a real number depends on your formulation, the best way to learn it is to describe the product and request a custom quote.
How does scaling from pilot batch to full production work?
The process starts with a small pilot batch to validate chemistry, stability, and packaging. After the pilot meets specification, the formula moves to a larger vessel with mixing time, ingredient feed rates, and temperature adjusted for the new scale. Using the same blender for both stages reduces the risk of formulation drift during technical transfer.
Are there flexible toll manufacturing options for small batches?
Yes. Some toll blenders support small batch work for new product launches, regional tests, and niche applications where volume is naturally limited. Small runs help manage cash flow and inventory risk during validation, and packaging can scale from pails to bulk as demand grows.
How does capacity planning affect a chemical toll blending minimum order quantity?
Capacity planning schedules equipment, labor, and raw materials across a mix of large runs and small custom batches. A facility running near capacity may need larger minimums to justify a schedule change, while one with open time can be more flexible. Sharing an annual forecast helps the blender plan ahead and often supports smaller or more frequent runs.
Why do powder and liquid products have different minimums?
Liquid blending is limited by tank volume, impeller coverage, pumps, and temperature control, while powder blending is limited by the working volume of ribbon blenders or plow mixers. Viscosity matters on the liquid side, and particle size and bulk density matter on the powder side, so the same batch volume does not suit both.
Plan Your Next Blending Run
Understanding a blender’s minimums turns a procurement detail into a supply chain planning tool. The businesses that handle it well enter the conversation knowing their annual volume, formulation complexity, and packaging needs, which shortens onboarding and reduces cost surprises. Tell us about your product and we will recommend a batch size, packaging format, and scale up path that fits it. You can request a custom blending quote online or call (563) 322-4882 to talk through your formulation.
Regional distributors, private-label brands, commercial cleaning suppliers, facility maintenance companies, and industrial manufacturers that hit supply chain ceilings or formulation limits all need a dedicated industrial cleaning chemical manufacturer. The real question is not whether outsourcing makes sense at scale. It is whether the drag of in-house mixing or fragmented sourcing is already costing more than a transition would.
Mixing in-house pulls capital, labor, and attention away from selling. A specialized blending partner such as Industrial Technology Corporation extends a brand’s operational reach without requiring it to build tanks, ventilation, and safety infrastructure of its own.
Industrial manufacturers: Whose cleaning requirements are too specialized for off-the-shelf chemistry.
Operational bottlenecks are usually the first concrete signal. When a distributor’s lead times stretch because one raw material is back-ordered, or a private-label brand cannot scale a SKU because its supplier has hit a capacity ceiling, the case for a dedicated manufacturer stops being theoretical.
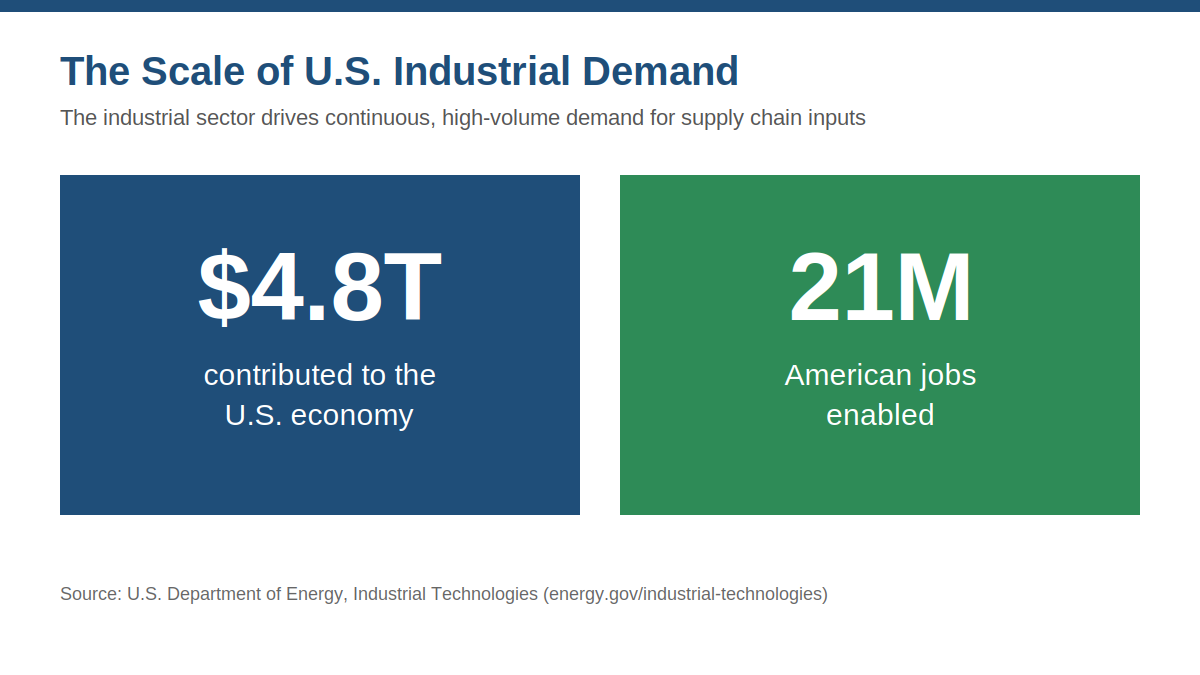
The underlying demand is enormous. The U.S. Department of Energy reports that the industrial sector contributes $4.8 trillion to the economy and enables 21 million jobs, which generates steady, high-volume demand for chemical supply chains that can keep pace with production schedules.
Signs an Industrial Cleaning Chemical Manufacturer Is the Next Step
Supply chain stability at that level takes more than a vendor relationship. It takes a manufacturer with deep raw material sourcing, quality systems that catch batch variation before product ships, and the logistics to fill orders across multiple packaging configurations. Warning signs that a business has outgrown its current setup include:
Back-orders on a single raw material that stall finished product.
A supplier that cannot add capacity for a growing SKU.
Inconsistent batches that trigger customer complaints or returns.
Staff time going to mixing, labeling, and paperwork instead of sales.
Cleaning problems that catalog products cannot solve.
For businesses that have outgrown a local chemical supplier, industrial cleaning chemical blending at a dedicated facility closes the gap between what a brand can sell and what it can reliably produce.
Compliance pressure compounds the sourcing problem. Growing businesses face an expanding set of rules covering chemical labeling, Safety Data Sheets, and VOC limits. Managing those requirements internally demands dedicated staff, ongoing monitoring, and documentation systems that most distributors and private-label brands are not built to maintain. A professional partner absorbs that burden as part of the production relationship, not as a separate line item.
Efficiency matters too. A manufacturer with strong inbound sourcing and outbound logistics gives customers more predictable pricing and delivery windows, which is valuable when inventory is spread across several distribution points.
Products an Industrial Cleaning Chemical Manufacturer Can Produce
A professional blending partner makes liquid and powder formulations across many categories, including car wash concentrates, fleet cleaning solutions, heavy-duty degreasers, floor care products, and specialty blends for particular industrial soils. Unlike a catalog supplier with fixed SKUs and fixed performance, a manufacturer works from your specifications or develops formulations with you.
Customization lets brands compete on performance instead of price. A distributor serving food processors needs a different alkaline cleaner than one serving metal fabrication shops, even if the two look similar on a spec sheet. Configuring surfactant packages, alkaline builder concentrations, and solvent ratios to match specific surfaces and soils is what separates a manufacturing partner from a reseller. It also lets a brand expand its line without in-house R&D or lab staff.
Product Category
Typical Use
Formulation Focus
Heavy-duty alkaline degreasers
Manufacturing equipment and production line maintenance
Solvent blend and surfactant balance for baked-on grease
Acidic cleaners and brighteners
Scale removal, rust inhibition, and aluminum brightening on fleet vehicles
pH control that cleans without etching metal
Neutral-pH floor finishes and strippers
High-traffic commercial facilities
Leveling, durability, and removability
Vehicle wash detergents
Touchless and brush-style commercial car washes
Foam, dwell time, and rinse performance
Adjusting surfactant ratios in any of these categories decides whether a product sheets off a surface quickly or clings long enough to penetrate baked-on grease and road film. End users notice that difference immediately, yet it takes precise formulation control to deliver it consistently. A capable surfactant blending process is where that control starts.
Industrial Technology Corporation has operated as a family-owned contract manufacturer for more than 40 years. For brands weighing outsourced production, the model is straightforward: chemical blending services run from formula intake to finished goods, eliminating the capital cost of blending tanks, ventilation systems, and specialized safety equipment while letting volume scale up or down with demand.
Industrial Cleaning Chemical Manufacturer Support for Degreasers and Detergents
Degreasers are among the most technically demanding products a manufacturer handles, and the challenge goes beyond mixing surfactants with alkaline builders. Cutting through heavy hydrocarbons, road tar, and soot without damaging aluminum, painted surfaces, or rubber seals calls for careful solvent selection, pH management, and chelating agents that keep soils suspended instead of redepositing on the surface. Experienced degreaser contract blending covers the full path from initial specification through batch production and quality verification.
Concentrate design is one of the most practical decisions in this category. A product engineered to work at a leaner dilution reduces cost per use for the end user and cuts shipping weight, which improves freight economics for the distributor. Getting there takes surfactant chemistry expertise and iterative testing, not just a formula tweak.
Fleet Wash and Commercial Detergent Formulations
Fleet cleaning adds another layer of complexity. Concentrates must brighten oxidized aluminum wheels and lift road film without etching metal or leaving residue that speeds corrosion, and the formulation window is narrower than it looks. Commercial detergent applications for fleet maintenance typically require:
High-pH alkaline detergents: For heavy road grime and organic soils on vehicle exteriors.
Low-pH acidic brighteners: For oxidized aluminum and brake dust removal.
Surfactant-rich foaming agents: Engineered for touchless systems where dwell time and foam coverage do the mechanical work.
Brands serving wash operators can go deeper with dedicated car wash chemical blending, tuned to the equipment and water conditions their customers run.
Concentrated Cleaners, Floor Care Products, and Specialty Blends
Shipping water is a waste that concentrates eliminate. The table below shows how much ready-to-use solution a single 5-gallon pail can produce at common dilution ratios.
Dilution Ratio (concentrate to water)
Approximate Ready-to-Use Volume from 5 Gallons
1:20
100 gallons
1:64
320 gallons
1:128
640 gallons
A pail designed for 1:128 dilution delivers the cleaning capacity of roughly 640 gallons of ready-to-use product at a fraction of the freight cost and storage space. Distributors gain a real freight advantage, and facility operators manage inventory more precisely because less product covers more area. Concentrates are a natural fit for liquid blending, and dry concentrates can be developed through powder blending when a dissolvable format suits the application.
Viscosity is a detail that deserves more credit than it gets. A floor finish that is too thin will not level, leaving streaks and uneven sheen. A degreaser that is too thick will not move through automated dispensing equipment. A manufacturer sets these parameters to match the customer’s application method, whether hand mop, auto scrubber, pressure washer, or foam applicator, so the product performs in the field and not only in the lab.
Floor finishes, sealers, and strippers for commercial facilities are a specialty category where precision directly affects durability under heavy foot traffic. A finish that fails early in a distribution warehouse or retail space creates maintenance cost and liability that far exceed the cost of getting the chemistry right. These blends are developed through collaborative consultation, where the technical team works against the customer’s performance targets, surface type, and application conditions instead of pulling a standard formula off a shelf.
Brands that already have a formula and need professional filling, labeling, and logistics rather than development can lean on contract chemical packaging, which covers the full production-to-shipment cycle from 5-gallon pails to 275-gallon totes.
Packaging, Labeling, and Shipping for Commercial Cleaning Products
Chemical labeling and Safety Data Sheet management carry stringent federal requirements that most brands underestimate until they face a compliance gap. Safety Data Sheets follow a uniform 16-section format aligned with the Globally Harmonized System of Classification and Labeling of Chemicals, and they must be revised within three months of a manufacturer becoming aware of significant new information about a chemical’s hazards. A professional manufacturer handles those updates as part of the production relationship, protecting brands from the violations and liability that come with outdated or incomplete hazard documentation.
Turnkey packaging and shipping logistics cover the full lifecycle, from container selection through staged outbound freight:
Custom labeling and private-label branding applied to finished containers.
Packaging in 5-gallon pails, 55-gallon drums, and 275-gallon totes to match distributor and end-user requirements.
Staging and preparation for outbound freight to distribution points.
How to Evaluate an Industrial Cleaning Chemical Manufacturer
When comparing potential suppliers, the criteria that matter most are technical capability, compliance infrastructure, and batch-to-batch consistency. A reliable partner will:
Communicate clearly throughout the production cycle.
Maintain raw material traceability from sourcing through finished goods.
Document quality control results so customers see what they are receiving, not just an invoice and a pallet.
Manage hazardous goods handling, which is where hazmat chemical packaging expertise becomes essential for corrosive and regulated products.
Managing packaging, labeling, and compliance in-house is a heavy burden that grows with every product added. Outsourcing lets growing brands redirect internal resources toward sales, marketing, and customer development instead of production management.
Why Outsourced Blending Works for Cleaning Chemical Brands
Capital preservation is the most immediate financial argument. Building or upgrading a blending facility means investing in mixing vessels, ventilation and exhaust, chemical storage, spill containment, and specialized safety equipment. Once committed to production infrastructure, that capital is no longer available for inventory, sales headcount, or market expansion.
Production scalability is the operational argument. An outsourced model lets brands raise or lower volumes based on real demand without carrying the fixed overhead of a facility sized for peak capacity. A private-label brand entering a new market can scale a SKU without pre-committing to a run larger than its initial distribution footprint. Brands that operate their own blending lines cannot match that flexibility, because their overhead only drops with volume, not with demand.
Ingredient safety is a third. Responsible manufacturers evaluate raw material safety and environmental impact against verified scientific data before a custom formulation reaches production, which matters for customers who must demonstrate responsible sourcing in their own supply chains.
Intellectual property protection is a reasonable concern in any toll blending conversation. Professional toll blenders protect client formulas through non-disclosure agreements and dedicated batch records that keep proprietary chemistry confidential. A true manufacturing partner acts as an extension of the client’s team, handling production, compliance, and logistics without competing in the client’s market or sharing formulation data with other customers.
Brands that want a single partner for both development and production can start with toll chemical blending and packaging, and those building their own product lines can explore private label chemical blending to bring differentiated products to market under their own name.
Frequently Asked Questions About Industrial Cleaning Chemical Manufacturers
What is the difference between toll blending and custom chemical formulation?
Toll blending manufactures a product from the customer’s exact, existing formula and specifications. The manufacturer provides capacity, equipment, and labor, and the customer keeps ownership of the formula. Custom chemical formulation is a collaborative process in which the manufacturer’s technical team develops or modifies a formula to meet specific performance requirements. Both services are available from Industrial Technology Corporation.
How do industrial chemical manufacturers ensure VOC compliance?
Manufacturers monitor volatile organic compound (VOC) regulations and adjust surfactant and solvent ratios to stay compliant without sacrificing cleaning performance. Because limits vary by application category and jurisdiction, a competent manufacturer tracks regulatory changes and updates formulations in advance instead of reacting after the fact.
What are the typical minimum order quantities (MOQs) for custom blending?
MOQs depend on whether the product is a liquid or powder and on the packaging configuration, since pails, drums, and totes each have different production economics. They are structured to optimize production efficiency and raw material sourcing, and they are usually discussed during the initial formulation consultation so customers can plan inventory and cash flow.
Can an industrial manufacturer help with private-label packaging and design?
Yes. Turnkey manufacturers provide private-label services that include container selection, custom label application, and compliance reviews so the finished product is retail- or commercial-ready under the customer’s brand. That covers GHS-compliant labeling, Safety Data Sheet documentation, and packaging that meets distributor and end-user requirements.
How are Safety Data Sheets (SDS) managed for custom formulations?
The manufacturer develops and updates each SDS in line with federal hazard communication requirements and GHS guidelines so all hazard information is accurate and current. Sheets must be revised within three months of significant new hazard information, a timeline a professional manufacturer tracks as part of its ongoing compliance work.
What types of businesses benefit most from outsourced cleaning chemical production?
Distributors, private-label brands, commercial cleaning suppliers, facility maintenance companies, and industrial manufacturers benefit most, especially when they face capacity limits, inconsistent supply, or formulation needs that catalog products cannot meet.
Reach Out to Us Today
Brands that outsource blending and packaging to a capable manufacturer gain more than capacity. They free internal resources for the work that drives growth: customer acquisition, distribution development, and product line strategy. Formulation, compliance, and logistics are handled by a partner with the equipment, expertise, and regulatory systems to manage them at scale.
Whether you need custom blending, private-label manufacturing, or contract packaging, our family-owned team is ready to talk through your goals and find the production model that fits your brand today and as it grows.
Agricultural chemical manufacturing is the operational backbone of modern food production, and its scope runs far wider than most product managers and distributors assume. The common association with pesticide synthesis misses much of what the industry makes: primary crop nutrients, soil conditioners, post-harvest treatments, livestock facility sanitizers, and heavy-duty equipment maintenance chemicals. Each category carries its own formulation requirements, regulatory obligations, and supply chain demands.
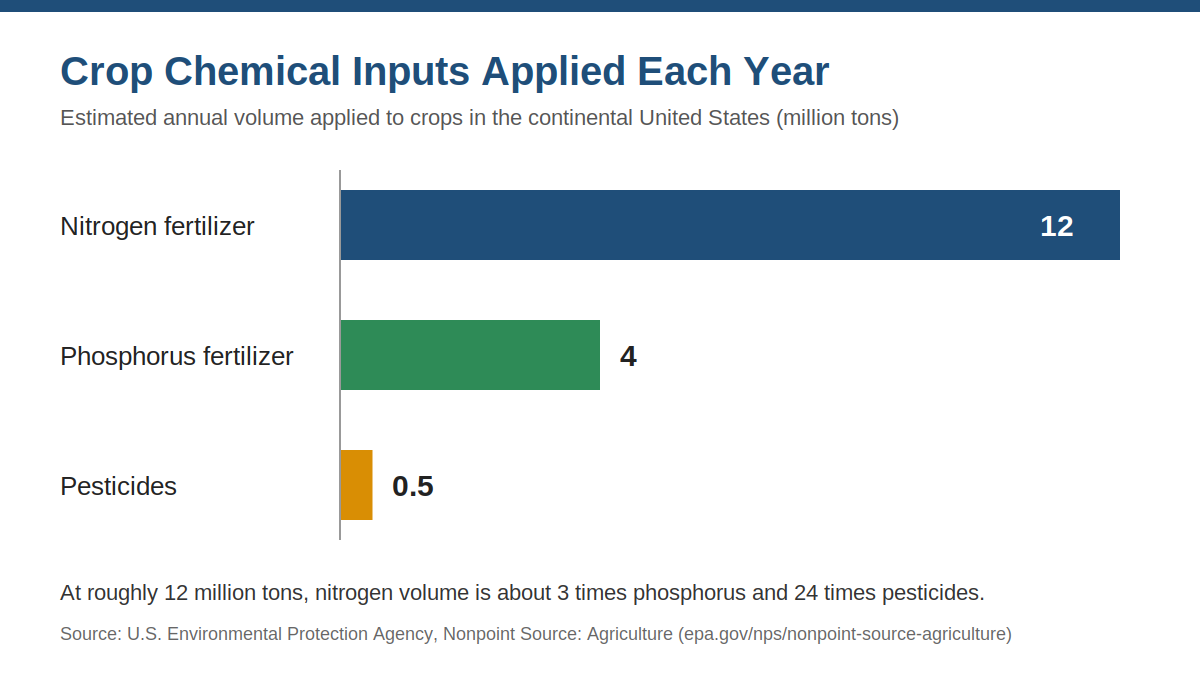
The scale of the work explains why it takes serious manufacturing infrastructure. According to the U.S. Environmental Protection Agency, roughly half a million tons of pesticides, 12 million tons of nitrogen, and 4 million tons of phosphorus fertilizer are applied to crops in the continental United States every year. Moving those volumes reliably requires precise formulation chemistry, dependable blending systems, and packaging operations built to handle hazardous materials at production scale.
That is where a specialized chemical blending and packaging partner like Industrial Technology Corporation becomes part of the picture, turning proprietary formulas into consistent, compliant, ready-to-ship products.
What Does Agricultural Chemical Manufacturing Produce?
The category is broader than field sprays and fertilizer bags. The table below shows the major product groups and why formulation precision matters in each one.
Product Group
Common Examples
Formulation Priority
Crop nutrients
Nitrogen, phosphate, potash, and sulfur blends
Stable concentration and compatibility with application equipment
Crop protection support
Surfactants, adjuvants, and carrier systems
Emulsion stability and consistent dilution
Facility sanitation
Sanitizers and disinfectants for dairies, egg processing, and livestock housing
Pathogen kill efficacy at calibrated active ingredient levels
Equipment maintenance
Degreasers, road tar removers, and aluminum brighteners
Cleaning power without damaging paint, anodized finishes, or fittings
Post-harvest treatments
Storage and commodity quality products
Residue control and handling safety
Agricultural Chemical Manufacturing for Crop Nutrition
Corn and soybean programs lean on the primary macronutrients nitrogen (N), phosphate (P₂O₅), and potash (K₂O), along with secondary nutrients like sulfur (S). The challenge is getting those nutrients into stable forms that perform the same way across different soil types, water sources, and spray or fertigation equipment.
Liquid formulations are especially demanding. Concentrations must stay accurate from the first gallon to the last, and the product has to remain pumpable and stable through a long application season. Experienced liquid blending is what keeps a nutrient concentrate within its stated analysis, batch after batch.
Dry nutrient and micronutrient products bring different concerns, including particle size, flowability, and uniform distribution of small-percentage ingredients. A reliable powder blending process prevents the segregation that leaves one bag rich in an ingredient and the next bag short.
Agricultural Chemical Manufacturing for Cleaning and Maintenance Products
Facility sanitation and equipment maintenance are a large and often underserved part of the agricultural supply chain. Egg processing plants, dairies, grain handling facilities, and livestock operations all work under strict sanitation expectations, and those expectations leave no room for improvised cleaning protocols or consumer-grade products.
Sanitizers and Disinfectants for Livestock and Processing Facilities
Contamination risks in these environments are real, and the cost of a sanitation failure reaches well beyond a failed inspection. Purpose-built industrial cleaning chemical blending accounts for active ingredient concentrations, surfactant selection, and compatibility with the surfaces and drainage systems found in agricultural settings. A cleaner that works well on stainless steel tanks may attack aluminum fittings or leave residues that interfere with food-contact surfaces, so formulation specificity matters.
Heavy-Duty Degreasers and Surface Treatments for Farm Equipment
Tractors, harvesters, and transport vehicles collect road tar, soot, hydraulic fluid, and baked-on grime. Effective degreaser contract blending produces products that cut through that buildup without stripping protective coatings.
Common facility and equipment applications include:
Facility sanitizers and disinfectants: Formulated for egg processing, dairies, and livestock housing, with concentrations calibrated for pathogen kill in those specific environments.
Equipment degreasers: Engineered to remove road tar, soot, and hydraulic fluid from tractors, harvesters, and trucks without damaging painted or anodized surfaces.
Post-harvest and livestock treatments: Specialized products that help maintain commodity quality in storage and support sanitation in livestock facilities.
Aluminum brighteners: Acid-based or chelated chemistry for trailers, RV rooftops, and equipment panels where oxidation and staining build up.
Brands that want to grow their cleaning and sanitation lines without building a plant of their own can do so through private label chemical blending, bringing consistently formulated products to market under their own name.
How Agricultural Chemical Blending Supports Farm and Facility Products
The gap between a stable bench formulation and a production-ready product is where many agricultural brands first run into operational friction. Blending is not just combining ingredients in the right ratios. It means managing pH stability across temperature ranges, keeping surfactant systems intact under the shear of high-volume mixing equipment, and confirming that active ingredients stay available instead of binding to carrier compounds.
Scaling From Bench Batches to Production Runs
Moving from a 5-gallon development batch to a 5,000-gallon production run introduces variables that bench chemistry does not predict well: heat generated during mixing, emulsifier behavior under extended agitation, and the settling characteristics of suspension concentrates in large containers. These are the root cause of products that worked in trials but perform inconsistently in the field.
Think of custom toll blending like a recipe that has to taste the same whether it is cooked for four people or four hundred. Adjusting ratios for surfactant blending and emulsion blending at scale is a skill, and a partner with production-scale experience brings it to the formulation process from the start, which means fewer surprises between development and commercial launch.
Blending and Packaging Support for Seasonal Demand
Agricultural chemical demand does not follow a fixed schedule. Planting windows compress weeks of input demand into days, and a biosecurity event at a poultry or swine operation can create urgent, high-volume sanitizer orders with almost no lead time. Brands that handle these spikes without supply disruptions have usually worked through production scaling and packaging logistics with their manufacturing partner before the season begins.
Packaging Formats in Agricultural Chemical Manufacturing
Packaging is where many brands underestimate the complexity. A formulation that ships efficiently in 275-gallon totes for large commercial operations may need to be repackaged in 5-gallon pails for distribution or 1-gallon jugs for direct-to-farm sales. Each format needs its own fill-line setup, label compliance, and closure specification.
Container
Typical Use
1-gallon jugs
Direct-to-farmer and retail sales
5-gallon pails
Route delivery and distributor stocking
55-gallon drums
Facility sanitation and equipment maintenance programs
275-gallon totes
Large commercial and cooperative accounts
Bulk tankers
Distribution hub replenishment
Dependable contract chemical packaging lets a brand move between small specialty runs and high-volume seasonal production without carrying excess finished-goods inventory. Direct shipping and staging through warehousing and shipping removes handling steps between production and the farm gate when application windows are tight.
The core advantages of flexible blending and packaging support include:
Logistical flexibility: Smooth transitions between small-batch runs and high-volume seasonal production.
Container diversity: Liquid and powder formulations packaged to match distributor and end-user preferences.
Supply chain integration: Warehouse staging and direct shipping that shorten the path from production to the customer.
Why Consistent Production Matters for Agricultural Chemical Brands
For agricultural chemical brands, formulation drift is an immediate liability. A batch of liquid fertilizer that is measurably off its stated nitrogen concentration does not simply underperform. It can injure crops, trigger warranty claims, and damage distributor relationships that took years to build. The same applies to equipment cleaners: a degreaser that is too strong strips protective coatings, and one that is too weak leaves contamination behind.
Consistency gets harder as production scales and raw material sources shift. Surfactant lots vary in their HLB characteristics, solvent batches carry trace impurities that affect viscosity, and active ingredient levels in incoming materials move within their specification ranges. If the blending process does not adjust for those variances in real time, the finished product drifts with them.
Climate adds another layer. A liquid concentrate that pours smoothly at 65°F may be too thick to pump at 40°F, or may separate after sitting in a 90°F warehouse. Locking in those performance limits during development and verifying them batch after batch is what separates a product that earns repeat orders from one that generates returns.
Proprietary formulas are real competitive assets, so brands also need a manufacturing partner that treats formula confidentiality as a firm operating standard, not a marketing claim.
Quality Control for Repeatable Agricultural Chemical Production
Batch-to-batch consistency depends on testing that goes well beyond a final pH check before shipment. A solid protocol typically includes:
Viscosity monitoring: Checks at multiple points in the blend catch surfactant or solvent variance before it becomes a finished-product defect.
Active ingredient verification: Titration, spectrophotometric analysis, or chromatography, depending on the chemistry, confirms the product delivers what the label claims.
Retention samples: Saved samples from every batch give a reference point for investigating field complaints and support traceability.
Documentation: Batch records that support distributor audits and compliance reviews.
The analytical equipment behind these protocols is a major capital investment that most agricultural brands do not need to own. A partner with in-house testing carries that burden and supplies the documentation trail. When quality verification is tied to filling and labeling, the consistency achieved in the blend carries through to the finished unit.
Navigating the Agricultural Supply Chain and Compliance
Agricultural chemical brands operate under several overlapping federal frameworks, and a gap in any one of them can delay a launch or put a registration at risk. Key obligations include:
Pesticide registration: Products making pest-control claims must be registered before commercial distribution, which requires formulation data, efficacy evidence, and safety assessments.
Waste and environmental safety: Chemical waste generated during manufacturing must be managed under hazardous waste rules, and water monitoring data informs reviews of how formulations behave in the environment.
Transport labeling and documentation: Shipping hazardous agricultural chemicals requires compliant labels, safety data sheets, and shipping papers.
Because transport rules apply the moment a product leaves the building, hazmat chemical packaging works best when it is built into the production workflow instead of handled at the shipping dock. A capable partner also absorbs safe storage, waste handling, and safety data sheet management, so brands can focus on sales and market development without surrendering control of the product.
How Toll Blending Gives Agricultural Brands a Practical Path to Market
Toll manufacturing is an arrangement in which a specialized manufacturer blends and packages raw materials into finished products according to the client’s own formula. The brand keeps ownership of the intellectual property and the customer relationship, while the manufacturer supplies the equipment, trained operators, and quality systems.
For crop nutrition, facility sanitation, and equipment care brands, this model removes the capital cost of tanks, filling lines, and laboratory equipment. A full-service toll chemical blending and packaging program handles everything from raw material receiving to finished, labeled product, and agricultural toll blending experience helps match formulations to the demands of seasonal distribution. The same approach scales across the full range of chemical blending services, from a first small order to a sustained production program.
Frequently Asked Questions About Agricultural Chemical Manufacturing
What is the definition of an agrochemical?
An agrochemical is any manufactured chemical compound used to improve agricultural productivity, protect crop health, or maintain farm facilities. The category includes primary crop nutrients (nitrogen, phosphate, potash), soil conditioners, pesticides (herbicides, insecticides, fungicides), and specialized facility sanitizers.
What is the difference between intensive farming and organic farming?
Intensive farming relies on targeted, high-volume inputs such as synthetic fertilizers and pesticides to maximize yields on a given acreage. Organic farming avoids synthetic chemical applications and relies on biological pest control, crop rotation, and organic soil amendments. Conventional production still accounts for most of the food supply, which is why consistent chemical manufacturing remains essential.
What are the primary pesticide application safety guidelines?
Core safety practices include wearing proper personal protective equipment, following label dilution ratios exactly, preventing drift during application, and disposing of waste through compliant hazardous waste channels. Transport of these products is governed by separate hazardous materials rules.
How does custom chemical blending benefit agricultural brands?
Custom blending lets brands adjust standard formulations to specific soil profiles, crop needs, or climate conditions. It ensures liquid and powder concentrates dilute properly and rinse clean without clogging equipment, while protecting the brand’s proprietary formula.
What is agricultural chemical toll manufacturing?
Toll manufacturing, also called toll blending, is an arrangement where a specialized manufacturer processes, blends, and packages raw materials into finished products using a client’s proprietary formula. Agricultural brands gain access to production equipment, quality control systems, and compliance expertise without the expense of building their own facility.
What container sizes are available for agricultural chemical products?
Liquid and powder products can be packaged in sizes ranging from 1-gallon jugs and 5-gallon pails to 55-gallon drums, 275-gallon totes, and bulk tankers, depending on how the product is distributed and used.
Contact Us Today
Agricultural chemical manufacturing is a technically demanding, heavily regulated discipline that extends well beyond field sprays and fertilizer bags. The brands that build lasting positions, whether in crop nutrition, facility sanitation, or equipment maintenance, treat formulation consistency, compliant packaging, and supply chain agility as core strengths. Seasonal demand does not wait for a manufacturing partner to get organized, and formulation shortcuts do not hold up under scrutiny.
Industrial Technology Corporation is a family-owned blending and packaging partner with more than 40 years of experience. If you are ready to scale an agricultural product line, share your formulation, packaging, and toll blending needs with our team.